-
E-mail
spm@beierpm.com
-
Phone
13773268866
-
Address
Intersection of Gangcheng Avenue and North Second Ring Road, Zhangjiagang Economic Development Zone, Jiangsu Province
Product Categories
Jiangsu Bell Machinery Co., Ltd
Screw plastic extrusion production equipment
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
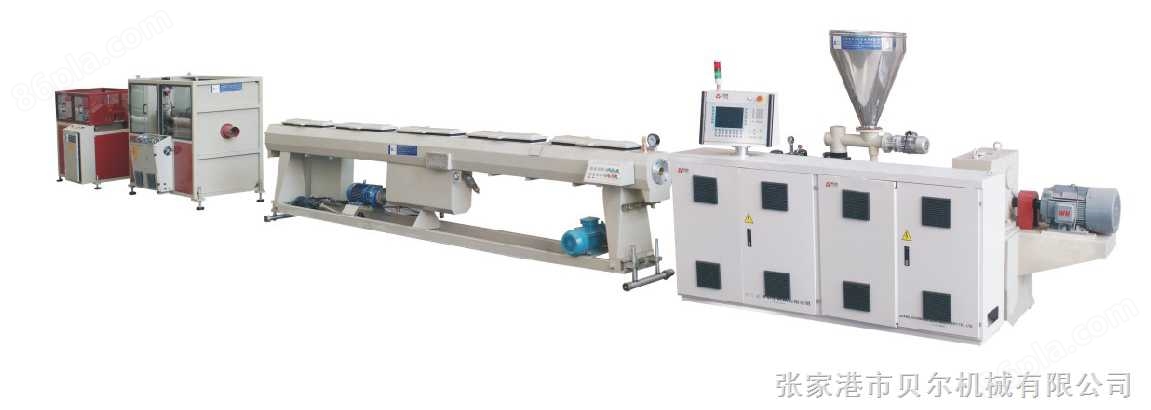
The screw plastic extrusion production equipment has stable performance and can effectively plasticize and extrude the melt at lower temperatures. The barrel is equipped with a cast aluminum heater, which has high thermal efficiency, fast and uniform heating, and is equipped with a cooling fan.
Product Details
Screw plastic extrusion production equipmentstructure
deceleration system
The reduction system adopts a plastic mechanical gearbox, and the transmission components are made of ultra-high alloy carburizing steel, combined with carburizing, quenching, and gear grinding processes. The key components have been strengthened with surface treatment, with a tooth surface strength of HRC54-62, a core hardness of HRC30-40, and gears of 6 levels. This system has the characteristics of high speed, high torque, and low noise.
feeding systemAdopting a quantitative feeding system with a twin-screw mixer, the feeding is uniform, accurate, and does not produce any shelving phenomenon.
electric control systemImported electrical components are used, the control panel is a human-machine interface, and various parts of the equipment are controlled in a "modular" manner (which can also be configured according to user requirements). The multifunctional module structure is clear, with safety interlock devices (such as lubrication pressure loss protection, machine head pressure protection, overcurrent protection, etc.), which truly reflect the operation status of the equipment, with accurate control, high sensitivity, and easy operation. Heating system: Adopting cast aluminum, cast copper, and ceramic resistance heating devices, the heating is uniform, the temperature rises quickly, and the temperature control accuracy is high.
Temperature control system:Adopting a dual channel temperature control meter, it has sensitive response, convenient temperature setting and adjustment, and high temperature control accuracy.
cooling systemAdopting two forms of cooling: water cooling, oil cooling, and air cooling, the cooling is rapid, uniform, and effective.
Vacuum system:Built in vacuum system, with a vacuum degree of up to 0.09Mpa., ensuring full plasticization of materials and improving product quality.
Auxiliary machinery:According to different process requirements of users, various cutting forms such as cold drawn strip cutting, drag chain traction cutting, air-cooled die surface hot cutting, water ring hot cutting, etc. can be selected.
Screw plastic extrusion production equipmentMaintenance and upkeep:
(1) Daily maintenance is a regular routine work that does not take up the operating hours of the equipment and is usually completed during the driving period. The key is to clean the machine, lubricate all moving parts, tighten loose threaded parts, timely inspect and adjust the motor, control instruments, various working components and pipelines, etc.
(2) Regular maintenance is generally carried out after the extruder has been running continuously for 2500-5000 hours before stopping. The machine needs to extract the screw to inspect, measure, and identify the wear of the main components, replace parts that have reached the specified wear limit, and repair damaged parts.
(3) The extruder is not allowed to run empty to avoid damaging the screw and machine shaft.
(4) If there is any abnormal noise during the operation of the extruder, it should be stopped immediately for inspection or repair.
(5) Strictly prevent metal or other debris from falling into the hopper to avoid damaging the screw and barrel. To prevent iron impurities from entering the barrel, a magnetic frame can be installed at the material inlet of the barrel; Or screen the materials beforehand.
(6) When the extruder needs to be stopped for a long time, the screw should be placed in the machine shaft and not removed. The working surface such as the head should be coated with anti rust lubricating grease.
(7) Regularly calibrate temperature control instruments, check their correctness of adjustment and sensitivity of control.
Similar Product Recommend