-
E-mail
spm@beierpm.com
-
Phone
13773268866
-
Address
Intersection of Gangcheng Avenue and North Second Ring Road, Zhangjiagang Economic Development Zone, Jiangsu Province
Product Categories
Jiangsu Bell Machinery Co., Ltd
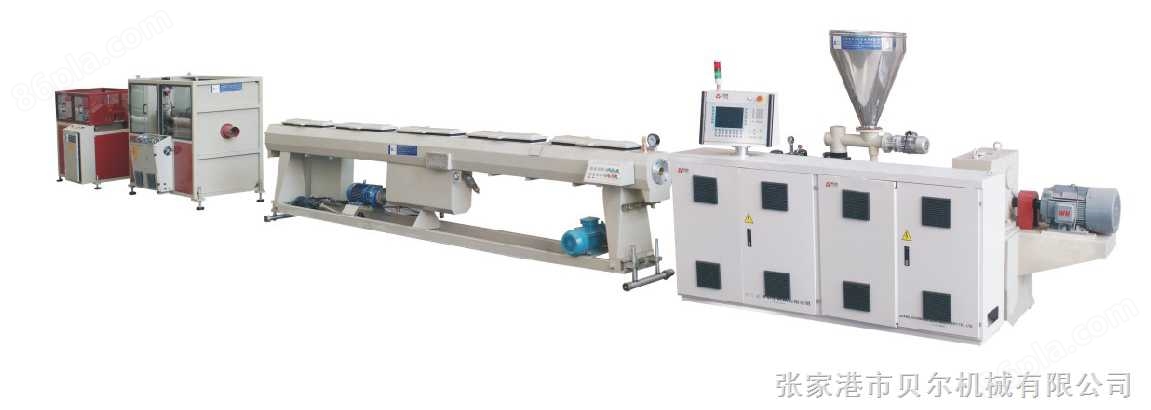
Plastic pipe extrusion production equipment
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The conical pipe extrusion production equipment is mainly used for producing various diameter and wall thickness plastic PVC pipes for agricultural water supply and drainage, building water supply and drainage, cable laying, and other aspects
Product Details
Plastic pipe extrusion production equipmentIntroduction:
Mainly used for the production of various diameter and wall thickness plastic PVC pipes for agricultural water supply and drainage, building water supply and drainage, cable laying, etc., it consists of a conical twin-screw extruder, a vacuum forming table, a traction machine, a cutting machine, a flipping rack, etc. The screw extruder and traction machine adopt AC variable frequency speed regulation device, and the vacuum pump and traction motor are all high-quality products. There are traction methods such as two claw, three claw, four claw, and six claw. Saw blades or planetary cutting can be used, and length and thickening devices can also be equipped. The unit has reliable performance and high production efficiency. Our company can configure equipment to produce spiral silencing tubes and core foam tube units according to customer requirements.
Plastic pipe extrusion production equipmentPrecautions for operation:
(1) Preparation before startup
① Correctly handle the position and connection of the air holes on the splitter bracket and mold body during the installation of the machine head; The mouth mold and core mold should be concentric: the sealing end face should be tightly pressed to prevent material leakage; Place a splitter plate between the discharge end of the extruder and the head of the machine; The connection between the head flange and the extruder flange should be evenly tightened. If it is a bolted connection, it should be tightened again after the machine is preheated.
② The heating ring outside the machine head should be tightly wrapped around the machine head during installation, and there should be no empty space between the heating ring and the outer wall of the machine head. Then, the thermocouple should be installed and the power should be turned on.
③ After installing the device in a fixed position, connect the cooling water inlet and outlet pipes and vacuum pipeline (if using vacuum shaping technology).
④ Set the temperature for each section of the extruder and preheating the head; After heating up to the set temperature, maintain it for a certain period of time to bring the temperature inside and outside the machine and the machine head to the same level.
⑤ The inspection and adjustment of each machine in the pipeline production line should ensure that the center position of each device is aligned and the start-up and operation are normal: the water and gas pipelines are unobstructed.
(2) Power on
① Maintain a fixed material level in the hopper; When driving, the screw should run slowly first, and after the guide pipe reaches a smooth state, the screw speed should be increased.
② When the material is extruded from the machine head, the plasticization state of the material and the uniformity of the pipe blank wall thickness should be observed first, and the heating temperature should be adjusted according to the plasticization situation; Adjust the adjusting bolts according to the bending condition of the extruded pipe blank to achieve the requirement of uniform pipe wall.
(3) Shutdown
① Shutdown operation, stop feeding or unloading the stored materials in the hopper; Squeeze out the materials in the machine as much as possible.
② Stop heating; Reduce the screw speed first, gradually reduce it to zero, and then stop the machine.
③ Turn off water, electricity, cooling water inlet valve, compressed air machine or vacuum pump, traction machine, etc.
④ Disassemble the machine head: Disassemble the machine head and clean it thoroughly; Attention should be paid to using tools that do not scratch the surface of the machine head: if not in use temporarily, the machine head should be coated with grease for protection.
Similar Product Recommend