-
E-mail
webmaster@rxjd.com
-
Phone
13801568566
-
Address
China
Product Categories
Zhangjiagang Rixin Electromechanical Co., Ltd
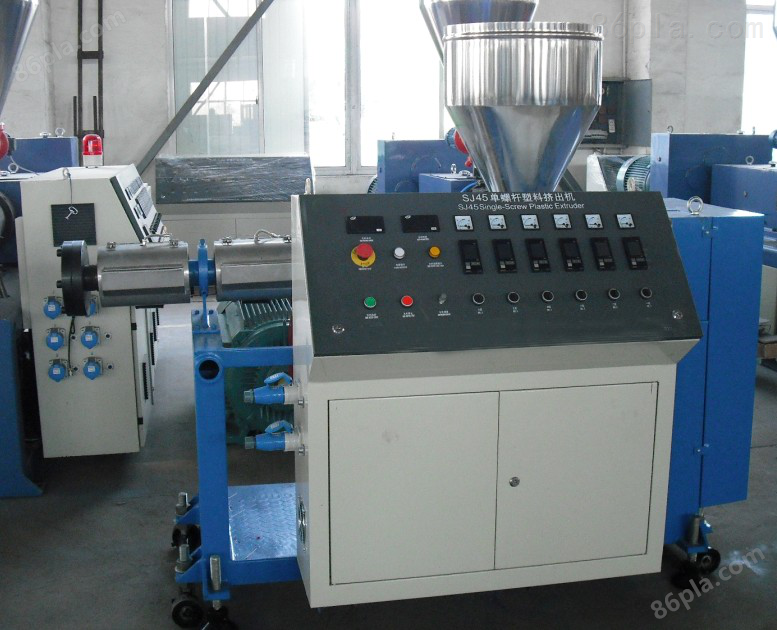
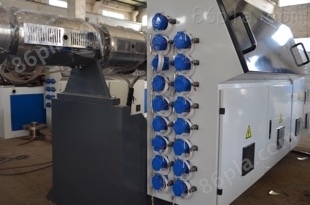
Multi functional PVC extrusion production equipment
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The reliable two-stage screw core external circulation temperature control system of the multifunctional PVC extrusion production equipment ensures that different formulations can produce high-quality UPVC pipes
Product Details
Introduction to Multi functional PVC Extrusion Production Equipment:
Complete all the above processes through a barrel with a screw and a spiral channel. Plastic pellets enter the barrel through a hopper at one end and are then transported to the other end of the barrel through a screw. In order to have sufficient pressure, the depth of the threads on the screw decreases as the distance to the hopper increases. External heating and internal heat generated by friction between plastic and screws soften and melt the plastic. Different polymers and applications often have different design requirements for plastic extruders. Many options involve discharge ports, multiple feeding ports, special mixing devices along the screw, cooling and heating of the melt, or no external heat source (adiabatic plastic extruder), relative size changes in the gap between the screw and the barrel, and the number of screws, etc
Multi functional PVC extrusion production equipmentoperation
Complete all the above processes through a barrel with a screw and a spiral channel. Plastic pellets enter the barrel through a hopper at one end and are then transported to the other end of the barrel through a screw. In order to have sufficient pressure, the depth of the threads on the screw decreases as the distance to the hopper increases. External heating and internal heat generated by friction between plastic and screws soften and melt the plastic. Different polymers and applications often have different design requirements for plastic extruders. Many options involve discharge ports, multiple feeding ports, special mixing devices along the screw, cooling and heating of the melt, or no external heat source (adiabatic plastic extruder), relative size changes in the gap between the screw and the barrel, and the number of screws, etc
Multi functional PVC extrusion production equipmentoperation
1、 Drive
1. After the constant temperature is maintained, the machine can be driven. Before driving, the flange bolts of the machine head and extruder should be tightened again to eliminate the difference in thermal expansion between the bolts and the machine head. The sequence of tightening the machine head bolts is diagonal tightening, and the force should be uniform. When tightening the flange nut of the machine head, it is required that the tightness around is consistent, otherwise the material will run off.
2. Drive, select the "Ready to Drive" button, then connect the "Drive" button, and slowly rotate the screw speed adjustment knob to start the screw speed slowly. Then gradually increase the speed while adding a small amount of material. Pay close attention to the changes in the readings of the host ammeter and various indicator heads when adding materials. The torque of the screw should not exceed the red mark (usually 65% -75% of the torque gauge). Before the plastic profile is extruded, no one is allowed to stand directly in front of the die to prevent injury accidents caused by bolt breakage or soaking due to wet raw materials. After the plastic is extruded from the die of the machine head, the extruded material needs to be slowly cooled and led onto the traction device and shaping die, and these devices need to be activated. Then, based on the indication values of the control instrument and the requirements for the extruded product. Adjust each part accordingly to ensure that the entire extrusion operation reaches a normal state. And according to the needs, sufficient material is added, and the twin-screw extruder adopts a metering feeder to uniformly and uniformly feed at a constant speed.
3. When the discharge of the mouth mold is uniform and the plastic is good, it can be pulled into the shaping sleeve. The degree of plasticization needs to be judged based on experience, usually based on the appearance of the extruded material, that is, the surface has luster, no impurities, no foaming, coking, and discoloration. If the extruded material is squeezed to a certain degree by hand without burrs or cracks, and has a certain degree of elasticity, it indicates that the material is well plasticized. If the plasticization is poor, the screw speed, barrel, and head temperature can be adjusted appropriately until the requirements are met.
During the extrusion production process of PVC drainage pipe extruder, various process parameters should be checked regularly according to the process requirements to ensure that they are normal, and a process record form should be filled out. Inspect the quality of profile products according to quality inspection standards, and take timely measures to solve any problems found.
2、 Parking
1. Stop feeding, squeeze the plastic out of the extruder, and when the screw is exposed, turn off the power supply of the barrel and head, and stop heating.
2. Turn off the power supply of the extruder and auxiliary equipment to stop the operation of the screw and auxiliary equipment.
3. Open the connecting flange of the machine head and disassemble the machine head. Clean the various components of the porous plate and machine head. To prevent damage to the inner surface of the machine head during cleaning, residual materials inside the machine head should be cleaned with steel plates and steel sheets. Then, the plastic adhered to the machine head should be sanded off and polished, and coated with engine oil or silicone oil for rust prevention.
4. Clean the screw and barrel, remove the machine head, restart the main engine, add parking material (or crushed material), clean the screw and barrel, and choose low speed (around SR/min) for the screw to reduce wear. After the parking material is crushed into powder and extruded, compressed air can be used to repeatedly blow out residual granules and powders from the feeding port and exhaust port until there is no residual material in the barrel. Then, reduce the screw speed to zero, stop the extruder, and turn off the main power and cold water main valve.
5. Safety precautions to be taken during extrusion include electrical, thermal, and mechanical rotation, as well as handling of bulky components. The PVC drainage pipe extrusion locomotive room must be equipped with lifting equipment to install and remove bulky components such as machine heads and screws to ensure safe production.