-
E-mail
248693695@qq.com
-
Phone
15268032526
-
Address
Lingang Industrial Park, Shuangqiao Town, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhoushan Jingke Machinery Manufacturing Co., Ltd
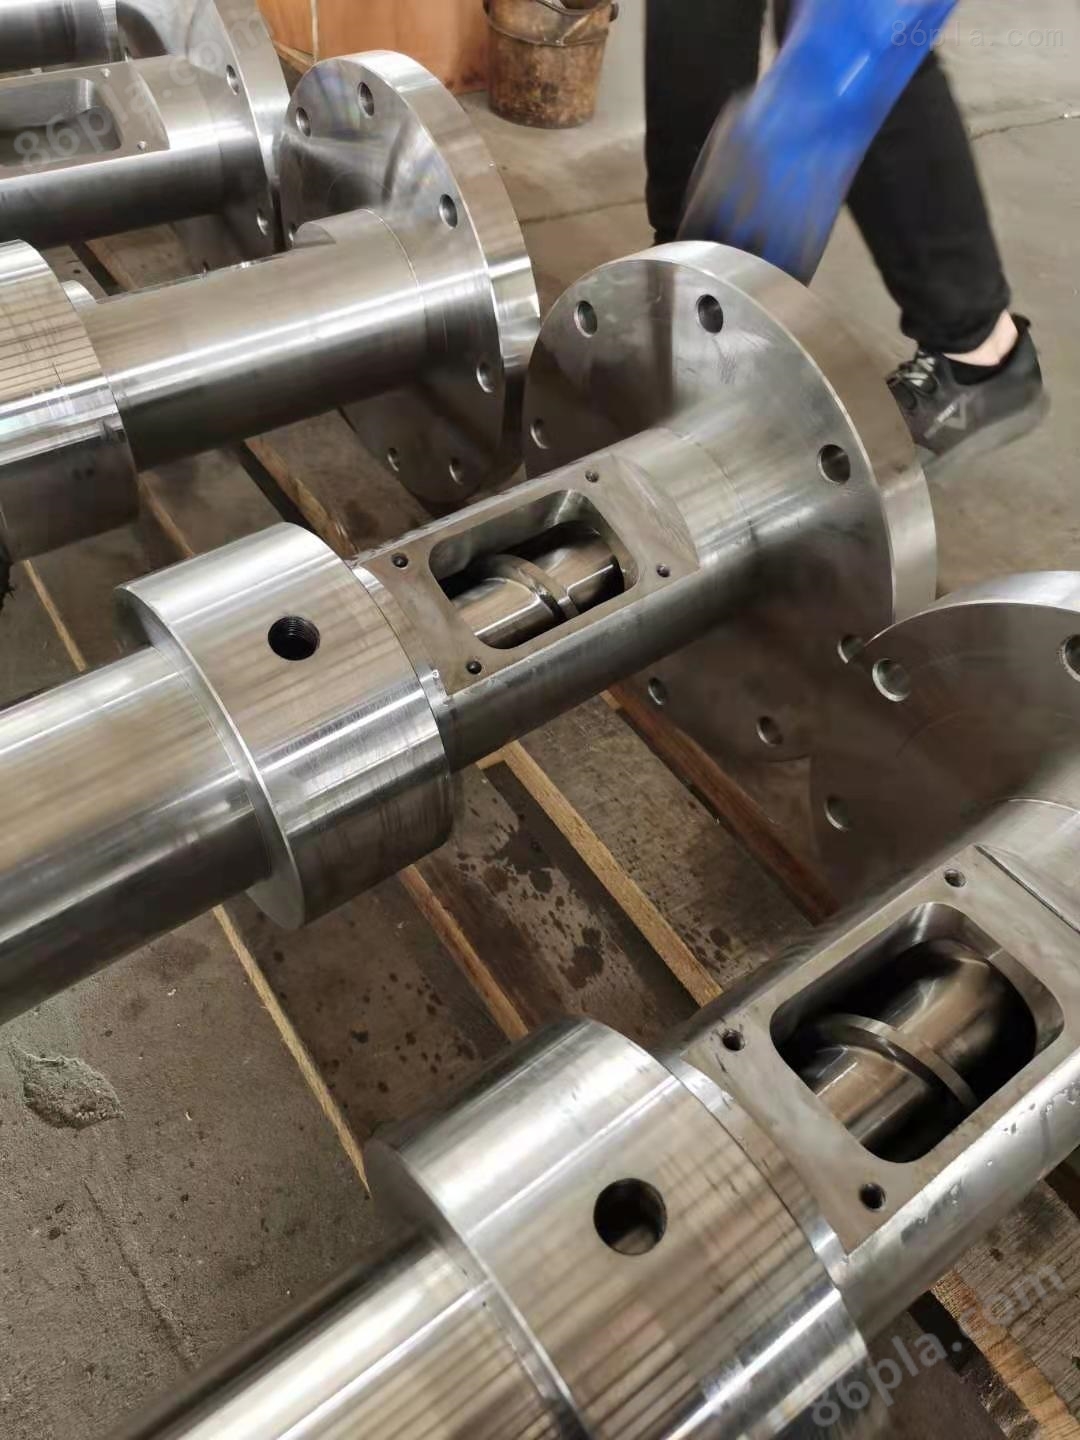
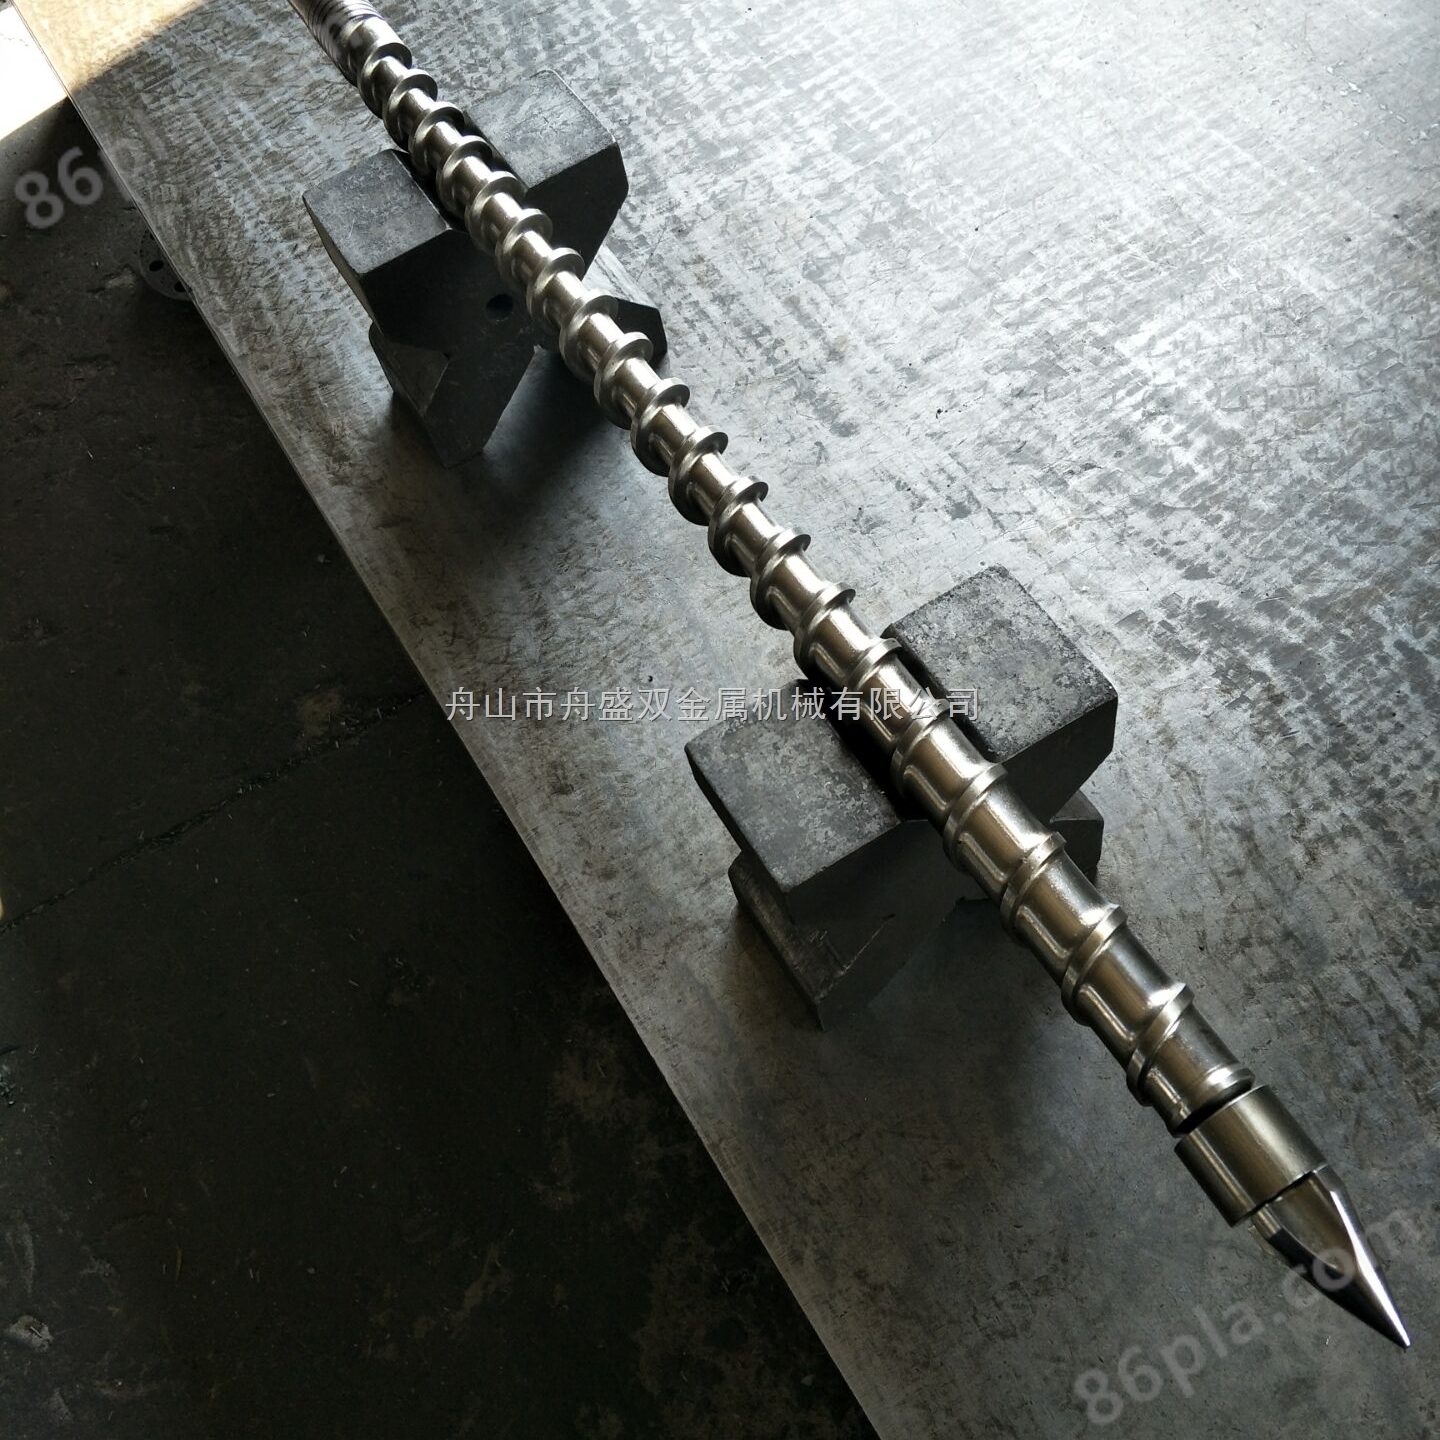
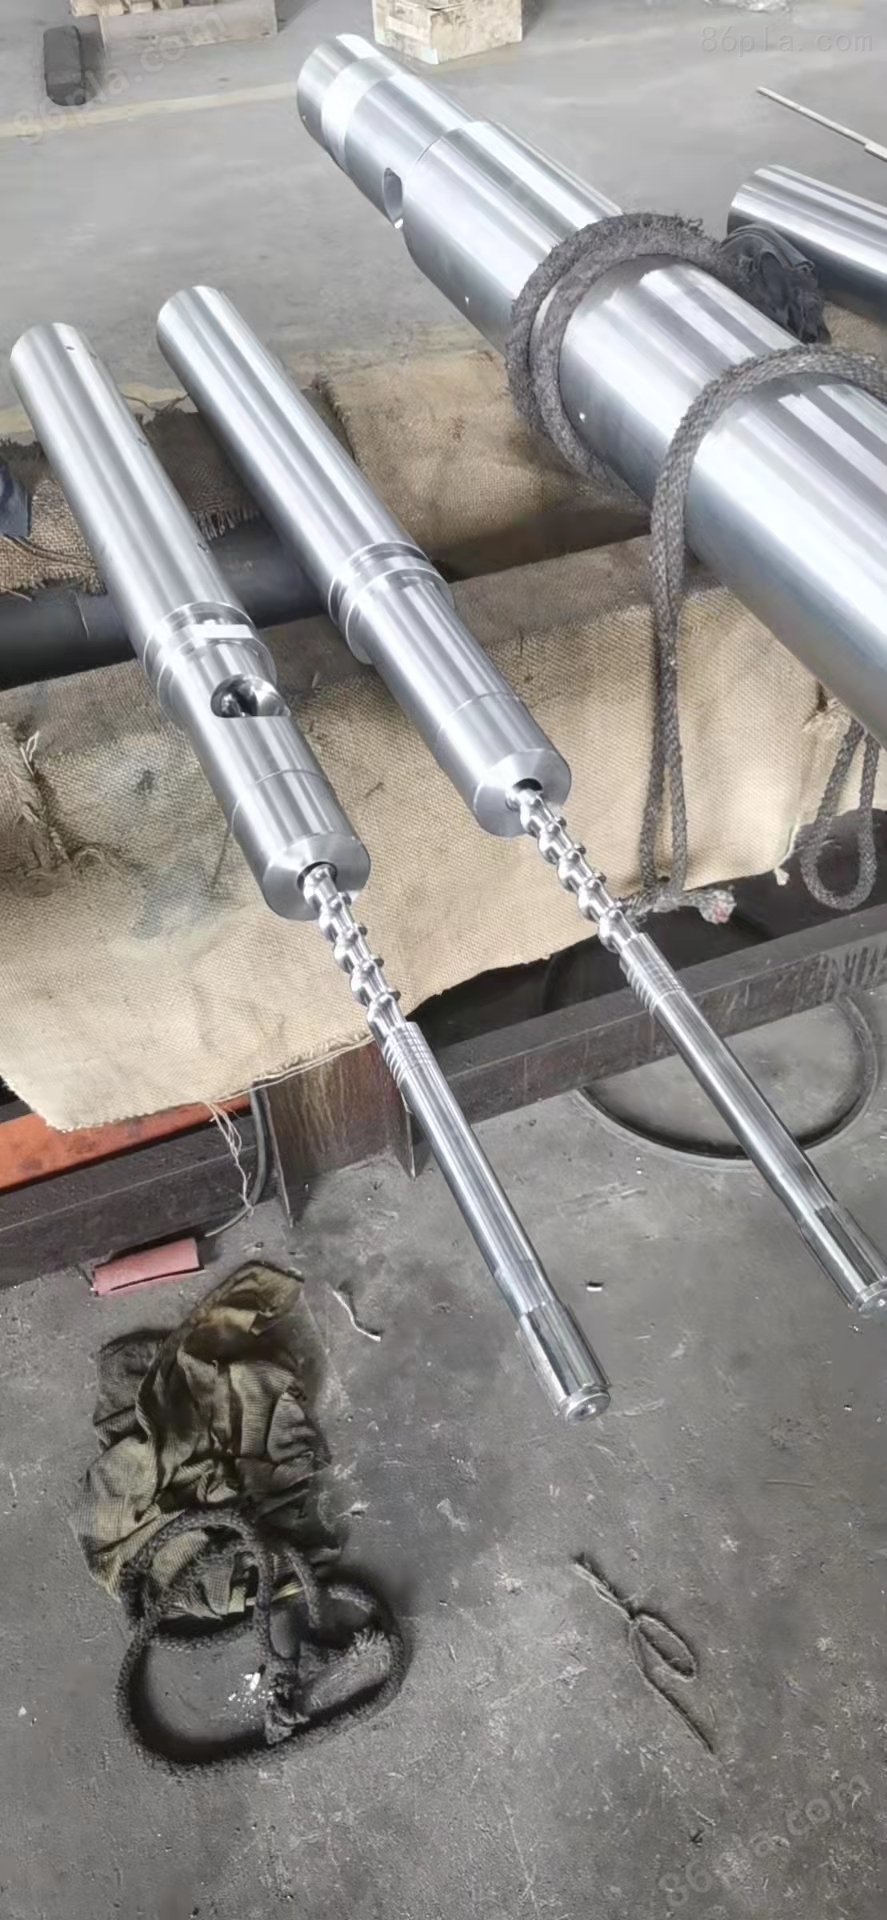
Wear resistant multi-layer screw
NegotiableUpdate on 01/27
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
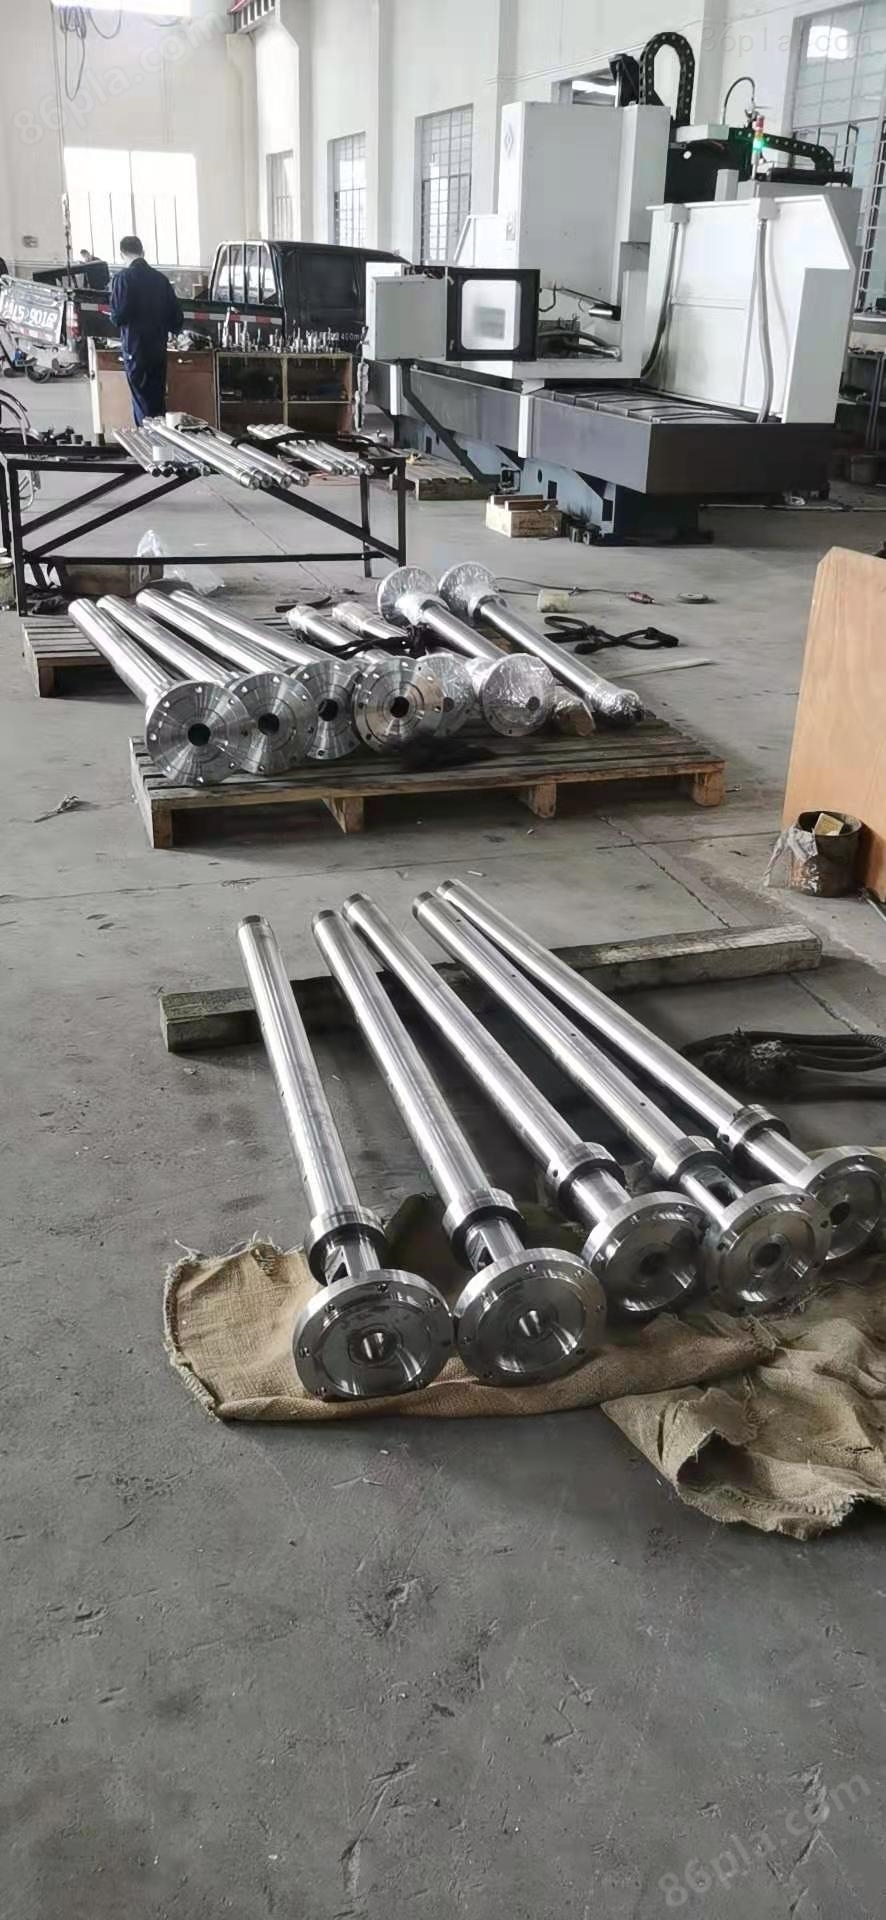
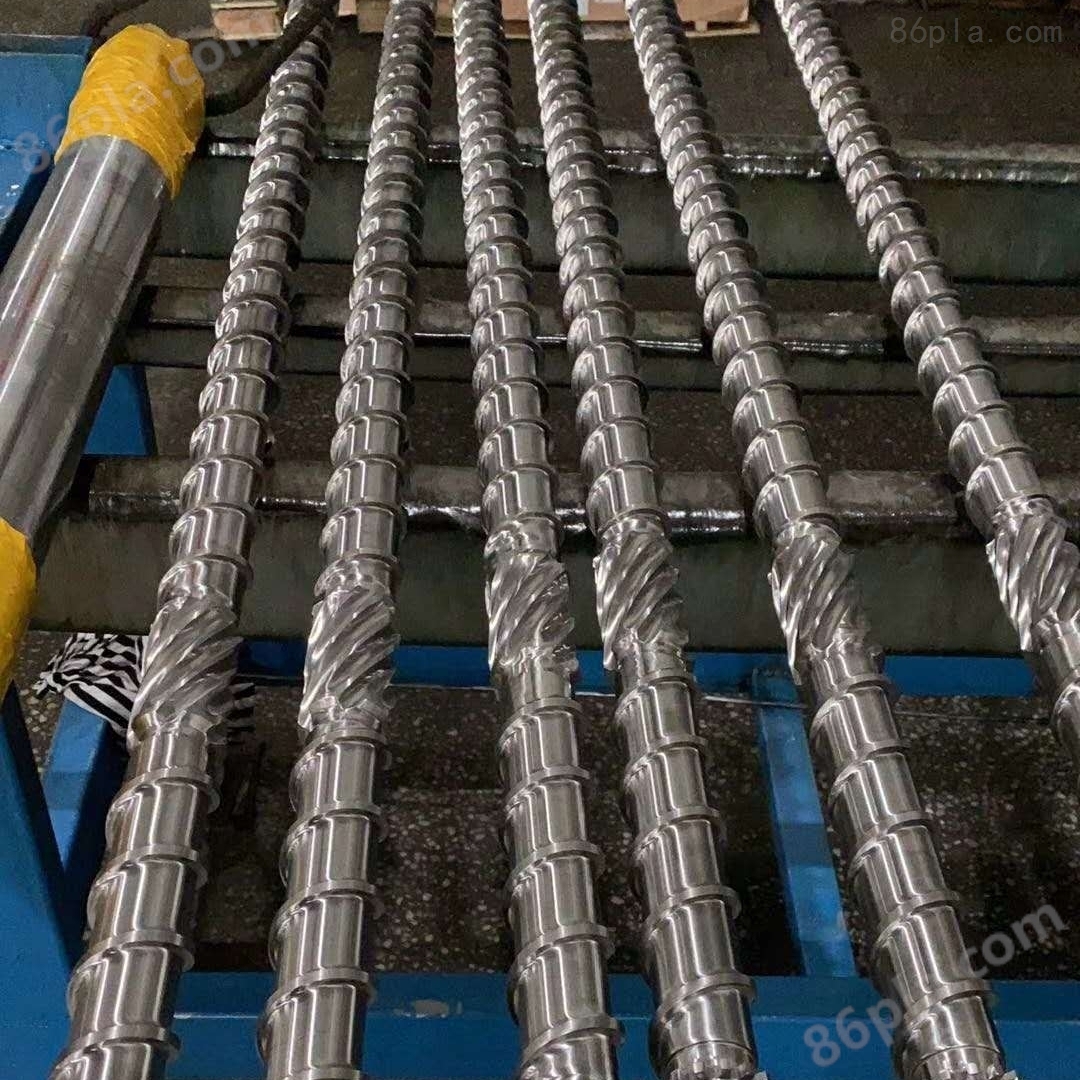
Wear resistant multi-layer screws have the characteristics of high strength, corrosion resistance, high temperature resistance, and wear resistance. They can be used for more than half of the time of ordinary barrel screws, reducing the operating and labor costs of many injection molding machine factories.
Product Details
Wear resistant multi-layer screwFeatures:
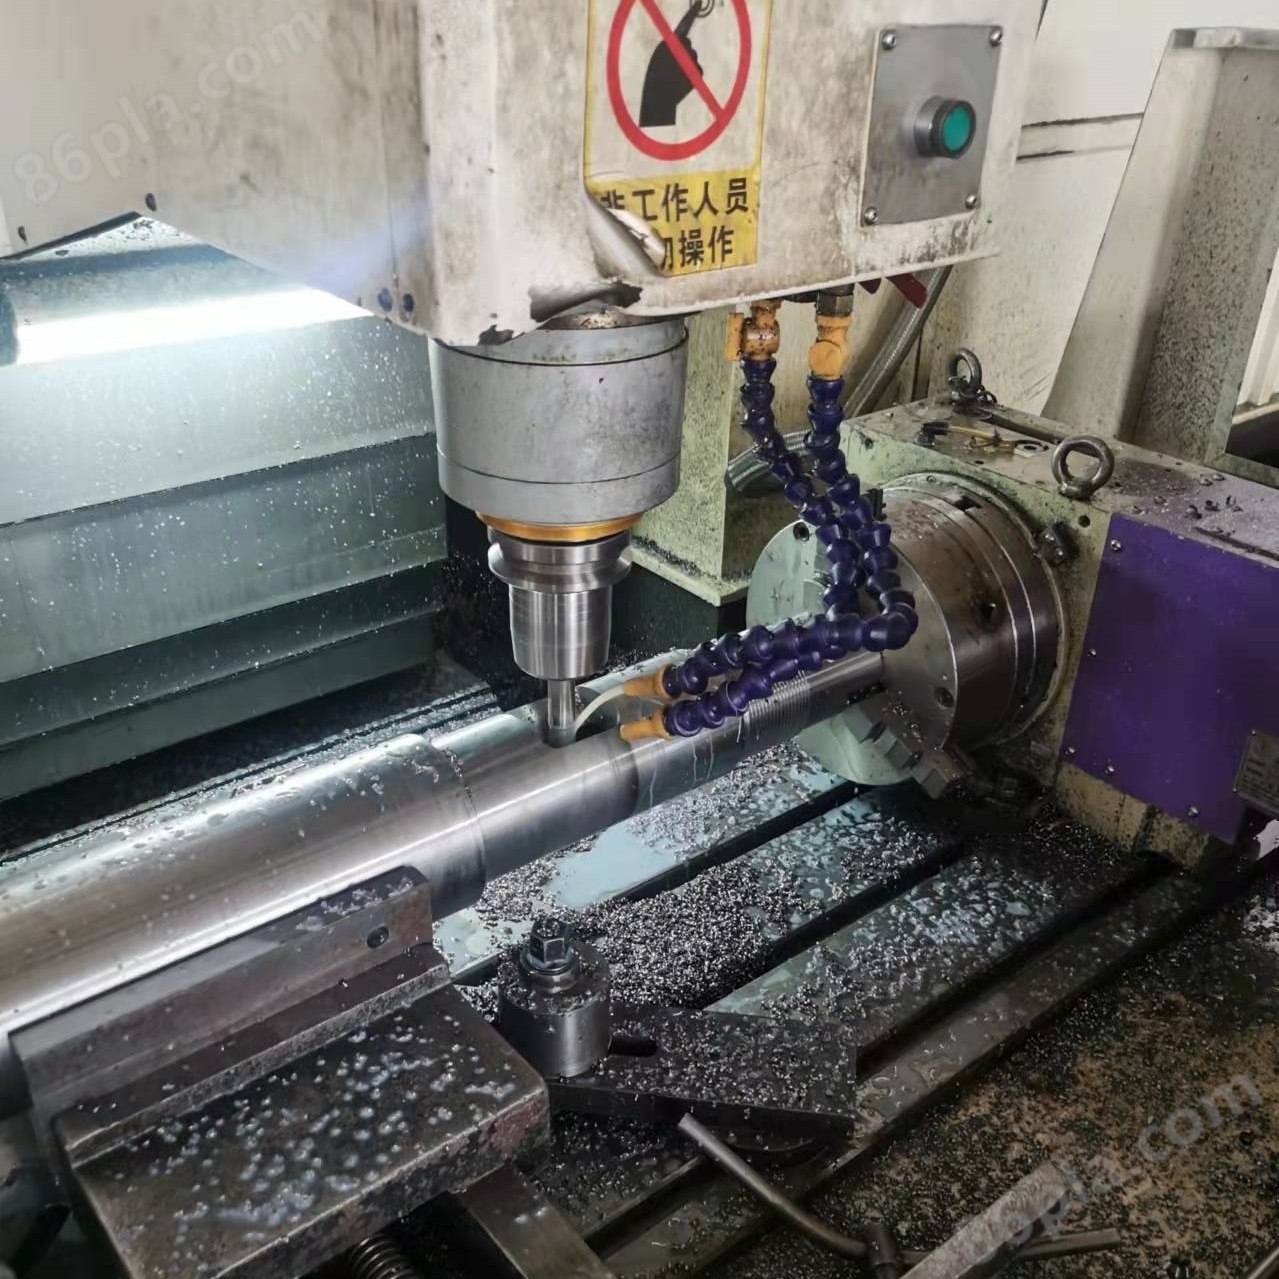
It has comprehensive properties such as high wear resistance, high hardness, and high temperature resistance, and its service life is generally more than 10 times that of general alloy steel. We use ultra-fine particle hard alloy materials, combined with our company's efficient processing equipment and advanced processing technology, to produce products with good cross-sectional crack resistance strength. At the same time, we can produce a large amount of cutting heat and rubber melt coating under harsh working conditions without being affected by corrosion, bringing excellent production efficiency to your machine
Precautions for use:
1) When starting the injection molding machine, the injection molding should be fully preheated. After the material barrel reaches the preset temperature, continue to keep the insulation for 15 minutes for those with a diameter of less than 60mm. After the above 30 minutes, restart the motor to start the screw related actions.
2) The material and screw should be matched. Especially for corrosive and hard materials such as PVC, flame retardant materials, and glass fiber additives, professional screws should be used instead of ordinary screws.
3) When using anti salivation, it is important to ensure that the plastic inside the barrel is melted to prevent damage to the transmission system components when the screw retracts.
4) Avoid phenomena such as screw idling and slipping.
5) Avoid mixing POM and PVC into the material barrel at the same time, as it may react and cause serious industrial accidents at the melting temperature.
Wear resistant multi-layer screwPrecautions for cleaning:
① Prepare ventilation conditions as smoke may be generated during the processing.
② Rotate the screw at a constant speed and heat the surface evenly. Do not only heat the screw at a certain point, otherwise the thermal stress on one side will cause the screw to twist and deform.
③ The temperature of the screw should not exceed 400 ℃ (including the thread), otherwise it will reduce the hardness and wear resistance of the screw.
④ Special care should be taken when handling the check ring, as the thin-walled part on the check ring heats up rapidly.
⑤ Clean with a wire brushscrewPolish the surface of the screw with sandpaper (sand grade 240-280).
⑥ Burn off the residual material on the internal thread (left-hand thread) with a flame, and then clean the thread with a wire brush.
⑦ When screwing on the screw head, apply HSC ointment. Do not use other types of lubricating oil or grease to lubricate the screw threads. These lubricants may undergo coking reactions at high temperatures, and the residue left behind may get stuck in the screw head.
⑧ Avoid letting hard objects hit the screw, causing cracks or fractures in the screw.
⑨ When repairing, especially when repairing heated onesscrewWhen using the barrel, it is necessary to wear a protective face mask and glasses.