-
E-mail
248693695@qq.com
-
Phone
15268032526
-
Address
Lingang Industrial Park, Shuangqiao Town, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhoushan Jingke Machinery Manufacturing Co., Ltd
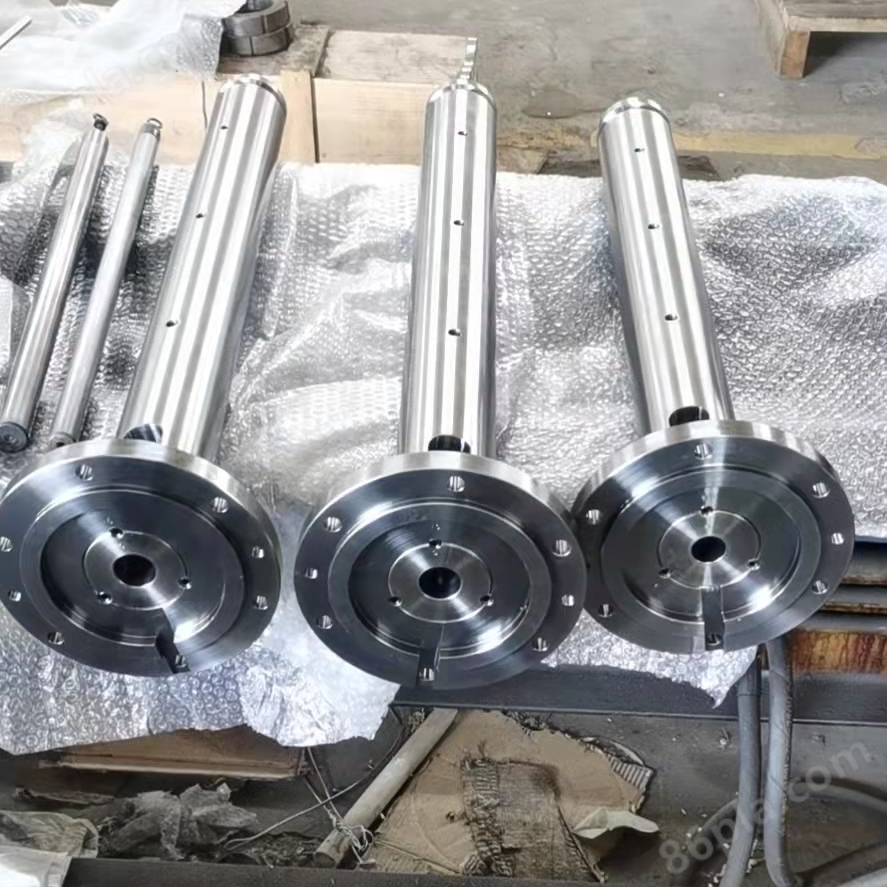
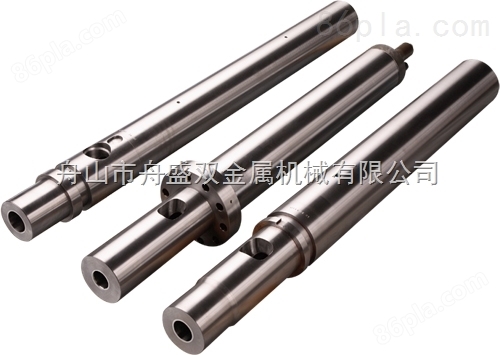
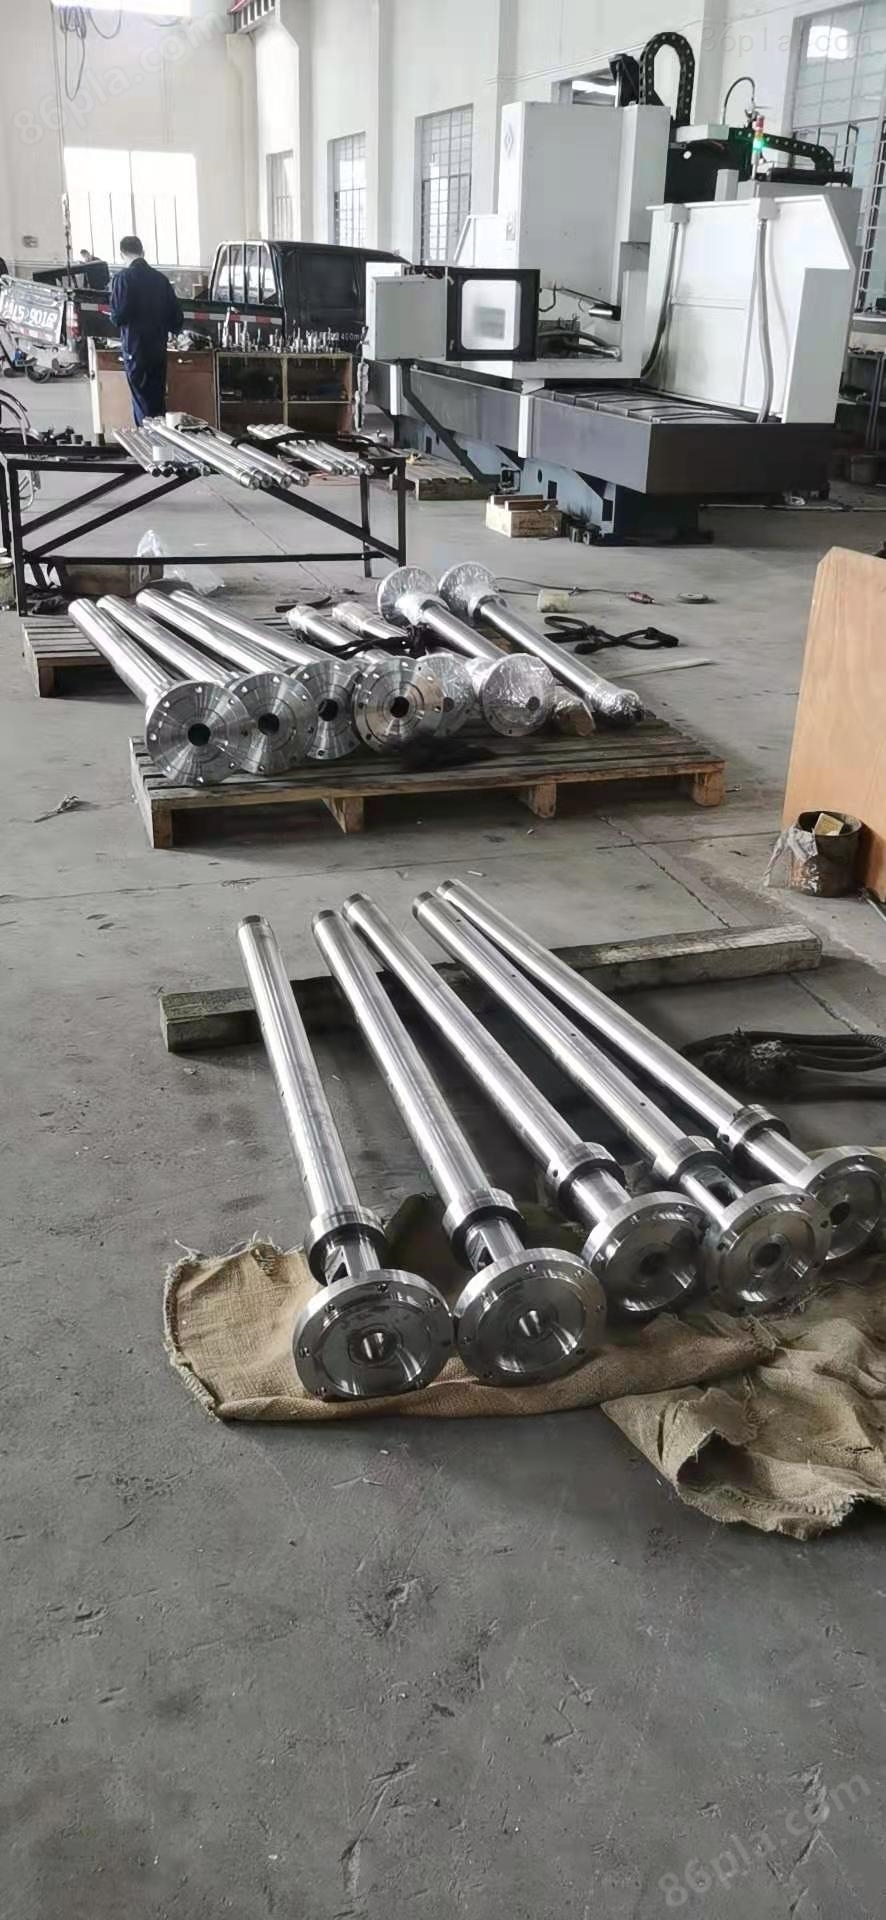
Multi layer alloy metal screw
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
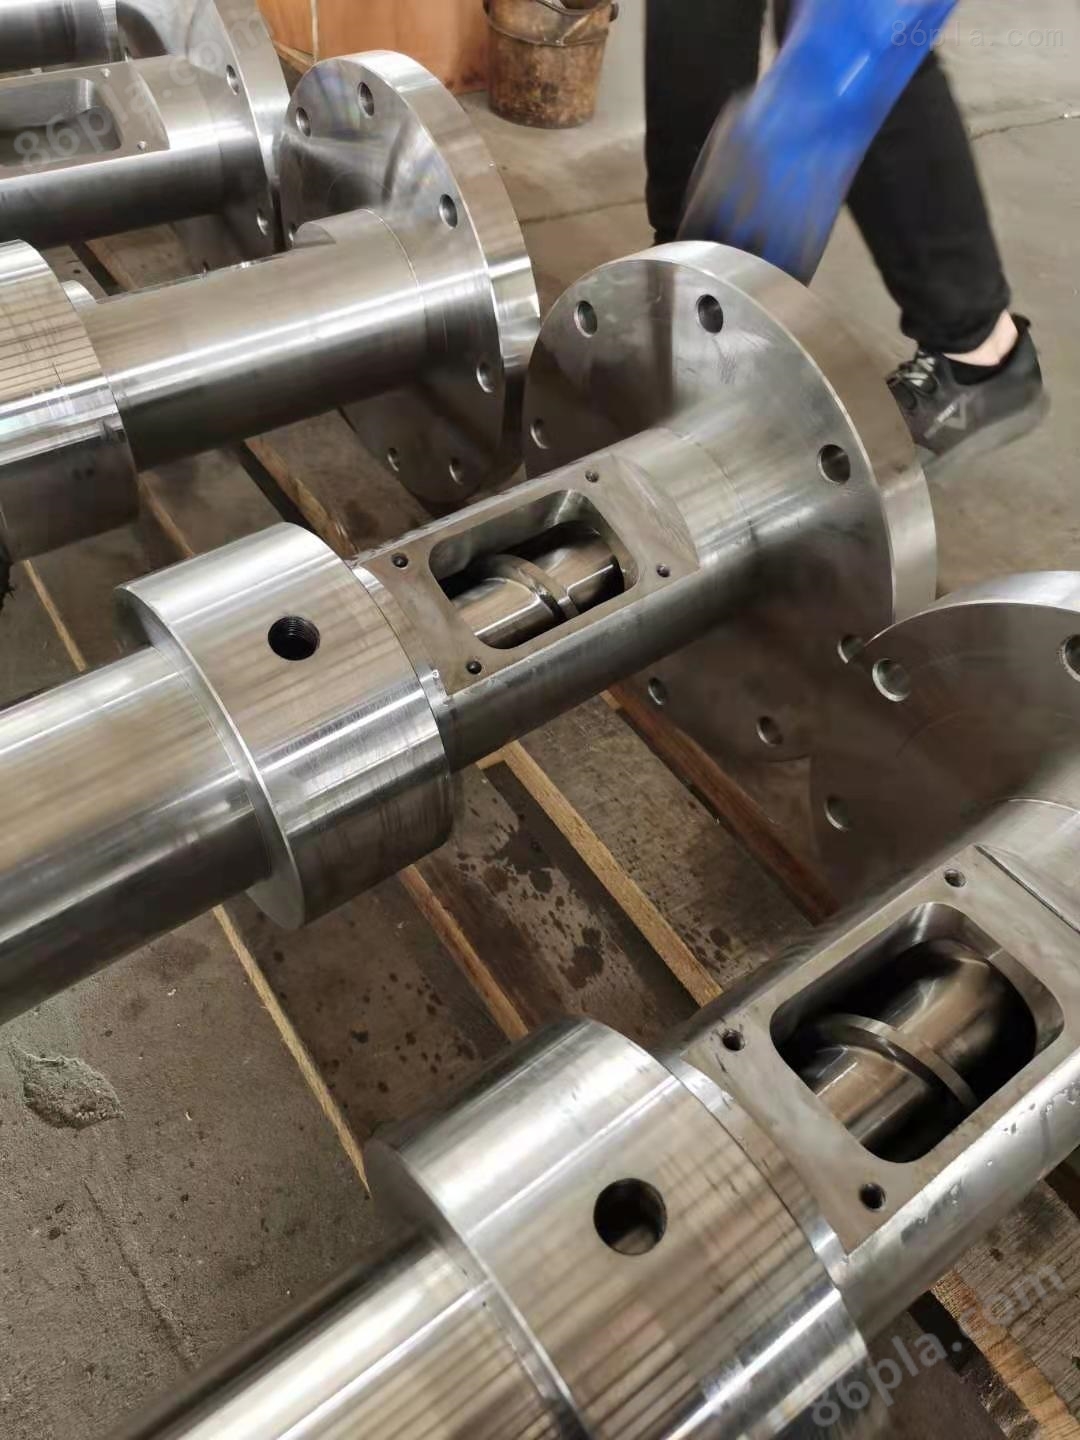
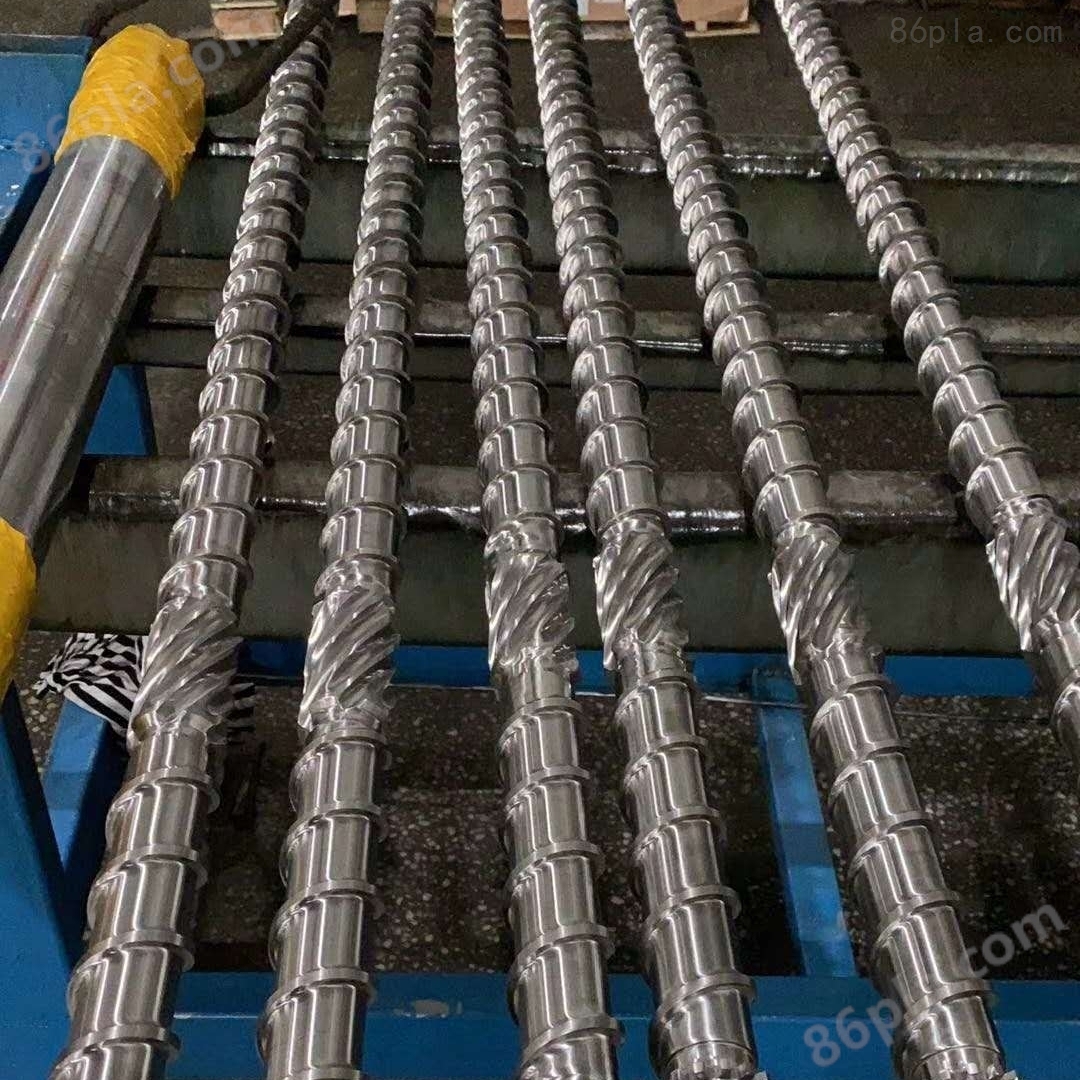
Multi layer alloy metal screws have the characteristics of high strength, corrosion resistance, high temperature resistance, and wear resistance. They can be used for more than half of the time of ordinary barrel screws, reducing the operating and labor costs of many injection molding machine factories.
Product Details
Characteristics of multi-layer alloy metal screw:
1. Wear resistant and have a long lifespan;
2. High temperature resistance, no deformation at high temperatures;
3. Corrosion resistance, materials have corrosiveness;
4. Good cutting performance;
5. High strength, capable of withstanding large torque and high speed;
6. After heat treatment, the residual stress is small and the thermal deformation is small.
Precautions:
1. When the injection molding machine is started, it should be fully preheated. After the barrel reaches the predetermined temperature, maintain a temperature below 60 millimeters for another 15 minutes. After more than 30 minutes, start the motor and perform operations related to the screws.
2. Match the material with the screw. Especially for corrosive materials and hard materials such as PVC, flame retardant materials, glass fiber materials, etc., avoid using ordinary materials.
3. If ordinary machines use corrosive materials, attention should be paid to using stable materials such as high-density polyethylene, high impact polystyrene, etc. for cleaning and replacement.
4. If ordinary machines occasionally use fiberglass materials, attention must be paid to high material temperature, low speed, and low back pressure. Remember.
5. Regardless of the material, try not to use low-temperature extreme production. For example, PC material can also be produced at 250 degrees, while ABS can hardly be produced at 185 degrees. However, it is not good for screws because it requires a large torque and severe wear. Meanwhile, if a lower limit issue must be used, a low speed should be employed.
6. After stopping for more than half an hour each time, the discharge port should be closed, the materials in the bucket should be cleaned, and an insulation layer should be set up.
7. Prevent foreign objects from falling into the cylinder and damaging the screw and cylinder. To prevent metal fragments and debris from falling into the funnel, a magnetic funnel should be added if the recycled material is being processed to prevent iron filings from entering the funnel.
8. When using anti saliva, make sure the plastic inside the bucket melts to prevent damage to the transmission system components when the screws retract.
9. Avoid idling and slipping.
10. When using new plastic, the rest of the bucket should be cleaned. When using materials such as polyoxymethylene, polyvinyl chloride, PA+GF, etc., the degradation of raw materials should be minimized as much as possible, and nozzle materials such as ABS should be washed away in a timely manner after shutdown.
Multi layer alloy metal screwMaintenance:
1. Avoid phenomena such as screw idling and slipping;
2. Avoid mixing POM and PVC into the material barrel at the same time, as they may react and cause serious industrial accidents at the melting temperature;
3. Avoid foreign objects falling into the material barrel and damaging the screw and barrel. To prevent metal fragments and debris from falling into the hopper, if processing recycled materials, a magnetic hopper needs to be added to prevent iron filings and other debris from entering the material barrel;
Do not start the machine until the material barrel has reached the preset temperature. Newly opened electric heaters generally require the temperature to reach the set value for 30 minutes before operating the screw;
5. When using anti salivation, it is necessary to ensure that the plastic inside the barrel is melted to prevent damage to the transmission system components when the screw retracts;
When the temperature of the molten plastic is normal but black spots or discoloration are constantly observed, the rubber screw check ring seat (over rubber ring, meson) should be checked for damage;
7. If the machine stops for more than half an hour each time, close the feeding port and clean the remaining material in the material cylinder, and set insulation;
When using new plastic, the residual material of the screw barrel should be cleaned thoroughly. When using POM, PVC, PA+GF and other materials, try to minimize the degradation of raw materials, and rinse them with ABS or other water outlet materials in a timely manner after shutdown.