-
E-mail
248693695@qq.com
-
Phone
15268032526
-
Address
Lingang Industrial Park, Shuangqiao Town, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhoushan Jingke Machinery Manufacturing Co., Ltd
Multi layer metal extrusion screw
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
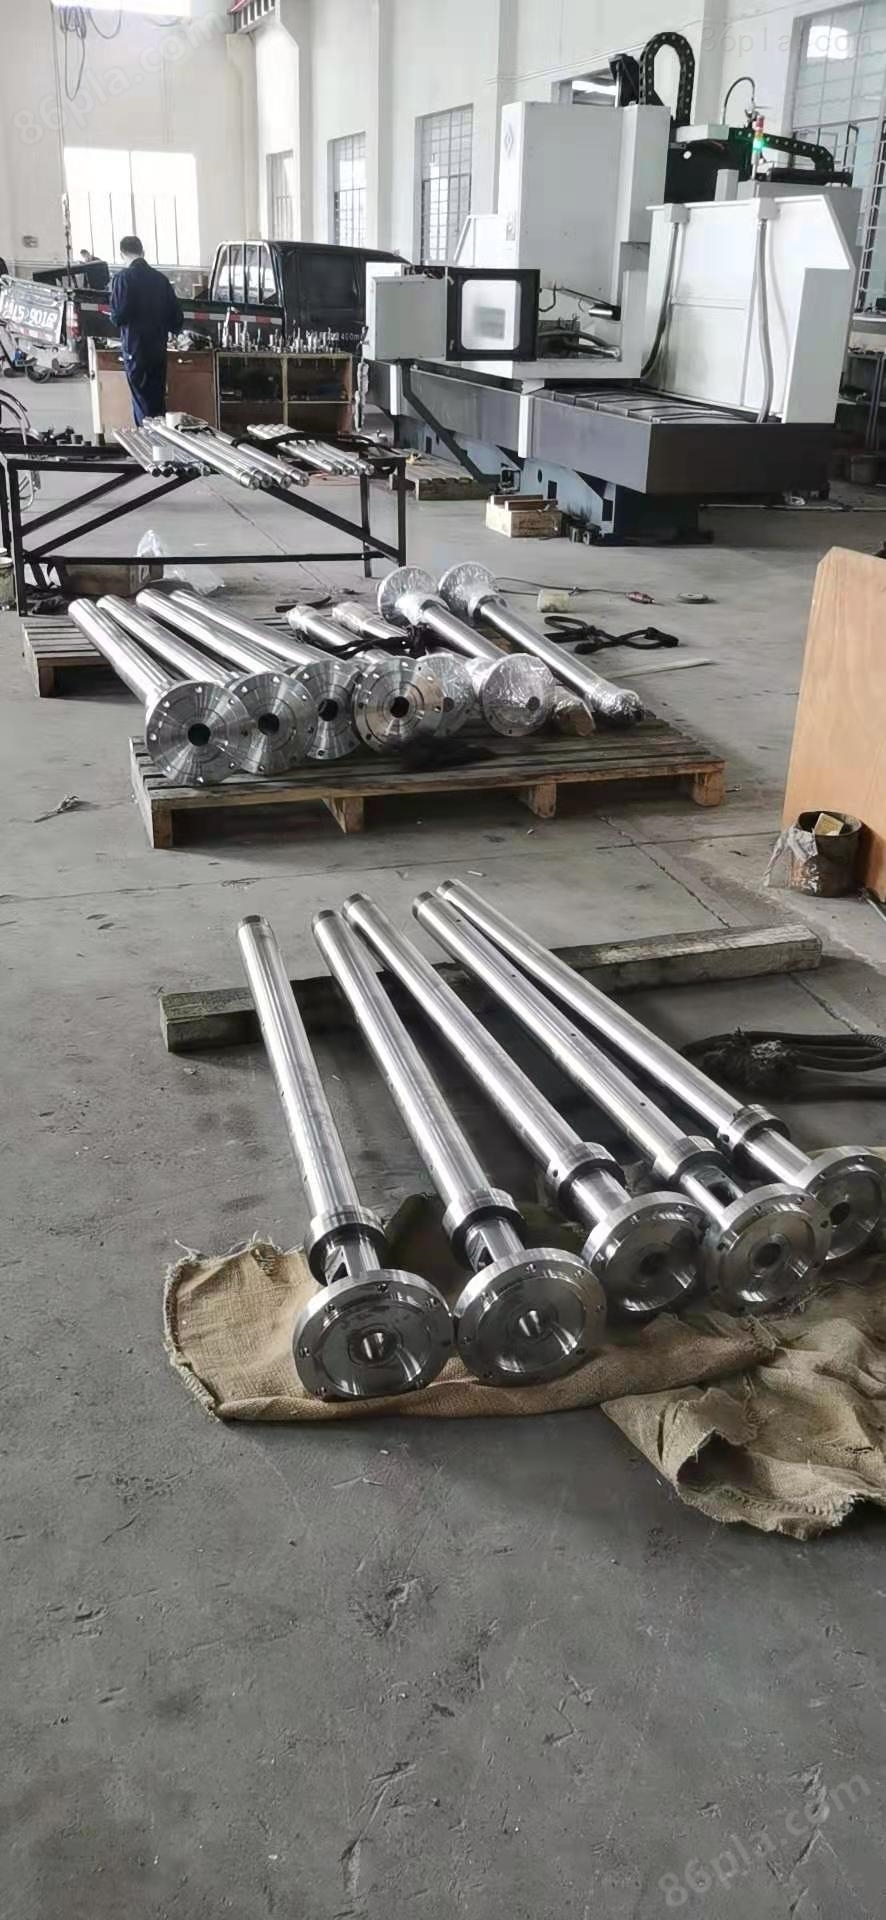
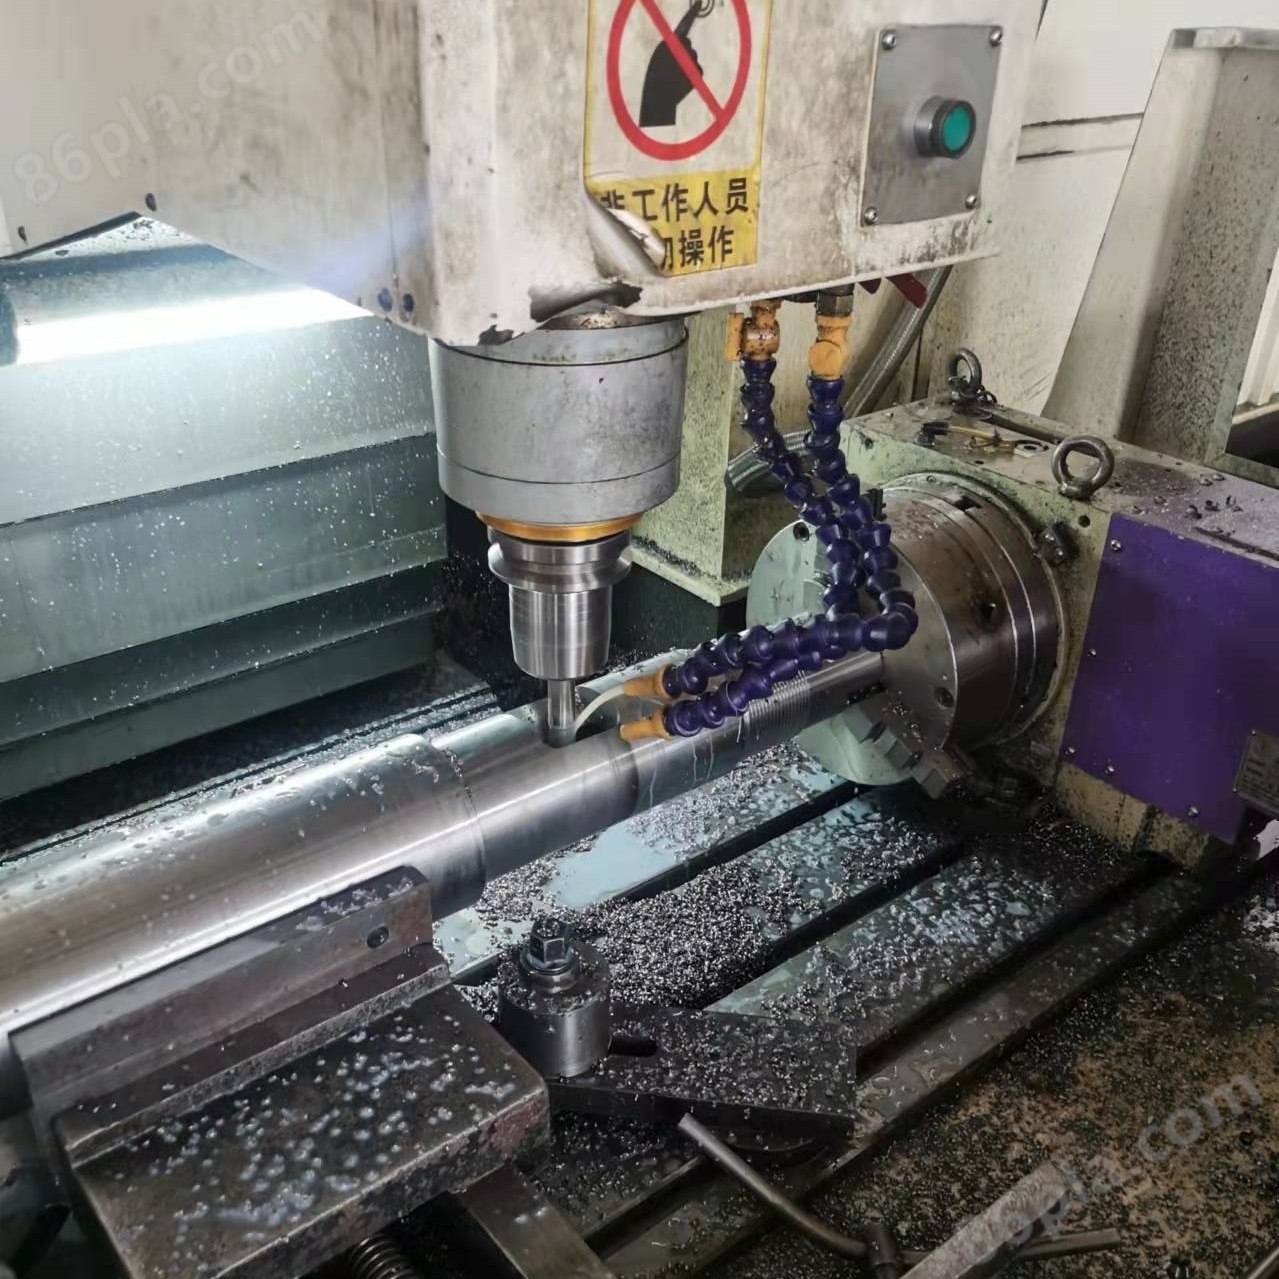
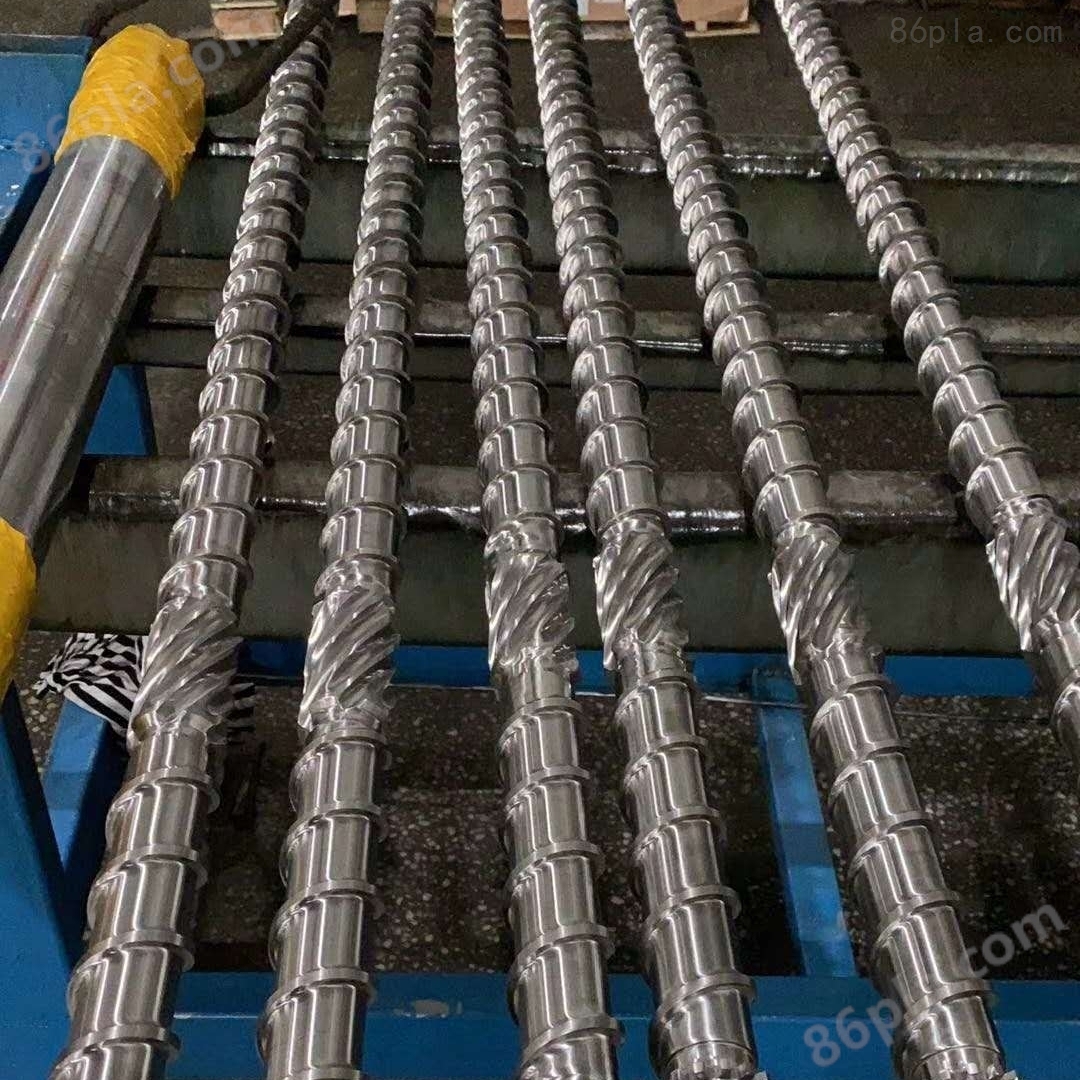
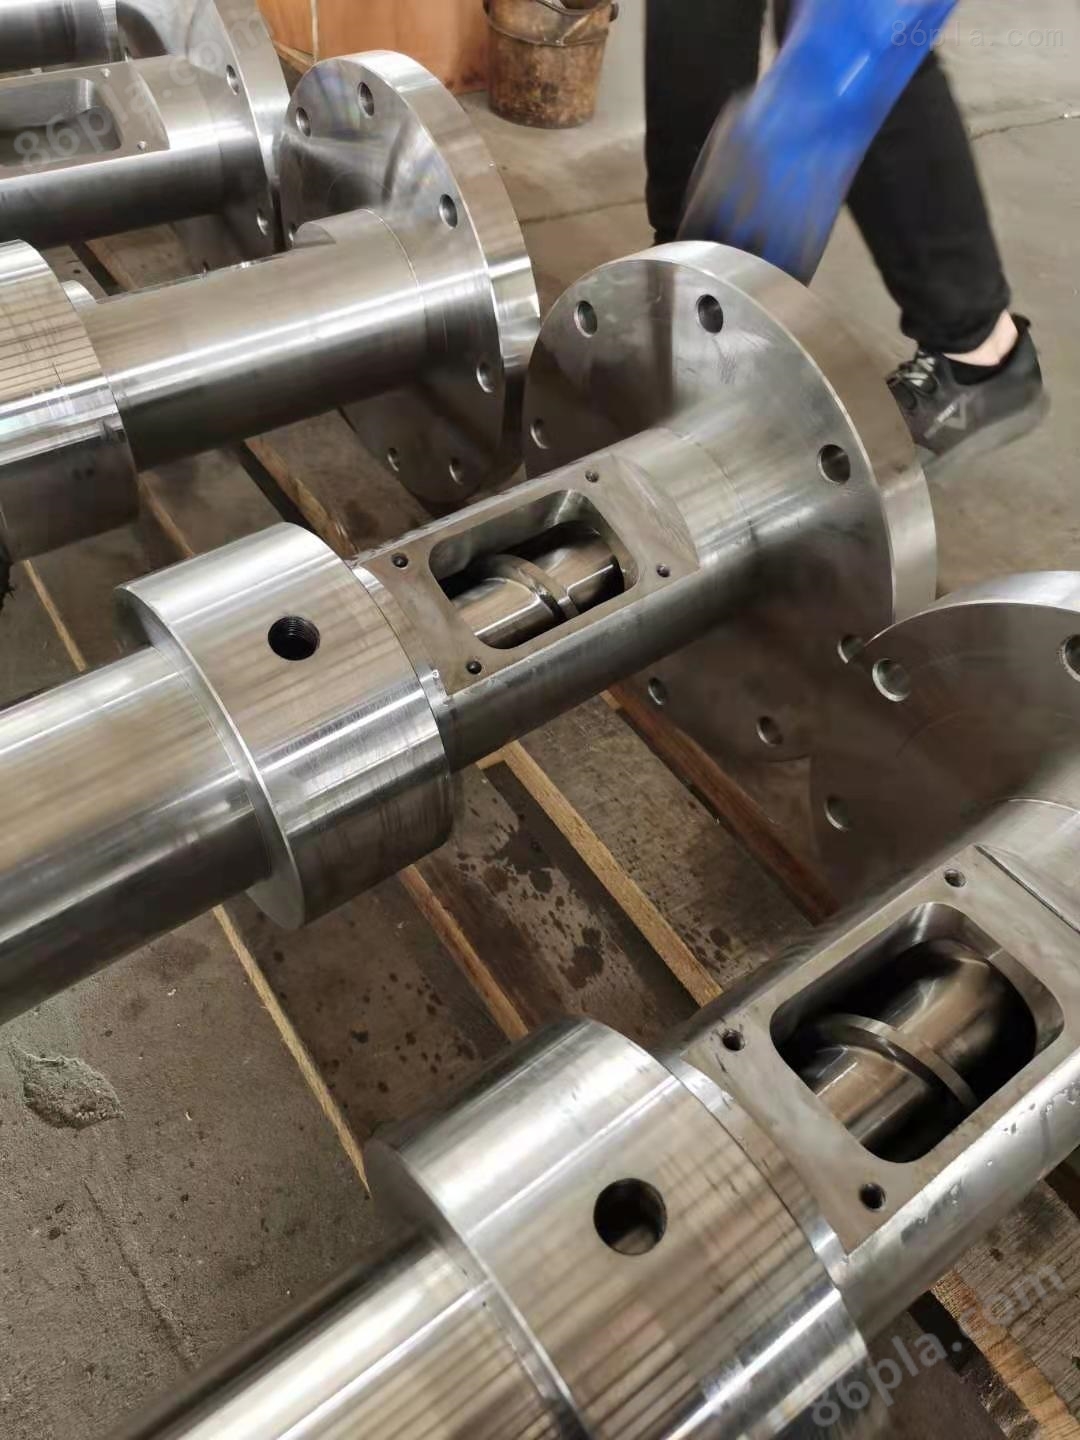
Multi layer metal extrusion screw surface hardness: HV ≥ 900 Nitriding layer depth: 0.5-0.8mm Surface WC/Co integral spray welding, can effectively improve the use of the screw
Product Details
Multi layer metal extrusion screwPrecautions for use:
1) When starting the injection molding machine, the injection molding should be fully preheated. After the material barrel reaches the preset temperature, continue to keep the insulation for 15 minutes for those with a diameter of less than 60mm. After the above 30 minutes, restart the motor to start the screw related actions.
2) The material and screw should be matched. Especially for corrosive and hard materials such as PVC, flame retardant materials, and glass fiber additives, professional screws should be used instead of ordinary screws.
3) When using anti salivation, it is important to ensure that the plastic inside the barrel is melted to prevent damage to the transmission system components when the screw retracts.
4) Avoid phenomena such as screw idling and slipping.
5) Avoid mixing POM and PVC into the material barrel at the same time, as it may react and cause serious industrial accidents at the melting temperature.
Multi layer metal extrusion screwMaintenance:
1. Daily maintenance is a regular routine work that does not take up the operating hours of the equipment and is usually completed during the driving period. The key is to clean the machine, lubricate all moving parts, tighten loose threaded parts, timely inspect and adjust the motor, control instruments, various working components and pipelines, etc.
2. Regular maintenance is generally carried out after the extruder has been running continuously for 2500-5000 hours and then stopped. The machine needs to be disassembled, inspected, measured, and evaluated for the wear of its main components, replaced with parts that have reached the specified wear limit, and repaired for damaged parts.
3. Empty operation is not allowed to prevent the screw and machine from rolling over.
4. If there is any abnormal noise during the operation of the extruder, it should be stopped immediately for inspection or repair.
5. Strictly prevent metal or other debris from falling into the hopper to avoid damaging the screw and barrel. To prevent iron impurities from entering the barrel, magnetic suction components or magnetic frames can be installed at the feeding port of the barrel to prevent impurities from falling in. The materials must be sieved in advance.
6. Pay attention to the cleanliness of the production environment, and do not allow garbage and impurities to mix into the material and block the filter plate, which will affect the product output, quality, and increase the resistance of the machine head.
7. When the extruder needs to be stopped for a long time, anti rust lubricating grease should be applied to the working surfaces of the screw, machine shaft, and machine head. Small screws should be suspended in the air or placed in wooden boxes, and leveled with wooden blocks to prevent deformation or damage to the screws.