- Phone
-
Address
No. 4 Lingang 2nd Road, Shuangqiao Street, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhejiang Zhoushan Huayi Machinery Manufacturing Co., Ltd
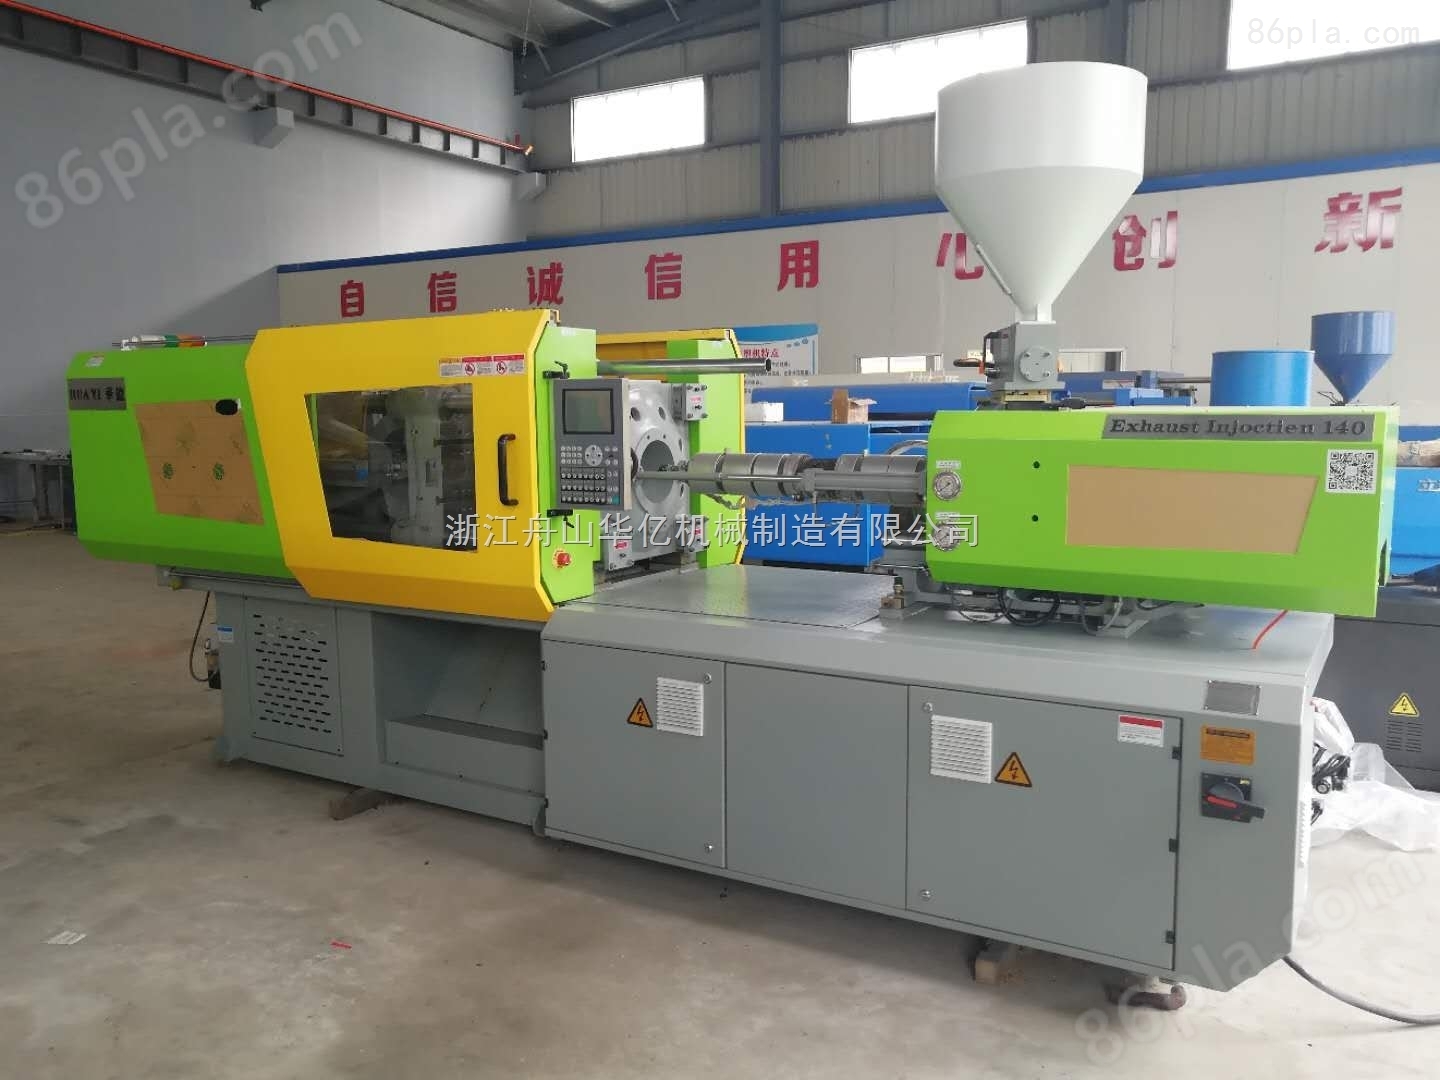
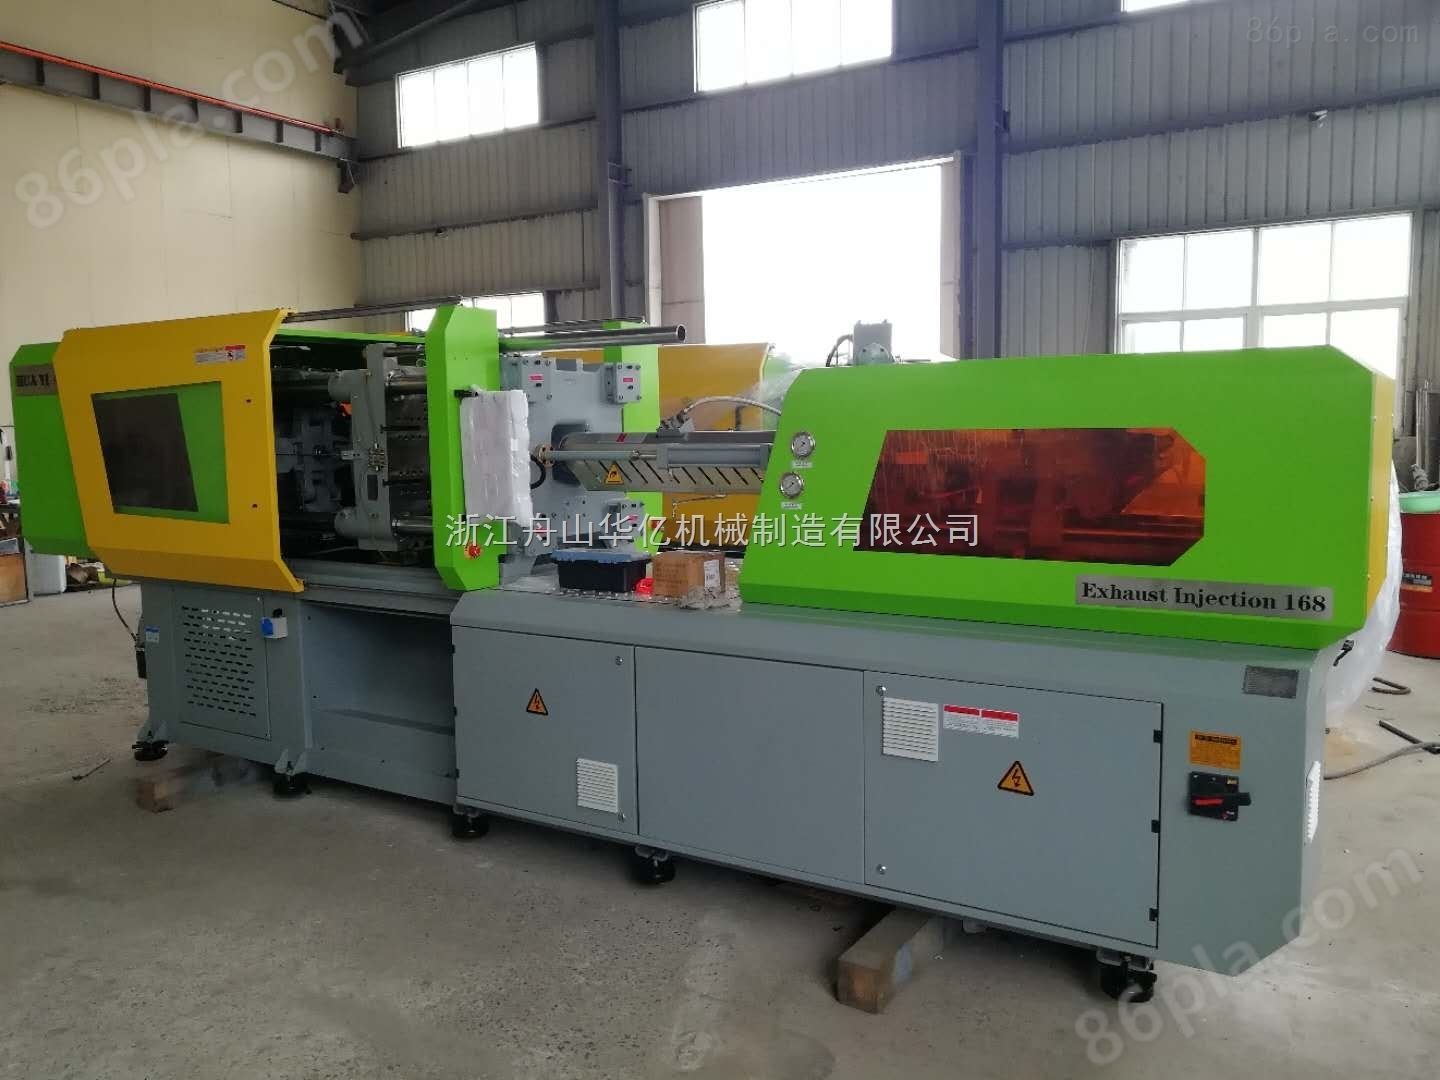
Large exhaust injection molding machine
NegotiableUpdate on 01/17
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
Based on the classic extrusion exhaust theory and the characteristics of exhaust injection molding, a large exhaust injection molding machine was studied for its exhaust mechanism and the design theory of plasticizing components. And many important parameters were measured through experiments. The influence of first-order screw melting characteristics such as screw speed, back pressure, feeding amount, exhaust temperature, and exhaust screw exhaust efficiency.
Product Details
Large exhaust injection molding machinePrecautions
1. Once the operator discovers a machine or electrical malfunction, they should immediately stop the oil pump motor, cut off the power supply, and report to the workshop management personnel.
2. During the injection molding production process, the operator must retrieve the product from the front safety door and must not directly touch high-temperature devices such as heating cylinders with their hands to prevent burns.
3. Operators are not allowed to change any injection molding process parameters without authorization..
4. During the operation of injection molding machines, operators are not allowed to leave their workstations without authorization and are not allowed to discuss topics unrelated to their work with others.
5. Within * minutes of starting (or connecting) the machine, the operator must carefully observe whether the operation of each lubrication slide and ejector pin of the mold is normal and whether there is a lack of lubricating oil; If there is any abnormality, immediately report to the workshop management personnel.
6. During the homework process, the operator must follow the quality inspector's instructions regarding quality. Defective products that have been self inspected must be confirmed by the workshop quality inspector before they can be placed in the waste bin.
7. When handing over the shift, the operator should clearly inform the incoming employee of the important events that occurred during the shift.
Operation requirements for large exhaust injection molding machines:
1. Before starting production with machine heating, open the cooling water valve and observe whether the water channel is unobstructed.
2. Close the power switch next to the control box, connect the internal power supply, and press the motor start button on the panel to start the oil pump motor.
3. For machines that are used for the first time or have not been used for a long time, after starting the oil pump, they should be run empty for a few minutes before starting the operation.
4. Turn on the heating switch of the material cylinder, connect the electric heating power supply, adjust the constant temperature nozzle and temperature controller on the box door, set the temperature, and observe the current of the ammeter to determine the quality of the electric heating coil.
5. The test run should be carried out sequentially from manual to semi-automatic to fully automatic, and important fastening bolts should be checked for looseness. If any abnormalities are found, they should be stopped immediately. After confirming normal operation or troubleshooting, proceed with the test drive.
6. When the processing stops or the material is changed, the material cylinder should be cleaned. The cleaning work should be carried out while the material cylinder is heated. After the cleaning is completed, immediately turn off the heating switch. Cleaning work is particularly important for processing easily degradable plastics.
Similar Product Recommend