-
E-mail
248693695@qq.com
-
Phone
15268032526
-
Address
Lingang Industrial Park, Shuangqiao Town, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhoushan Jingke Machinery Manufacturing Co., Ltd
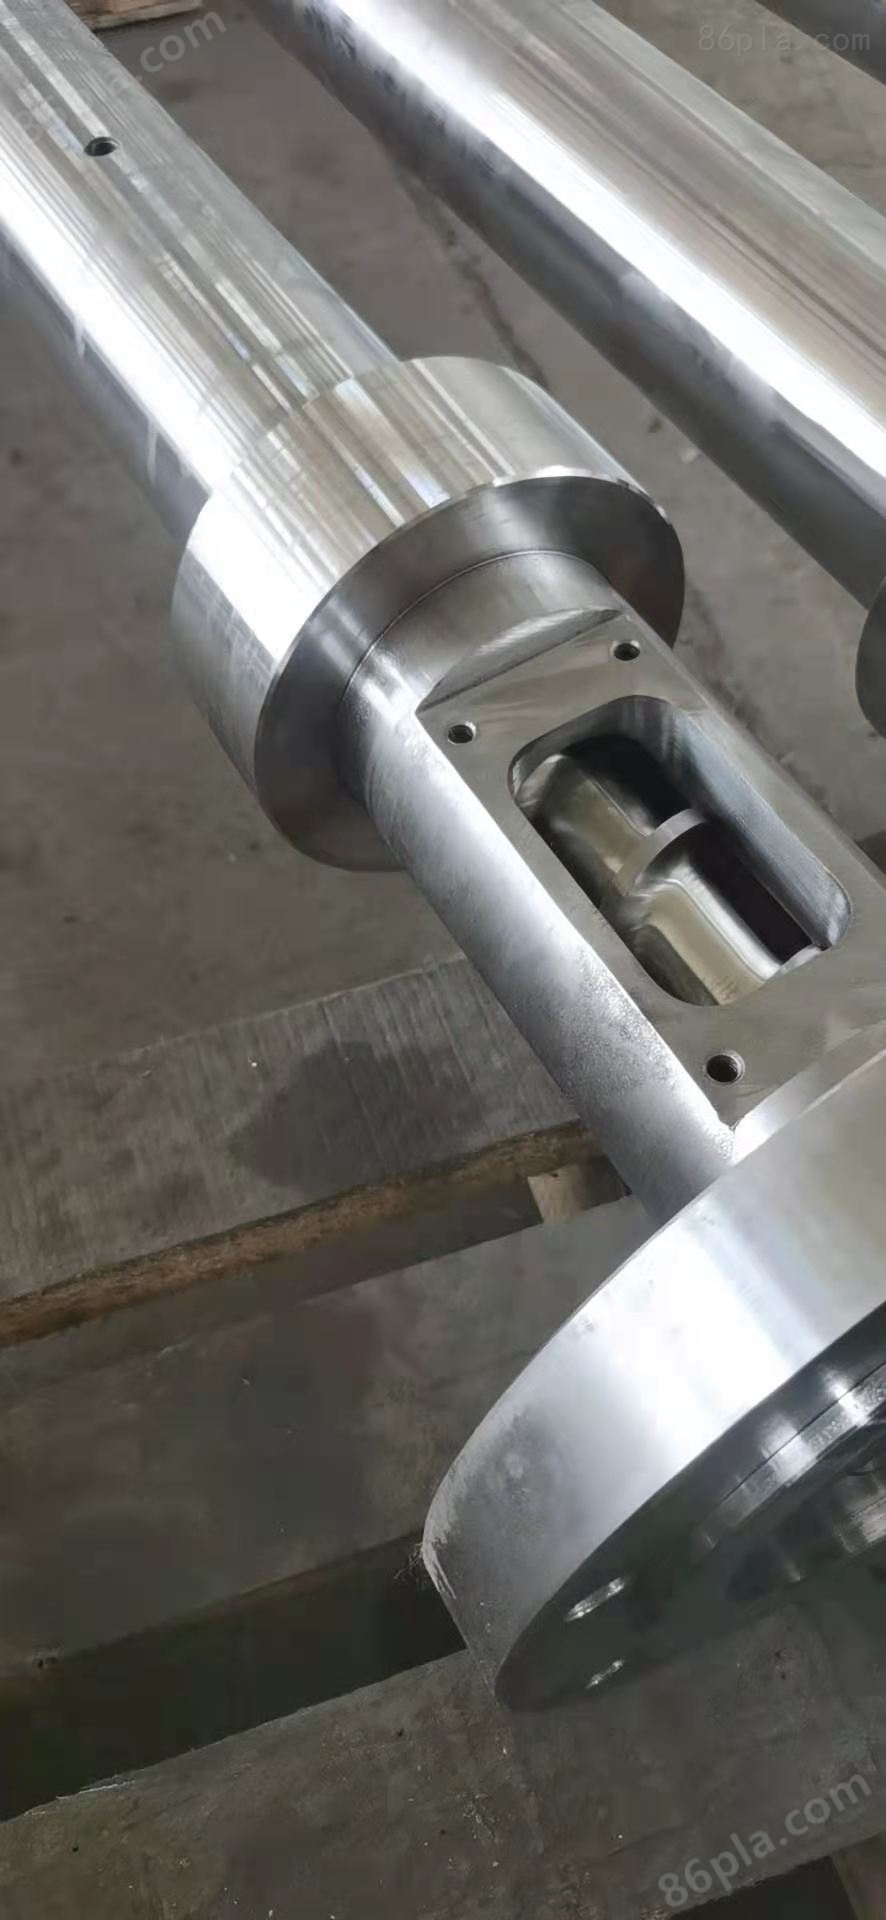
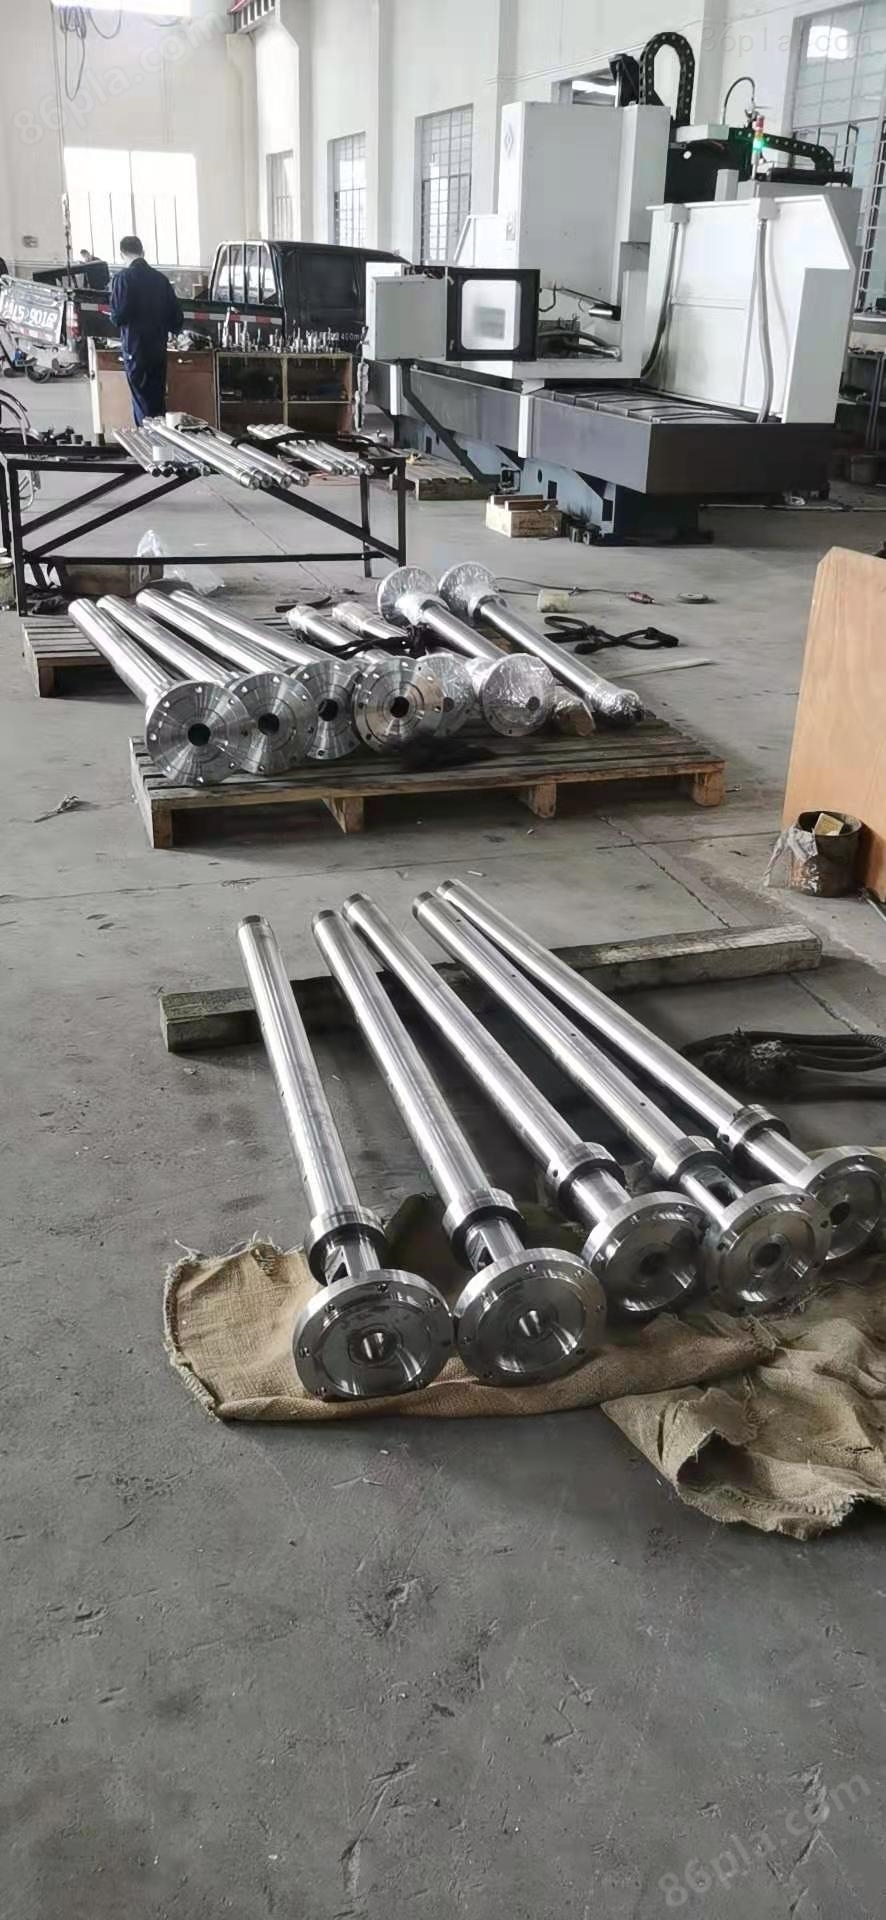
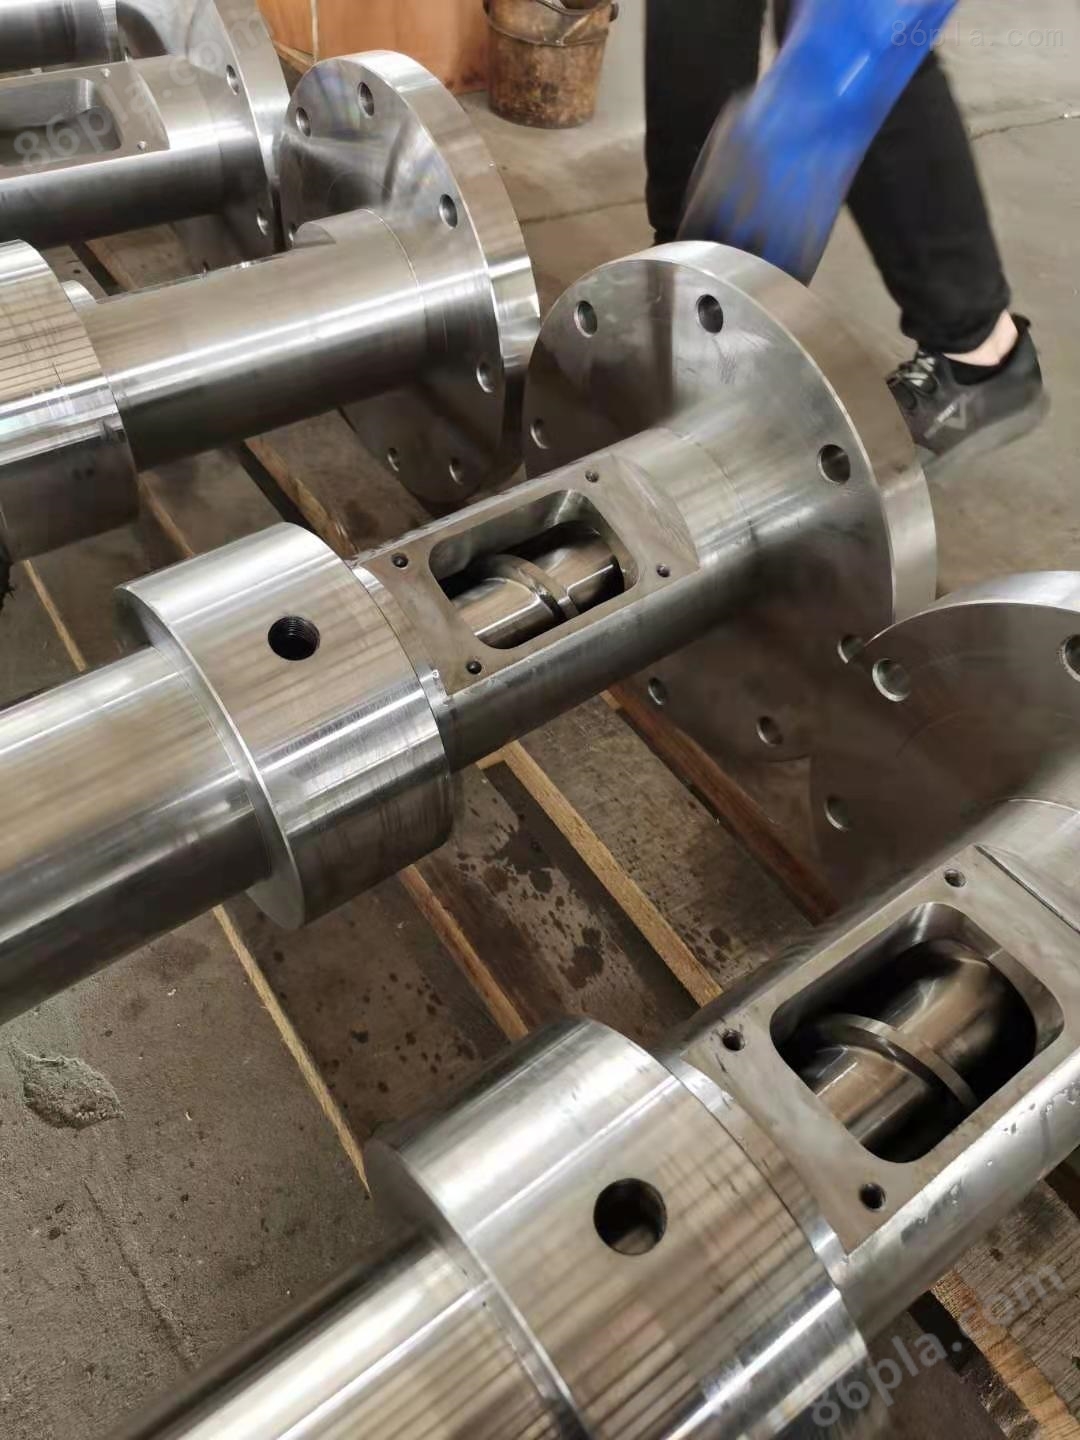
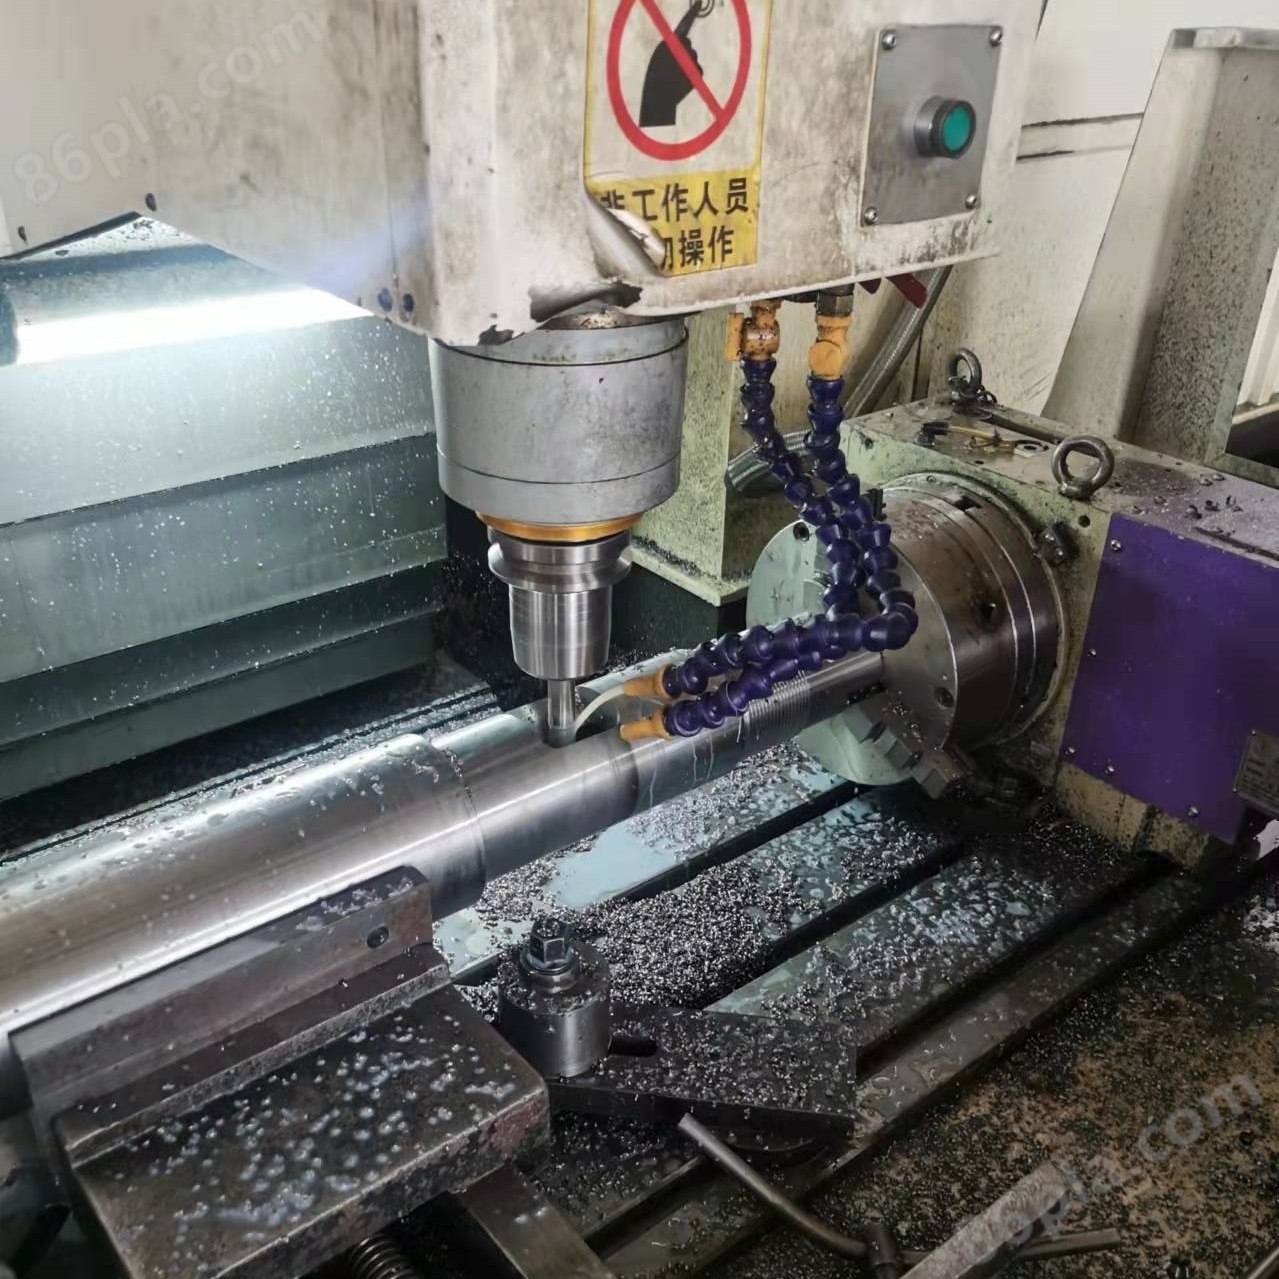
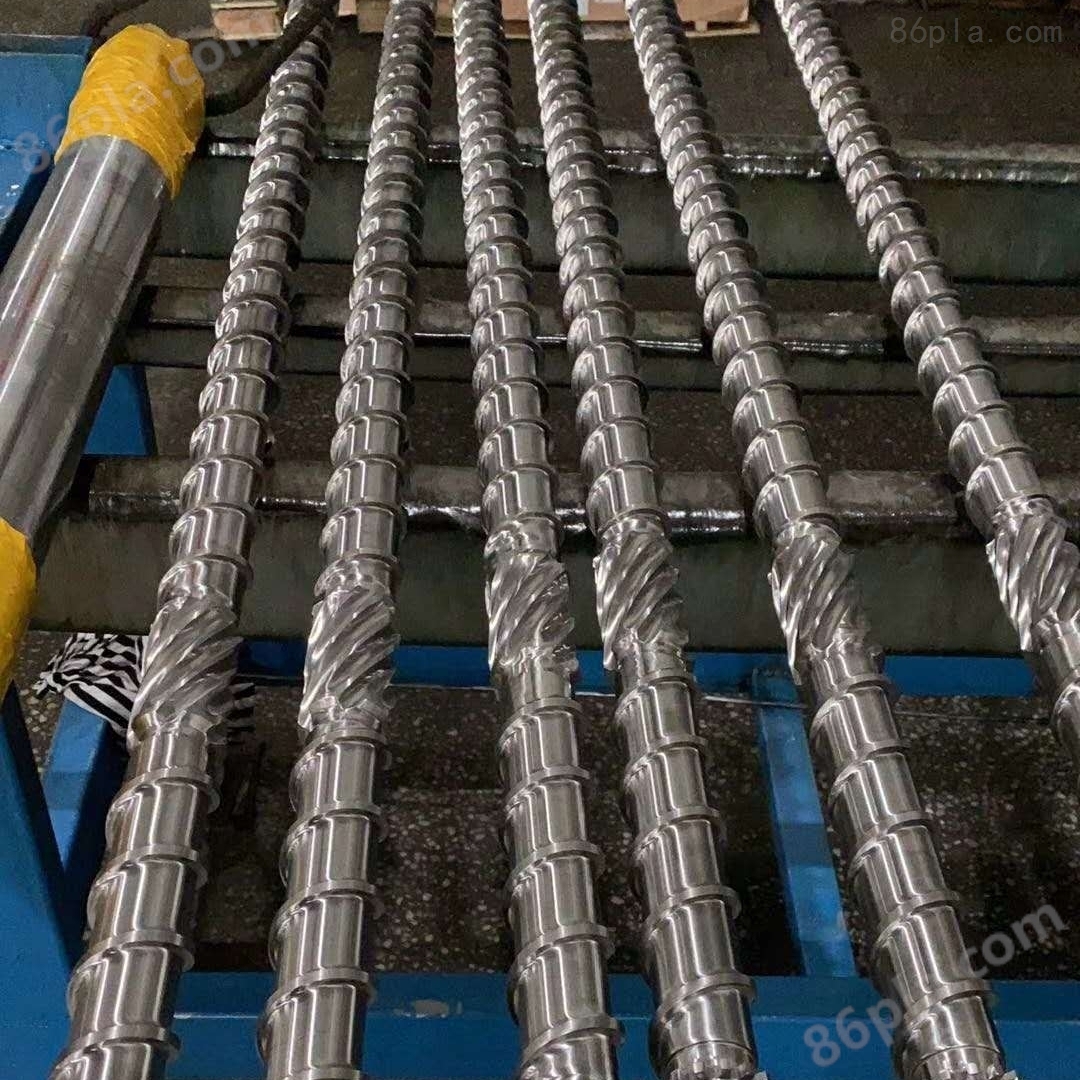
Jingke multi-layer screw
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The Jingke multi-layer screw is made of high nickel alloy and tungsten carbide special formula with alkane bonding. Has characteristics of wear resistance, corrosion resistance, high temperature resistance, and high pressure resistance; Hardness can reach HRC62-70 amp; amp; amp; amp; amp; amp; amp; amp; amp; amp; amp; amp; amp; amp; #176;; Applicable temperature ≤ 600; Its effective service life is greatly improved.
Product Details
Precautions for Jingke multi-layer screw:
1. Screw manufacturing should use wear-resistant alloy steel with minimal deformation in high-temperature environments. After precision machining, the working surface of the screw should be wear-resistant and corrosion-resistant. Therefore, the threaded part of the screw should be treated with nitriding and plated with a hard chromium layer, with a hardness of 700-800HV.
2. During idle testing, be careful not to let the screw run for a long time without air; During the trial operation and debugging, the idle running time should exceed 3 minutes
3. The disassembly of the screw can generally be done by pushing out the screw from the rear or using a tool to pull out the screw.
4. After cleaning the screw and its connected components, the working surfaces should be inspected for scratches and friction damage. Minor scars should be repaired with fine sandpaper or oilstone.
5. When serious wear and deep grooves appear on the working surface of the screw, the cause of the damage should be analyzed and identified, the fault should be eliminated to avoid similar phenomena from happening again, and then the worn scars should be treated. If both the screw and the barrel are severely worn, the actual clearance between the two components should be checked first. If it exceeds the standard requirements by a lot, the screw should be replaced at this time.
6. When assembling the screw, a layer of molybdenum disulfide heat-resistant grease should be applied to the joint surface with other parts to facilitate the next disassembly.
7. Temporarily unused screws should be coated with a layer of protective oil after surface cleaning, wrapped and hung in a dry and ventilated place.
Jingke multi-layer screwPrecautions for use:
1. Do not put anything other than plastics, pigments, and additives into the hopper. If a large amount of crushed secondary materials are used, a hopper magnet should be added to prevent metal fragments from entering the melt adhesive cylinder and damaging the melt adhesive screw and cylinder.
2. When the adhesive has not reached the pre adjusted temperature, do not start the hydraulic motor to melt, spray or loosen the adhesive, otherwise it will cause damage to the screw and adhesive head kit.
3. When using (loosening), prevent the plastic inside the melt adhesive cylinder from hardening due to low temperature. Otherwise, when the screw retracts, the hardened plastic will adhere to the front end of the rod to prevent damage to the rotating system components when the screw retracts.
4. When the machine is shut down for a long time, the plastic inside the melt adhesive cylinder should be cleaned properly first to prevent the plastic with high heat sensitivity from carbonizing and firmly adhering to the injection screw, which cannot rotate. When using highly corrosive raw materials, special attention should be paid to this, as this type of plastic can easily damage the inside of the material tube and the nitride layer on the surface of the injection screw if it stagnates inside the material tube.
5. Regularly inspect all parts of the injection platform, lock and loosen the parts, and ensure that the two injection oil cylinders are installed in a balanced manner to prevent damage to the oil seal of the cylinder, which may cause oil leakage and wear of the cylinder piston rod.
6. The electric heating element near the nozzle must not be wrapped in plastic, as it is easy for the electric heating element to be damaged due to poor heat dissipation caused by plastic wrapping.