-
E-mail
248693695@qq.com
-
Phone
15268032526
-
Address
Lingang Industrial Park, Shuangqiao Town, Dinghai District, Zhoushan City, Zhejiang Province
Product Categories
Zhoushan Jingke Machinery Manufacturing Co., Ltd
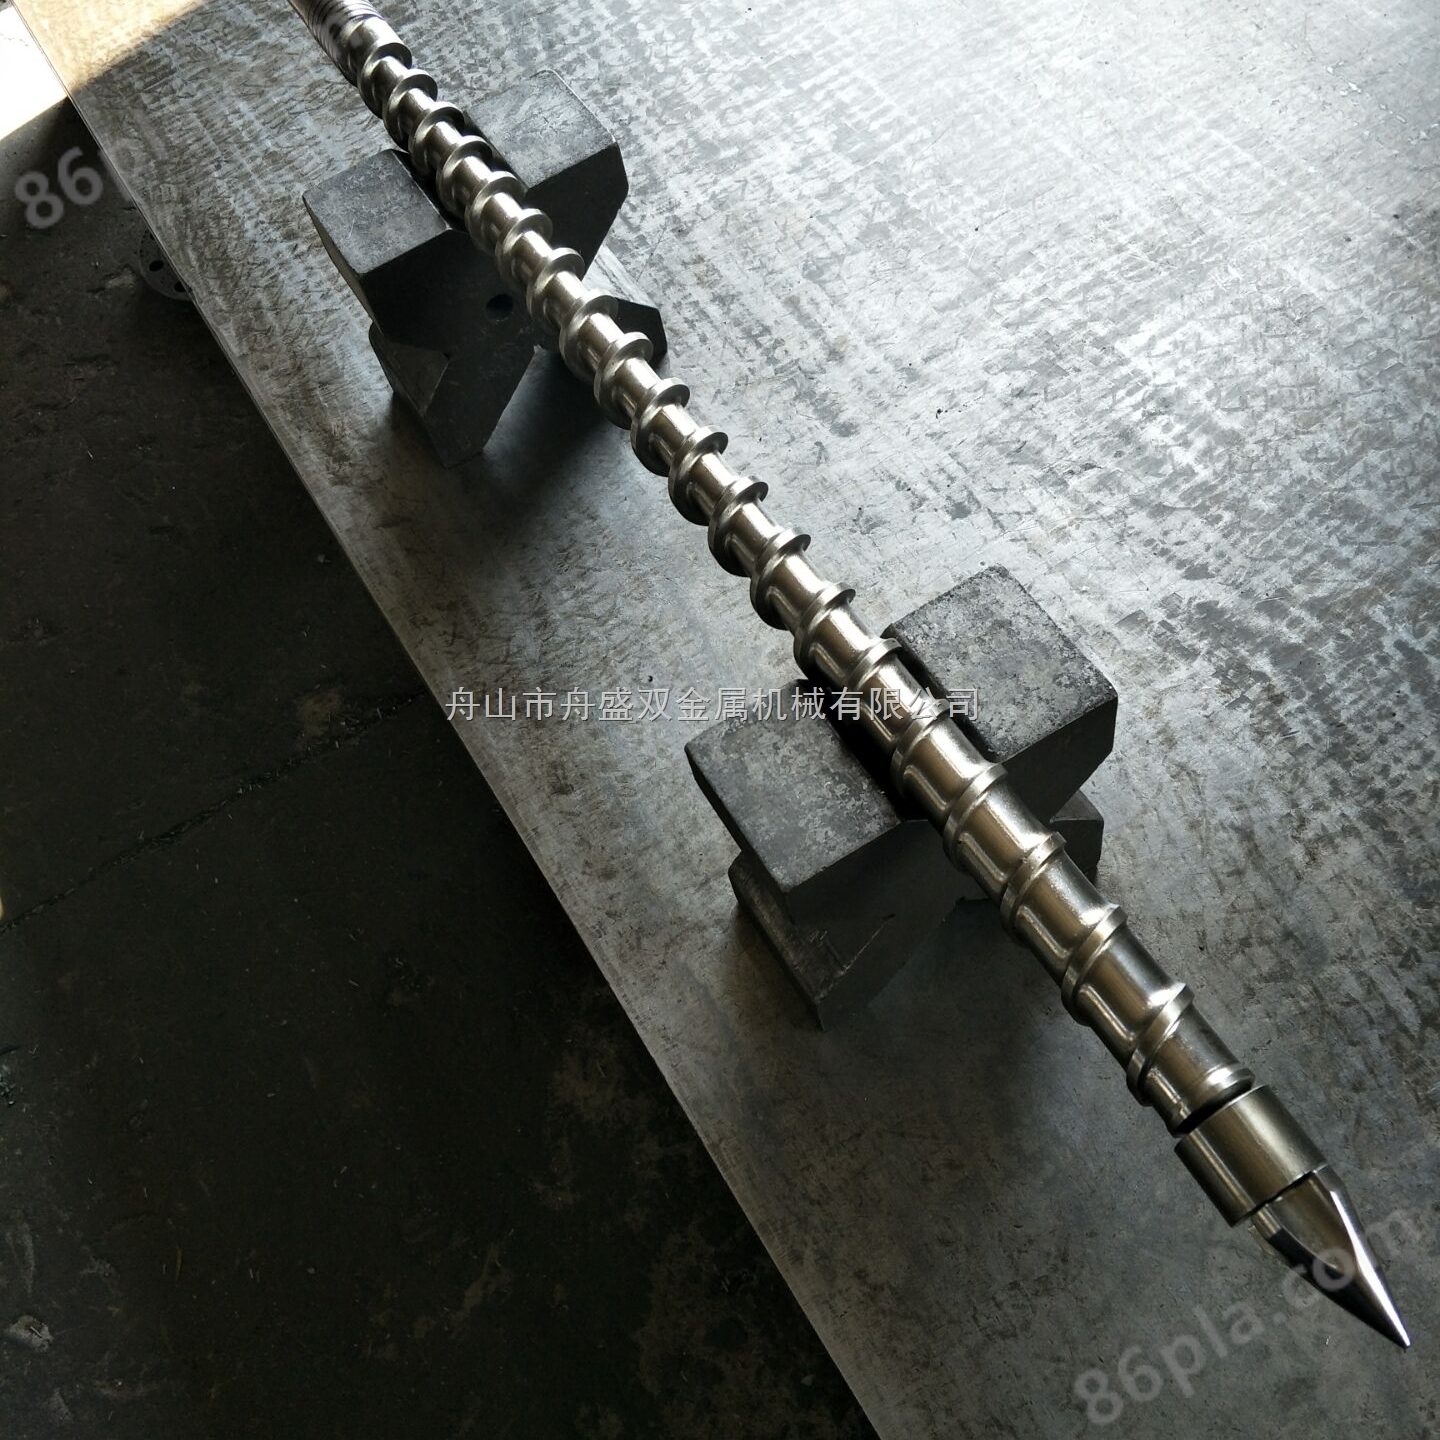
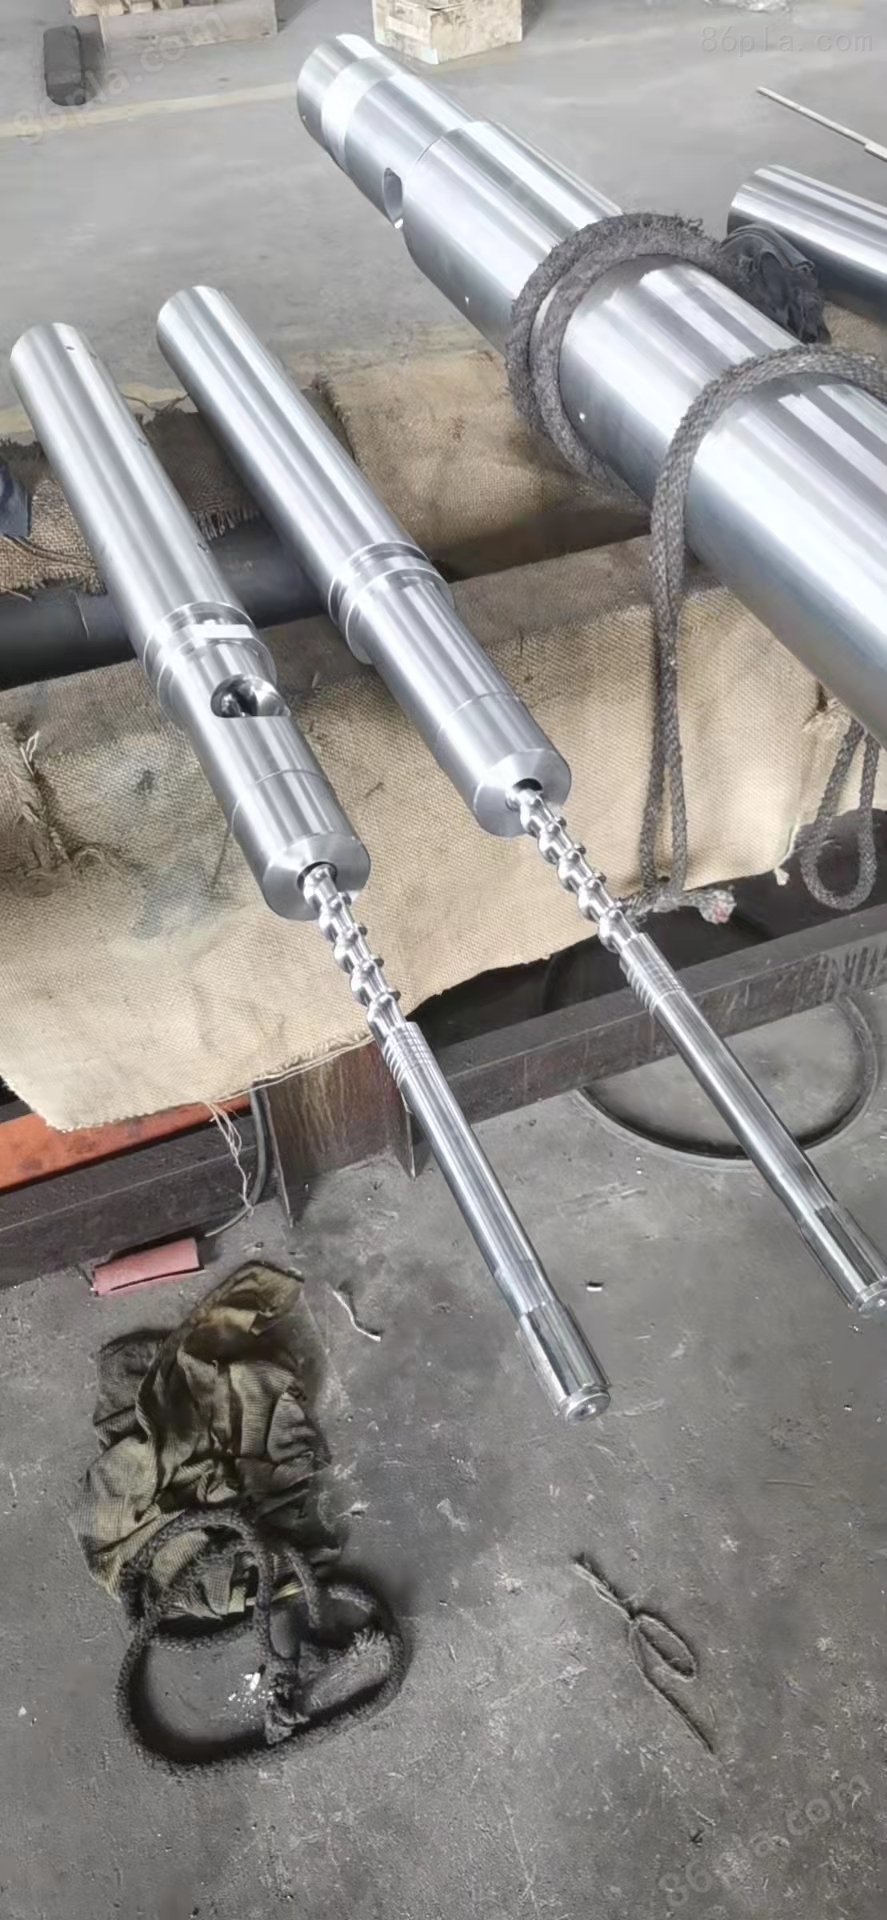
Halogen-free multi-layer screw
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
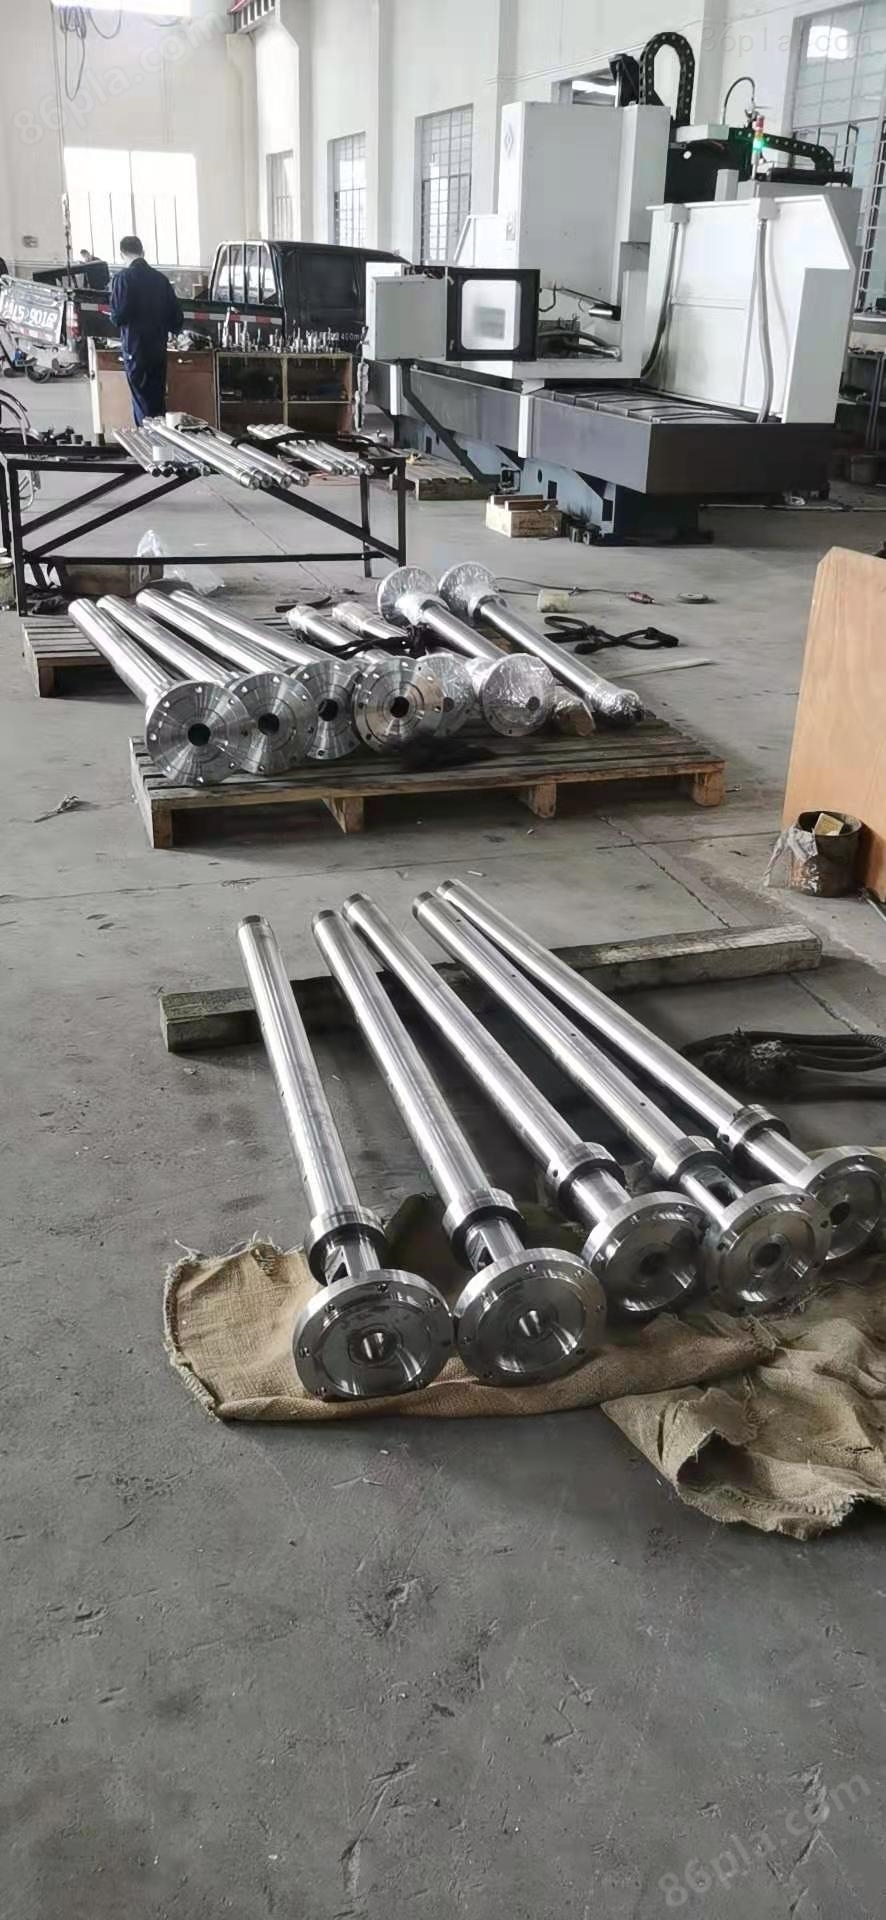
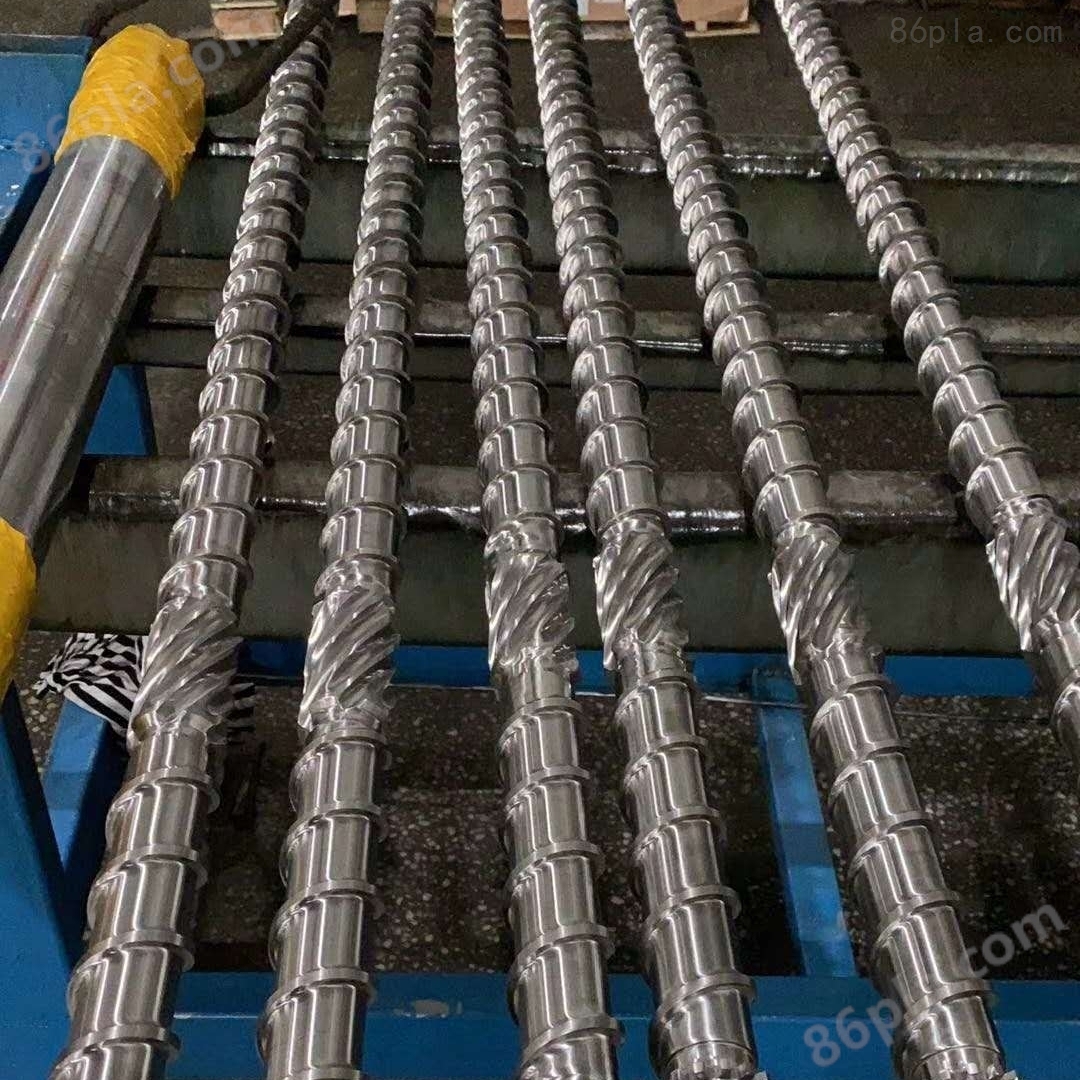
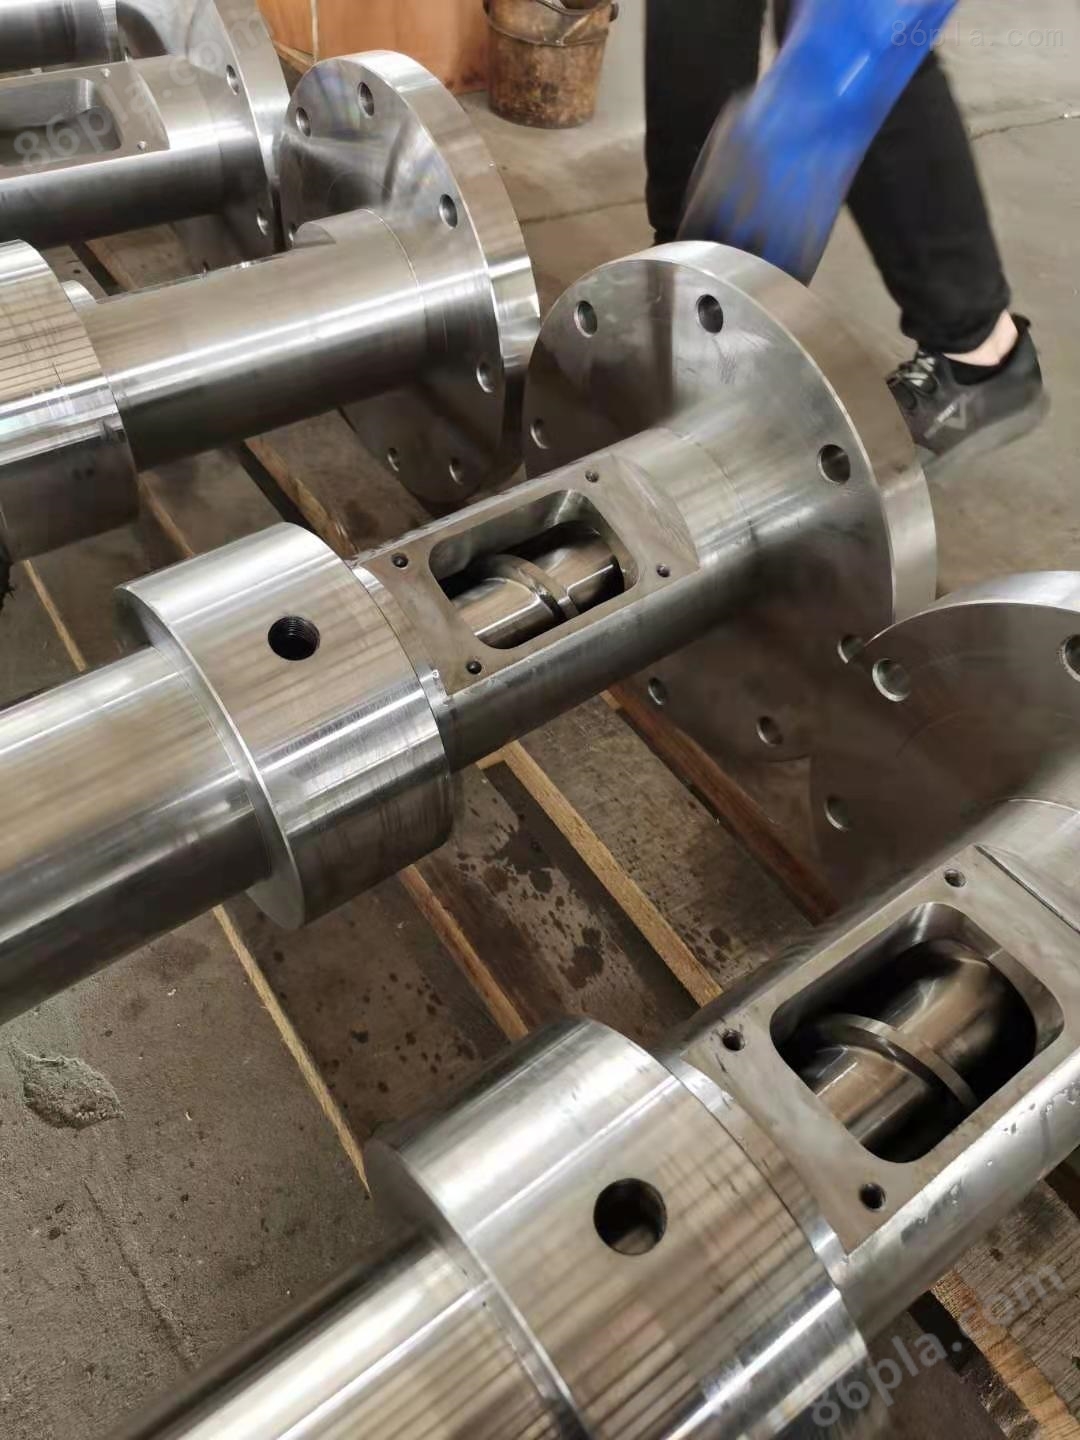
The halogen-free multi-layer screw has the characteristics of high strength, corrosion resistance, high temperature resistance, and wear resistance. Its usage time exceeds that of ordinary barrel screws by more than half, reducing the usage and labor costs of many injection molding machine factories.
Product Details
Halogen-free multi-layer screwFeatures:
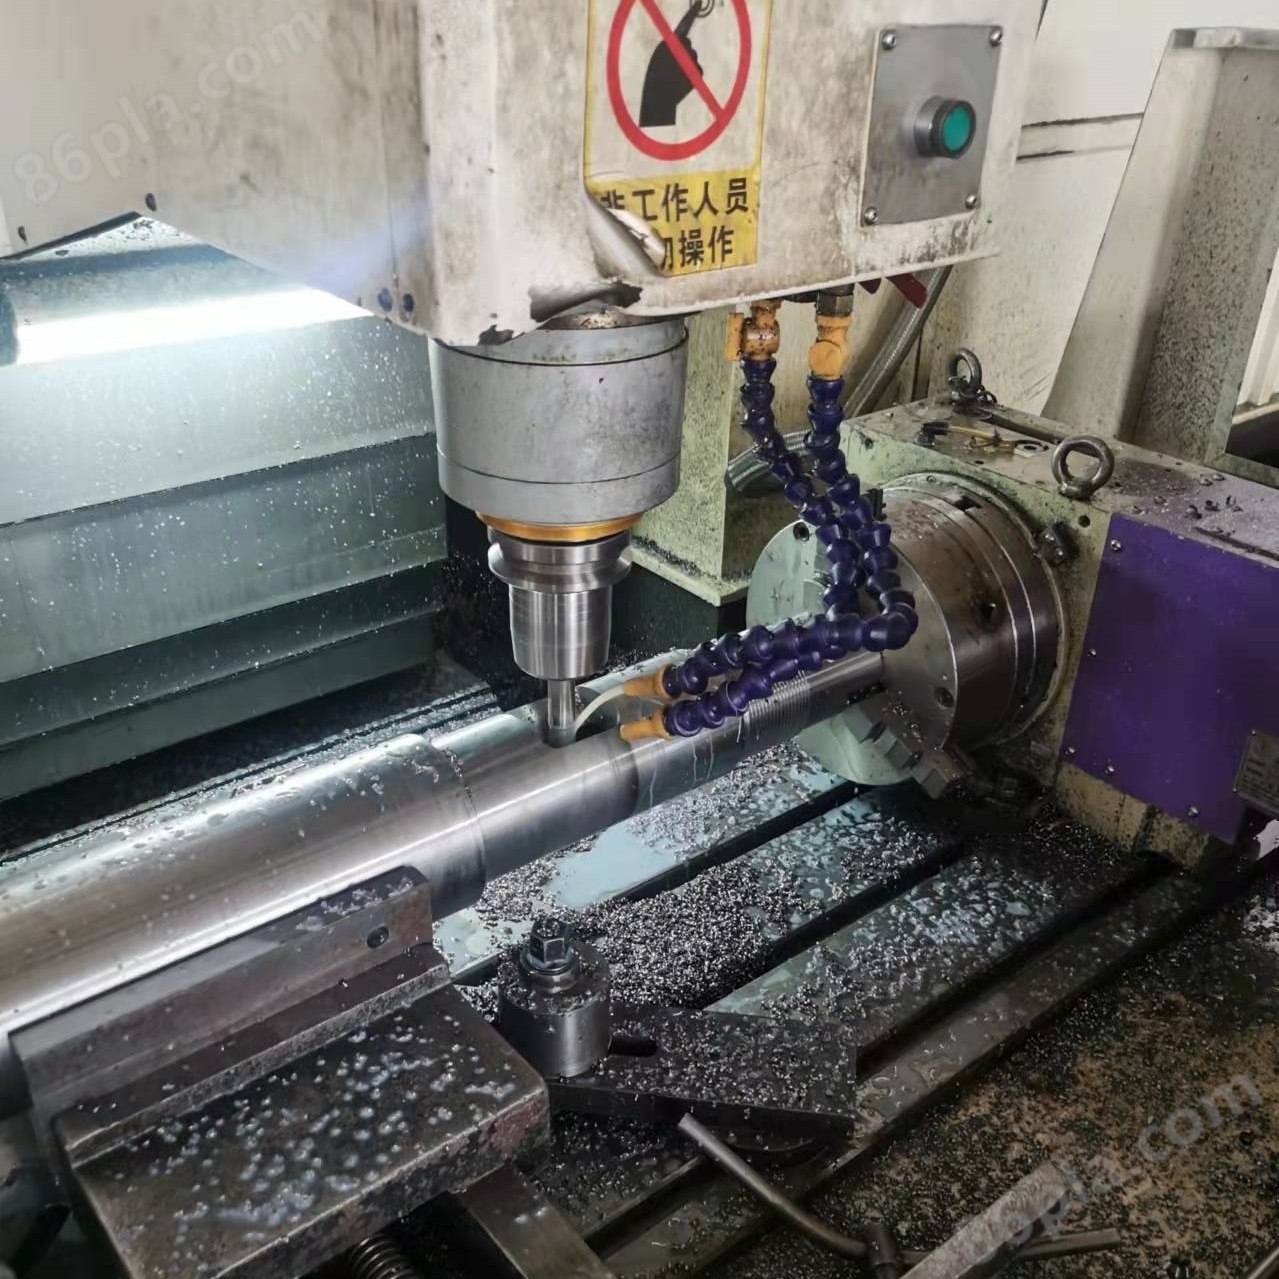
It has comprehensive properties such as high wear resistance, high hardness, and high temperature resistance, and its service life is generally more than 10 times that of general alloy steel. We use ultra-fine particle hard alloy materials, combined with our company's efficient processing equipment and advanced processing technology, to produce products with good cross-sectional crack resistance strength. At the same time, we can produce a large amount of cutting heat and rubber melt coating under harsh working conditions without being affected by corrosion, bringing excellent production efficiency to your machine
Precautions for halogen-free multi-layer screws:1. Screw manufacturing should use wear-resistant alloy steel with minimal deformation in high-temperature environments. After precision machining, the working surface of the screw should be wear-resistant and corrosion-resistant. Therefore, the threaded part of the screw should be treated with nitriding and plated with a hard chromium layer, with a hardness of 700-800HV.
2. During idle testing, be careful not to let the screw run for a long time without air; During the trial operation and debugging, the idle running time should exceed 3 minutes
3. The disassembly of the screw can generally be done by pushing out the screw from the rear or using a tool to pull out the screw.
4. After cleaning the screw and its connected components, the working surfaces should be inspected for scratches and friction damage. Minor scars should be repaired with fine sandpaper or oilstone.
5. When serious wear and deep grooves appear on the working surface of the screw, the cause of the damage should be analyzed and identified, the fault should be eliminated to avoid similar phenomena from happening again, and then the worn scars should be treated. If both the screw and the barrel are severely worn, the actual clearance between the two components should be checked first. If it exceeds the standard requirements by a lot, the screw should be replaced at this time.
6. When assembling the screw, a layer of molybdenum disulfide heat-resistant grease should be applied to the joint surface with other parts to facilitate the next disassembly.
7. Temporarily unused screws should be coated with a layer of protective oil after surface cleaning, wrapped and hung in a dry and ventilated place.