-
E-mail
13962469131@163.com
-
Phone
13962469131
- Address
Product Categories
Suzhou Haoda Machinery Co., Ltd
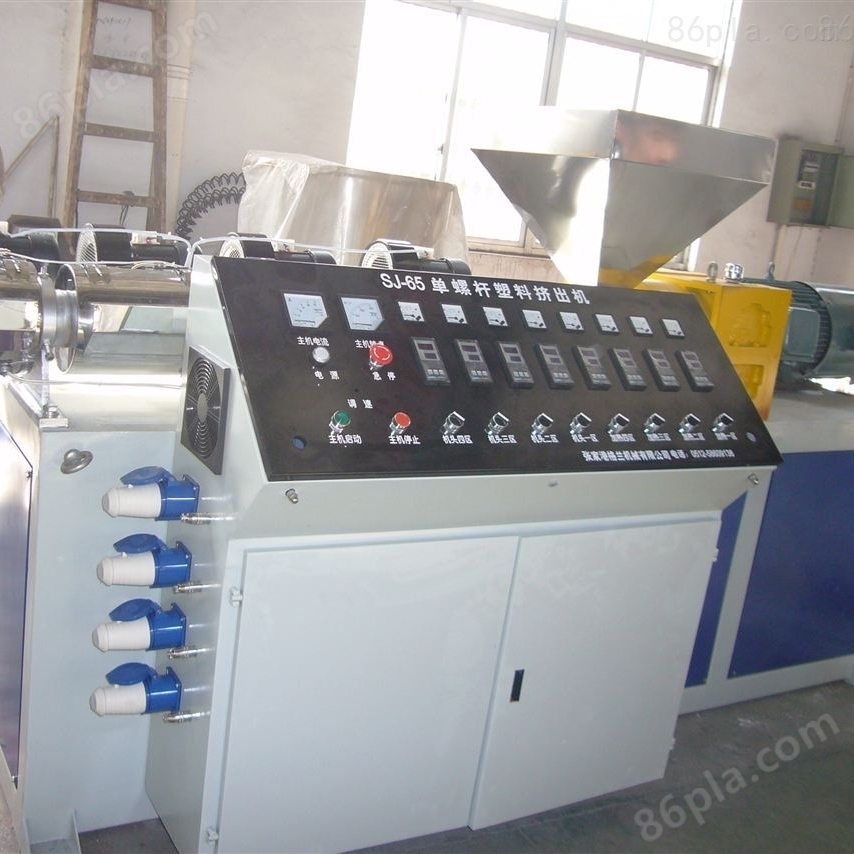
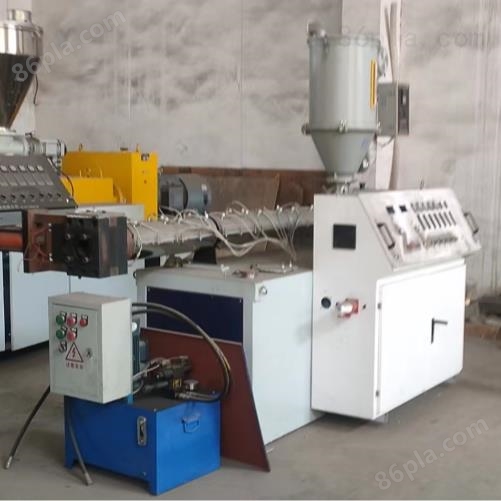
Sj series screw extrusion equipment
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The sj series screw extrusion equipment is mainly used for extruding thermoplastic plastics such as soft and hard polyvinyl chloride, polyethylene, etc. It can be used in conjunction with corresponding auxiliary machines (including molding heads) to process various plastic products, such as film tubes, plates, wires, belts, etc. It can also be used for granulation. Advanced design, high output, good plasticization, low energy consumption, using involute gear transmission, with low noise, smooth operation, high load-bearing capacity, and long service life.
Product Details
Sj series screw extrusion equipmentdrive
① Add qualified plastic into the hopper, open the insert plate, and start the screw to continue running the glue. The operator should pay attention to the feeding situation and observe the indications of the ammeter and voltmeter pointers when running the glue. At this time, the operator is not allowed to leave the work post to prevent problems from occurring.
② After the plastic is extruded from the mold sleeve, the plasticization of the plastic should be observed. When the plasticization of the plastic is good, the mold should be calibrated to adjust the thickness of the plastic evenly and prevent deviation of the plastic layer.
③ Sample and inspect the thickness of the plastic according to the process regulations, and check the quality of the extruded plastic, such as pores, surface plasticization, lumps, etc.
④ After everything is normal and production meets the requirements of the process regulations, the crew should be actively organized to start the operation. During the operation, they should divide the work and cooperate closely.
⑤ When threading the lead wire and starting the traction, the speed of the screw and traction should be controlled according to the thickness requirements of the plastic layer specified in the process, so that the wires and cables can be neatly arranged on the winding reel of the wiring device after passing through the traction. When threading wires, a dedicated person should be assigned to follow the wire connector, taking care to prevent water from entering the wire and cable or the connector from getting stuck.
⑥ Verify the zero position of the meter counter and ensure accurate measurement. When coiling wires and cables, the unqualified joint wires must be cut off, and the thickness and eccentricity must be checked until they are qualified before coiling.
⑦ Pay attention to the following points at all times during normal production: product quality, observe and test the surface quality of the plastic layer and the outer diameter of the product at all times; Pay attention to the operation of each mechanical part of the equipment; Observe the temperature control of the heating system; Pay attention to the changes in screw and traction speed to ensure the uniformity of extrusion thickness and product outer diameter; Be diligent in measuring outer diameter, inspecting quality, and observing equipment; Pay attention to adding materials in a timely manner to avoid glue breakage, delamination, and package leakage; If you notice burning while driving, you should immediately stop and clean the car; If it is found that the insulation is not qualified and needs to be peeled off, it is not allowed to split it by oneself. The wire core should be opened to the length for processing to avoid short ends or waste.
⑧ Keep a good record of the process quality of the product. Remember labels, tracking cards, production reports, process record sheets, etc.
8. Parking
When parking, first cut off the traction current, and then stop the main motor. Open the bolts at the connection between the extruder head and the machine body, turn off the insertion plate of the feeding hopper, move the head away, and remove the plastic from the barrel and screw. Organize personnel to promptly remove the mold core and sleeve, clean the machine head and sieve plate.
① When encountering the following situations, stop and clean the machine head: stop and clean the machine head in a timely manner after production is completed; When the temperature control is too high and plastic burning occurs, the machine head and screw should be stopped and cleaned; Park for more than an hour and clean the engine head; If there are other reasons for parking, such as power outage, water outage, waiting for power lines, waiting for equipment, or in case of equipment or personal accidents, the machine head must be cleaned.
② The machine head and screw should be cleaned thoroughly, and after cleaning, the machine head and screw should be installed in a timely manner.
③ Keep a handover diary and prepare for production for the next shift, such as molds, production trays, semi-finished products, etc.
④ According to job responsibilities, arrange personnel to be responsible for the cleaning and sanitation of the equipment.
⑤ After parking, check the power supply, water source, gas source, and various parts of the equipment. After confirming that there are no problems, turn off the power supply, gas source, and water source before leaving the machine.
Sj series screw extrusion equipmentMaintenance and upkeep:
1、 Cleaning
1. Before cleaning, turn off the power first and wait for the extruder to cool to room temperature.
2. Use detergent and clean water for cleaning, be careful not to let water flow into the interior of the machine.
3. The concentration of the cleaning solution should be controlled at around 3%, and the operating temperature should be between 50 ℃ and 60 ℃.
4. The cleaning time should be determined according to the frequency of use and the usage environment. Generally, a deep cleaning should be carried out every 3 months.
After rinsing, the machine should be dried using an electric fan.
2、 Lubrication
1. The extruder needs to be regularly lubricated to reduce wear and friction, and maintain machine stability.
2. It is recommended to choose suitable lubricating oil and replace it regularly according to the frequency of use, usually every 500 hours.
3. The lubricated parts include sliding components, gears, and bearings, etc. Attention should be paid to the amount of lubricating oil dripped, the uniform application, and the cleanliness of the surrounding area.
3、 Testing
1. The testing should include the inspection of the mechanical components and electrical control system of the machine.
2. Mechanical component testing includes adjusting and replacing clamps, locators, safety devices, etc. to maintain their stability and safety.
3. The testing of the electrical control system should include circuit breakers, fuses, wiring terminals, etc. to ensure its normal operation.
Similar Product Recommend