-
E-mail
geqianshun@vip.sina.com
-
Phone
18913397620,13951770588
-
Address
Chenggong Industrial Park, Lukou Town, Jiangning District, Nanjing City
Product Categories
Nanjing Shengchi Rubber Machinery Manufacturing Co., Ltd
Screw type automatic parallel extrusion equipment
NegotiableUpdate on 02/08
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
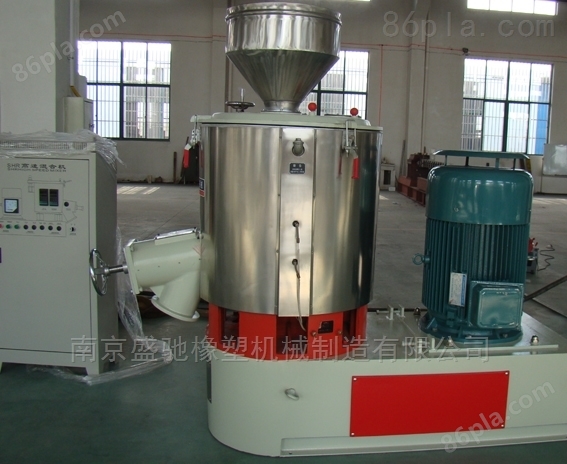
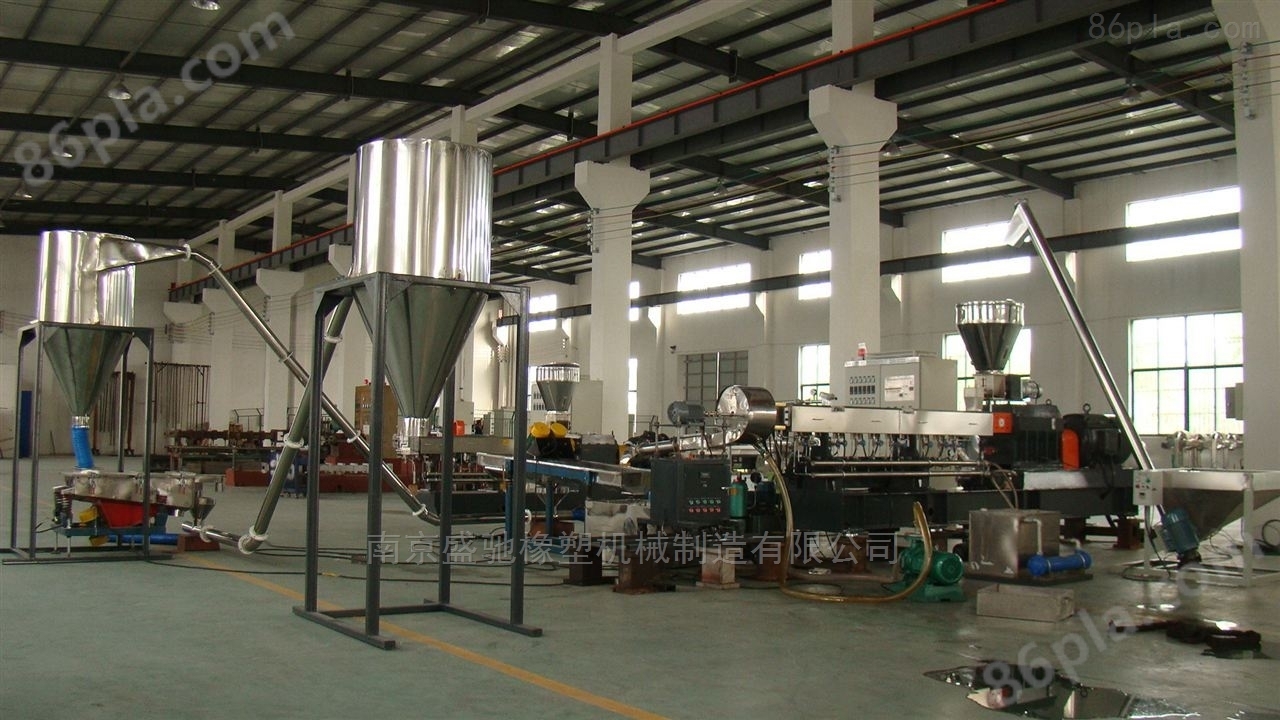
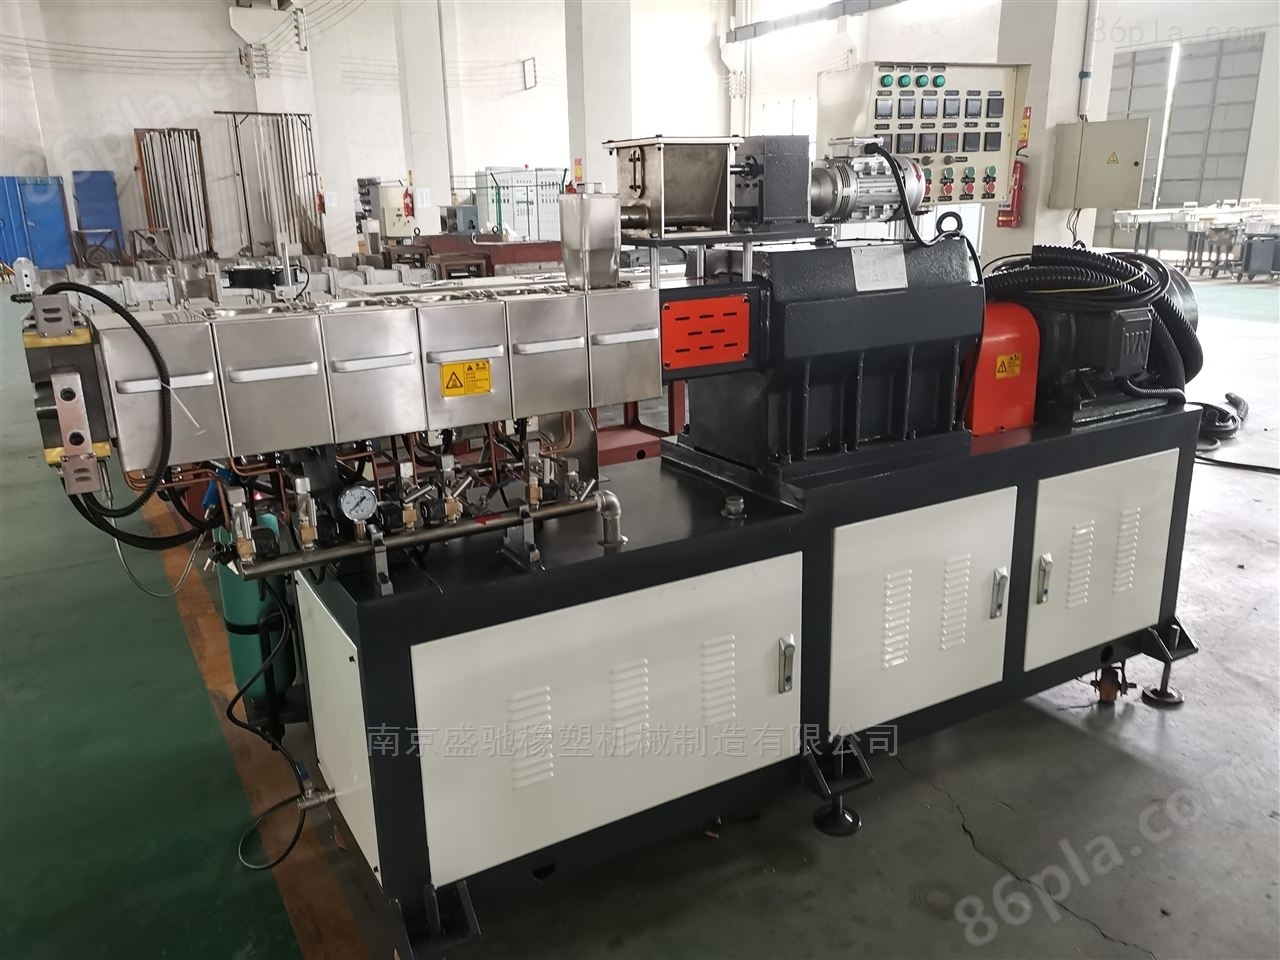
Screw type automatic parallel extrusion equipment should be engaged in the research, development, and manufacturing of twin-screw extruders, twin-screw extruder barrels, SHJ-35 twin-screw extruders, co directional parallel twin-screw extruders, and spare parts for twin-screw extruder manufacturers
Product Details
Screw type automatic parallel extrusion equipmentCorrect stopping sequence:
1. Firstly, we need to feed the twin-screw extruder. Conventional extruders have feeders or feeding systems. When using a multi-channel supply system, it is necessary to stop each auxiliary supply machine.
2. If the twin-screw extruder has a vacuum exhaust system, we need to close the valve of the vacuum pipeline and then open the upper cover plate of the vacuum chamber.
3. The screw of the twin-screw extruder cannot stop rotating directly, and the method of gradually reducing the screw rotation speed should be adopted to remove the residue inside the cylinder as much as possible.
4. When using heat sensitive materials that are prone to thermal decomposition as raw materials for twin-screw extruders, replace the residual materials in the main body with polyolefin materials before stopping, and stop the main body after the materials are basically discharged.
5. Stop the main motor cooling fan, oil pump, vacuum pump, and pump of the twin-screw extruder in sequence. Cut off the power switch of each section heater on the electrical meter control panel and stop auxiliary equipment such as the pellet machine.
Features of screw type automatic parallel extrusion equipment:
1. The screw thread structure of twin-screw extruders is single head, variable pitch, variable depth convergent, and conical propulsion. Two screws rotate in opposite directions, meshing as a whole and assembled with a certain angle, making the flow of rubber material smoother. The working ability of screw extrusion and conveying rubber material is greatly improved.
2. The feeding opening of the barrel is large, and the bottom end has a downward wave structure. The barrel wall is equipped with a clamp type cooling water channel, which has a significant heat dissipation effect, making the rubber material flow smoothly, without arching, burning, or bonding. There is no residual rubber material in the barrel.
3. The surface of the screw and the inner surface of the barrel are coated with a thick layer of wear-resistant hard chromium, which is wear-resistant and corrosion-resistant, greatly improving the service life of the twin-screw extruder equipment.
Similar Product Recommend