-
E-mail
geqianshun@vip.sina.com
-
Phone
18913397620,13951770588
-
Address
Chenggong Industrial Park, Lukou Town, Jiangning District, Nanjing City
Product Categories
Nanjing Shengchi Rubber Machinery Manufacturing Co., Ltd
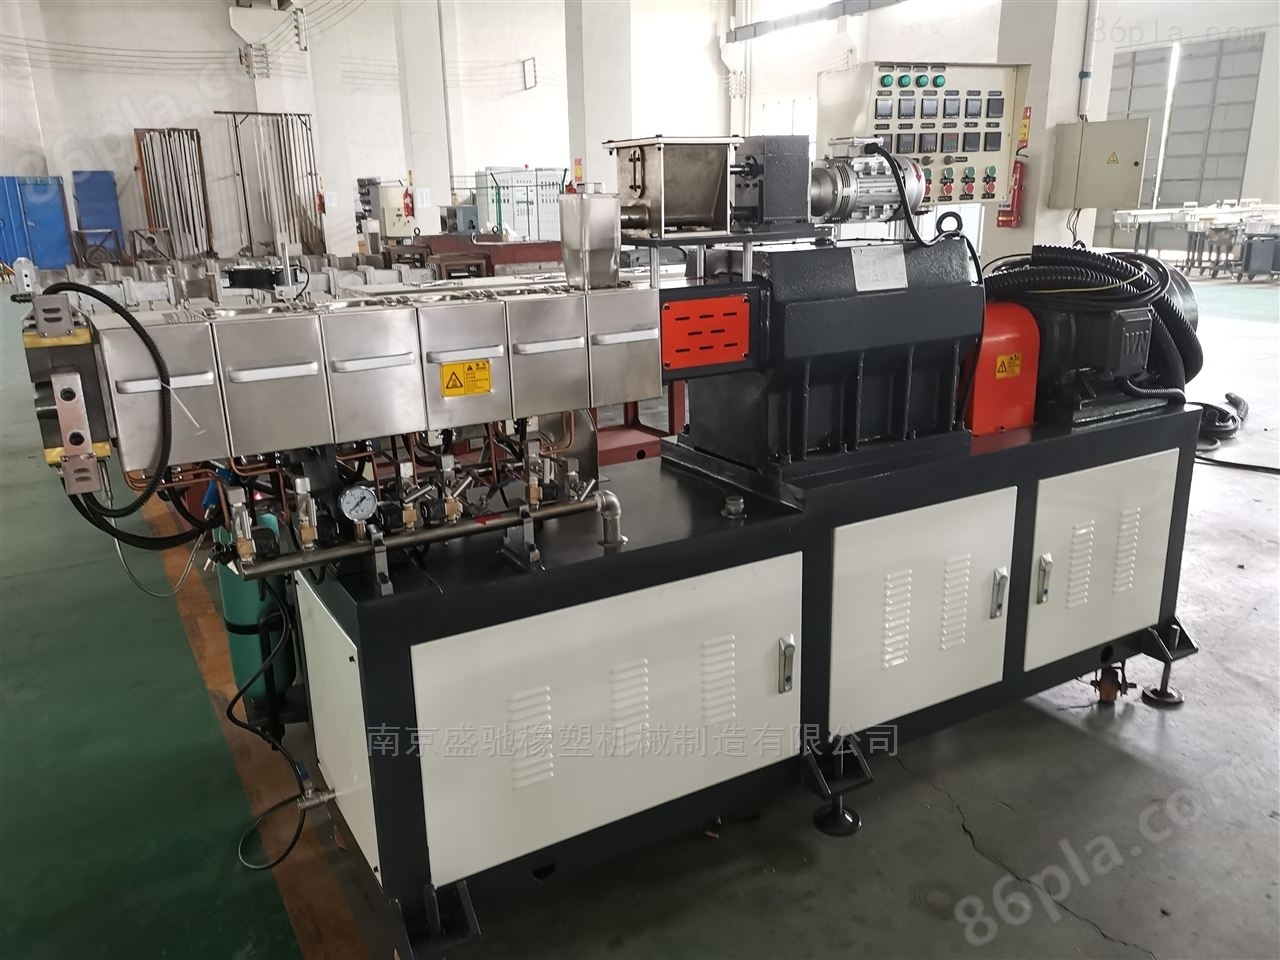
Parallel twin-screw extruder
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The parallel twin-screw extruder is mainly engaged in the research, development, and manufacturing of twin-screw extruders, twin-screw extruder barrels, SHJ-35 twin-screw extruders, co directional parallel twin-screw extruders, and spare parts for twin-screw extruder manufacturers
Product Details
Characteristics of parallel twin-screw extruder:
1. The screw thread structure of twin-screw extruders is single head, variable pitch, variable depth convergent, and conical propulsion. Two screws rotate in opposite directions, meshing as a whole and assembled with a certain angle, making the flow of rubber material smoother. The working ability of screw extrusion and conveying rubber material is greatly improved.
2. The feeding opening of the barrel is large, and the bottom end has a downward wave structure. The barrel wall is equipped with a clamp type cooling water channel, which has a significant heat dissipation effect, making the rubber material flow smoothly, without arching, burning, or bonding. There is no residual rubber material in the barrel.
3. The surface of the screw and the inner surface of the barrel are coated with a thick layer of wear-resistant hard chromium, which is wear-resistant and corrosion-resistant, greatly improving the service life of the twin-screw extruder equipment.
4. The equipment can directly control the speed of the screw and roller, and achieve mutual matching, so that the rolled film can be continuously connected and more compact, neat, and smooth.
5. The overall design of the twin-screw extruder is compact, efficient, and easy to assemble, apply, and maintain
Inspection of parallel twin-screw automatic extruder
1. It is necessary to regularly calibrate temperature control instruments and check their correctness of adjustment and sensitivity of control.
2. Regularly check the water quality of the cooling water tank, and replace it promptly if it becomes turbid.
3. Check if the solenoid valve is working properly, and replace the coil promptly if it is burnt out.
4. Timely clean the dirt in the vacuum tank and the materials in the exhaust chamber to keep the pipeline unobstructed.
5. The DC motor that drives the screw to rotate must be carefully inspected for brush wear and contact.
6. The insulation resistance value of the motor should be measured regularly to check if it is above the specified value.
7. A dedicated person should be responsible for the maintenance and upkeep of the equipment.
8. Detailed records of each maintenance repair should be included in the factory's equipment management file.
Daily maintenance knowledge of parallel twin-screw extruder
1. After using the machine for a period of time, a comprehensive inspection should be conducted to check the tightness of all screws.
2. If there is a power interruption in production, the main drive and heating will stop. When power is restored, each section of the material barrel must be reheated to the specified temperature and kept warm for a period of time before the extruder can be started.
3. After 500 hours of use of the extruder, there will be iron filings or other impurities from gear grinding in the gearbox, so the gears should be cleaned and the gearbox lubricating oil should be replaced.
4. If the full rotation of the instrument and pointer is found, check whether the contact of the thermocouple and other lines is good.
5. No debris is allowed inside the material, and it is strictly prohibited for hard objects such as metal and sand to enter the hopper and extruder.
6. When opening the material cylinder cover or exhaust cover, take strict precautions to prevent foreign objects from falling into the main engine.
7. There should be sufficient preheating and heating time, and the manual turning should be light and agile before driving. After reaching the set process temperature, it should be kept at a constant temperature for 2 hours.
8. The screw is only allowed to start at low speed and idle for no more than 3 minutes.
Similar Product Recommend