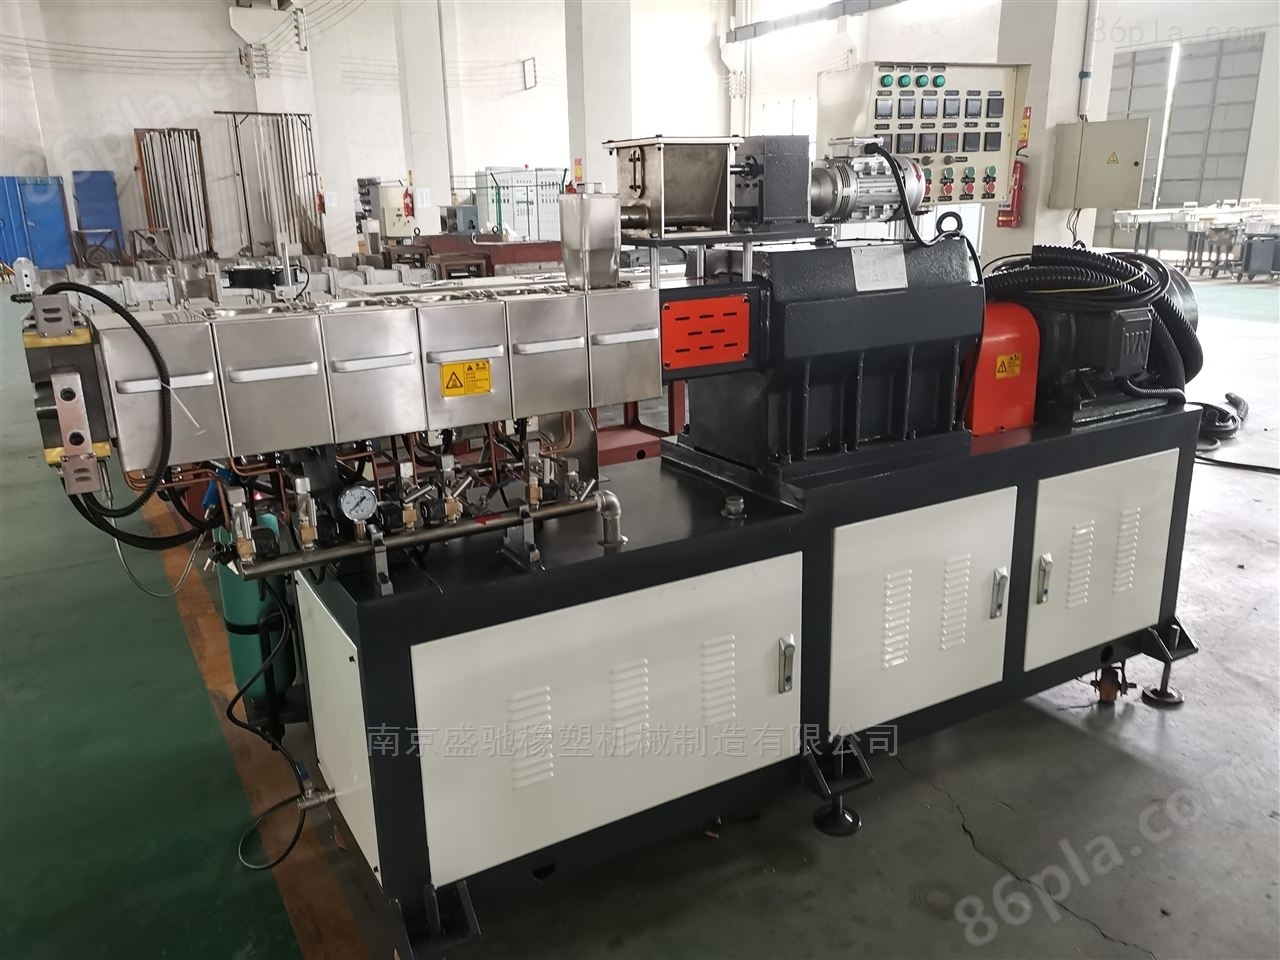
-
E-mail
geqianshun@vip.sina.com
-
Phone
18913397620,13951770588
-
Address
Chenggong Industrial Park, Lukou Town, Jiangning District, Nanjing City
Product Categories
Nanjing Shengchi Rubber Machinery Manufacturing Co., Ltd
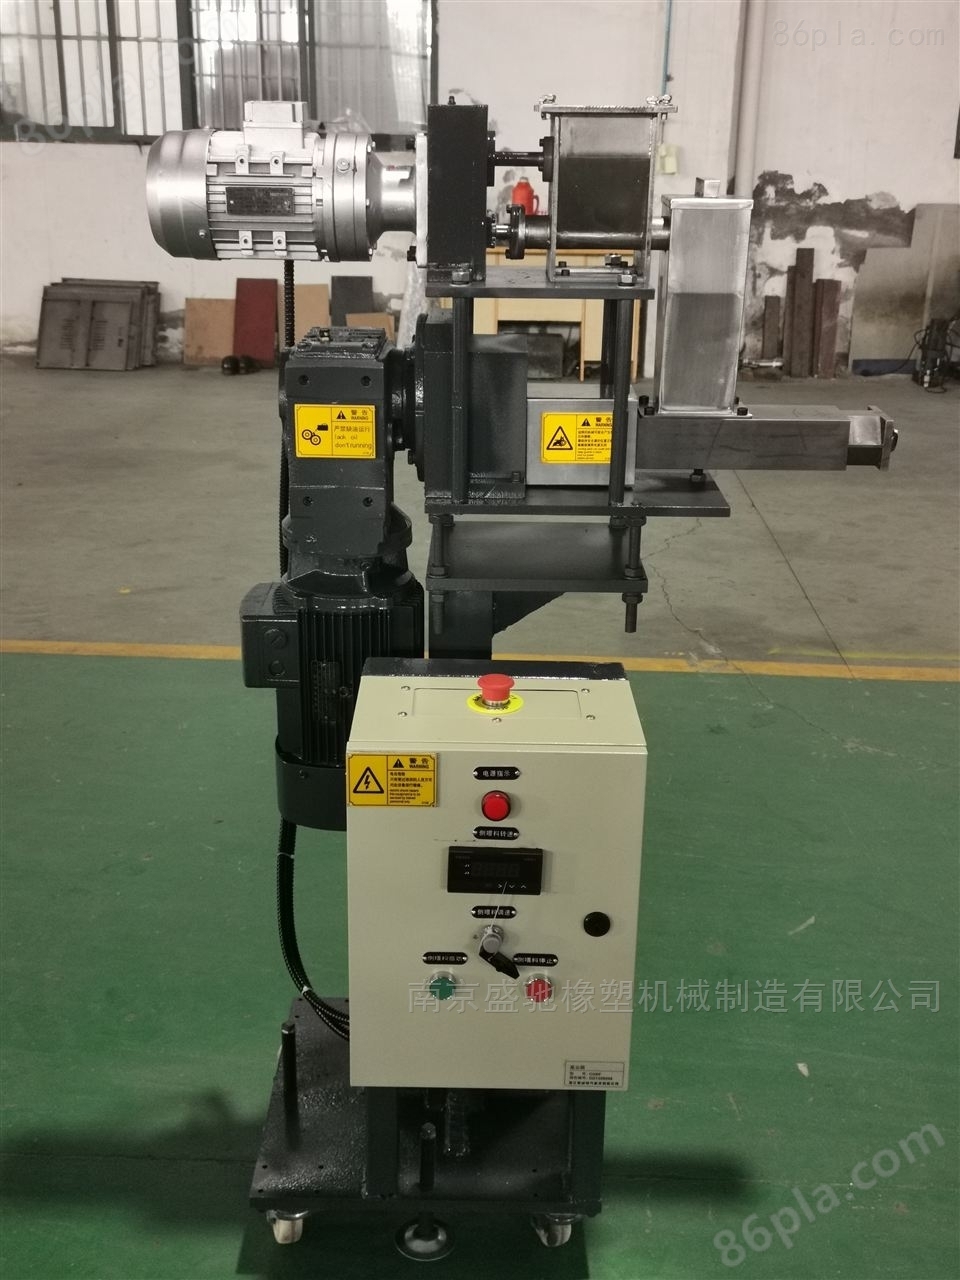
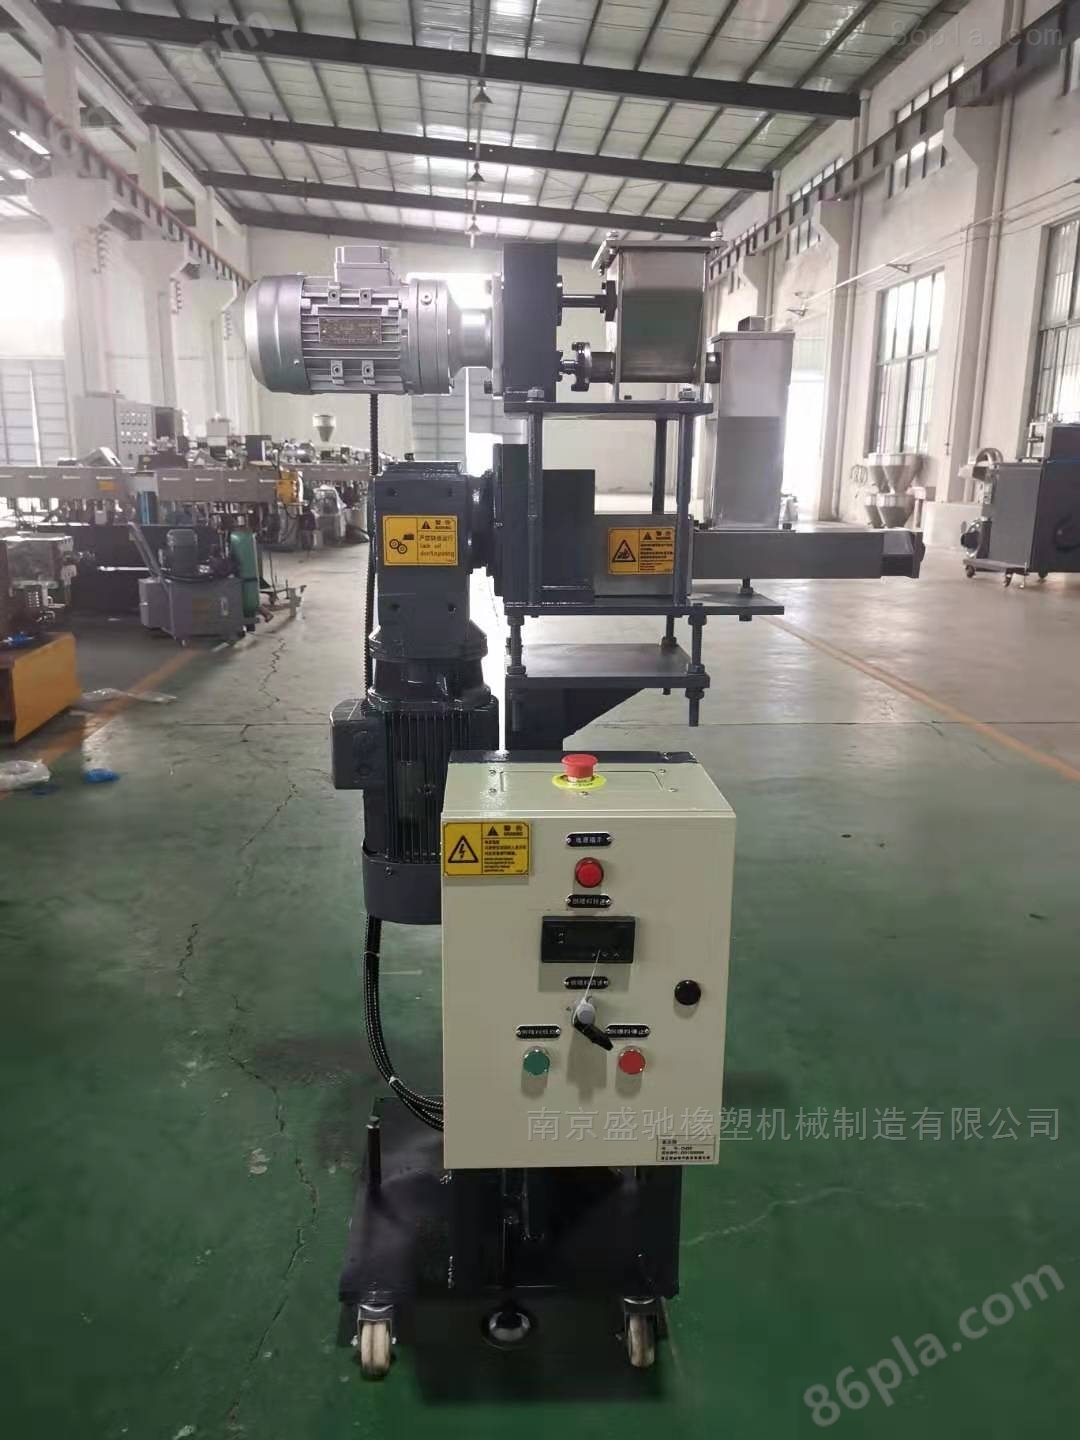
Fully automatic lateral feeding conveyor
NegotiableUpdate on 01/24
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The fully automatic lateral feeding conveyor adopts a modular design principle, with optimized screw configuration, cylinder structure, aspect ratio, feeding and extrusion, combined with German design structure. The basic screw component is a conveying component, designed with precise computer technology, and has excellent self-cleaning and interchangeable properties. With more than ten years of experience in screw configuration research and design and software technology, it can achieve advanced functions such as material conveying, pressure building extrusion, and various filling functions as needed, such as short glass fiber copolymerization, powder assisted combustion resistance, and calcium carbonate filling, with high energy efficiency. The main screw components have been collected
Product Details
Advantages of fully automatic lateral feeding conveyor:
1. The feeding body and hopper are both streamlined, ensuring smooth feeding and easy cleaning.
2. The first stage adopts a variable frequency speed regulation system for control and volume measurement. Second stage constant speed conveying.
3. Stainless steel feeding hopper with observation screen and cleaning port.
4. Feeding machine with support trolley. Removable, easy to install and maintain.
5. The motor and reducer are directly connected, and the feeding body is equipped with a horizontal mixer, ensuring smooth and even feeding without bridging.
Maintenance and upkeep of fully automatic lateral feeding conveyor:
1. When the feeder is used for batching and quantitative feeding, in order to ensure uniform and stable feeding and prevent material from flowing naturally to the horizontal equipment, if it is used for continuous feeding of general materials, the equipment can be tilted down by 10 °. For viscous materials and materials with high moisture content, the equipment can be tilted down 15 °.
1. When the feeder is used for batching and quantitative feeding, in order to ensure uniform and stable feeding and prevent material from flowing naturally to the horizontal equipment, if it is used for continuous feeding of general materials, the equipment can be tilted down by 10 °. For viscous materials and materials with high moisture content, the equipment can be tilted down 15 °.
2. The feeder behind the equipment should have a 20mm clearance for movement, and should be horizontal horizontally. Flexible connections should be used for hanging equipment.
3. Before the air test, all bolts should be consolidated once, especially the foundation bolts of the oscillating electromagnetic system. After working continuously for 3-5 hours, they should be tightened from the beginning.
4. During the test drive, the two oscillating motors must rotate in the opposite direction.
5. During the feeding process, the stability of amplitude, current, and noise should be regularly checked, and any abnormalities should be promptly stopped and dealt with.
6. Lubricating oil should be added to electromagnetic bearings every 2 months, and lubricating oil should be added once a month during high temperature seasons.
Similar Product Recommend