-
E-mail
dai_xiaozhong@163.com
-
Phone
13962468139
-
Address
Leyu Town, Zhangjiagang City
Product Categories
Suzhou Tielong Machinery Co., Ltd
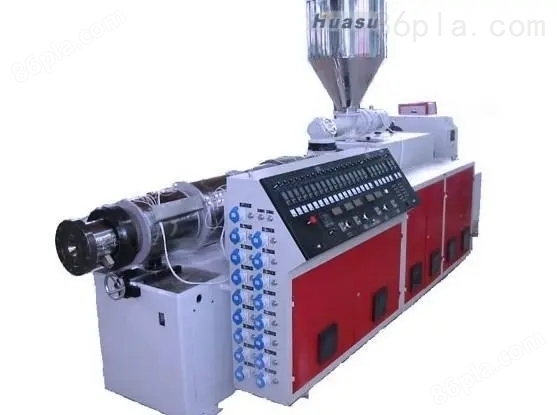
SJSZ-80 conical twin-screw plastic extruder
NegotiableUpdate on 01/12
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
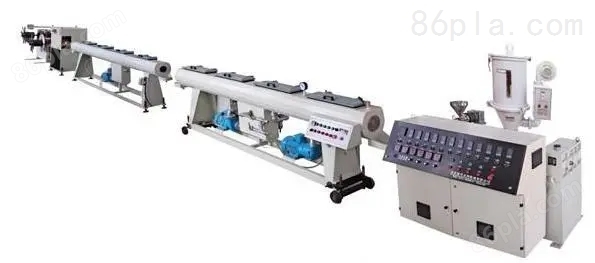
The SJSZ-80 conical twin-screw plastic extruder, equipped with appropriate head and auxiliary equipment, can directly process hard polyvinyl chloride powder into pipes, plates, profiles, etc., and can also be used for granulation of polyvinyl chloride powder.
Product Details
After being equipped with appropriate heads and auxiliary machines, the conical twin-screw plastic extruder can directly process hard polyvinyl chloride powder into pipes, plates, profiles, etc. It can also be used for granulation of polyvinyl chloride powder. Its working principle is as follows:
1. Plastic feeding: At the feeding port of the conical twin-screw extruder, plastic particles or powder are loaded into the feeding chamber.
2. Feeding and melting: When the twin-screw begins to rotate, they will push the plastic forward and apply shear force. Through continuous rotation and pushing, the plastic is gradually pushed into the narrower part of the conical chamber. During this process, the plastic is subjected to high temperature and pressure
Gradually melt into a melt with good plasticity.
3. Compression and mixing: The molten plastic is pushed towards the discharge port of the conical chamber under the action of the twin-screw. During this process, the plastic undergoes further mixing and homogenization to ensure the uniform dispersion of any additives or fillers.
4. Mold extrusion: Once the plastic is further compressed, evenly mixed, and reaches the desired state, it will be extruded through the extrusion port. Customized molds are usually used to give the extruded plastic the desired shape and size.
Operating procedures for conical twin-screw plastic extruder:
1、 Check
1. Start the main motor and blower motor, observe and check whether their rotation direction meets the requirements.
2. Pour cold water into the sink and observe whether the inlet and outlet water holes are unobstructed.
2、 Operation
1. According to the production process requirements, prepare the required materials, place the pay off reel and take-up reel, and release the cooling water. Place the traction wire properly.
2. Connect the main power supply, turn on the power switches for each heating section, and use high-speed temperature control for heating in each section.
3. Wait for the temperature gauge to indicate the specified temperature, hold for 1 hour (each heating section can be measured with a thermometer), drain the remaining material, then place the filter screen and connect the machine head.
4. When starting up, slowly adjust and observe whether the current indication is normal. After the core is aligned, thread the cable core into the machine head and start working officially.
During the process, operators must be diligent in their work. That is, "diligent observation, diligent measurement, diligent investigation".
3、 Precautions
1. Machines are generally not allowed to operate under no-load conditions to avoid scratching between the screw and the barrel.
2. The lubrication points of the machine should be regularly filled and replaced with lubricants.
3. After each production, the residual materials in the machine head and mold should be cleaned immediately. If the machine is temporarily not working, rust proof oil should be applied to the surface of the screw and mold head.
4. Strictly prevent steel impurities, small tools, and other objects from falling into the feed inlet to avoid scratching the screw and barrel.
5. Regularly check whether there is any dullness or misalignment of the instrument pointer during movement around the dial.
After the work is completed, cover the hopper lid and clean the site.
7. It is prohibited to start the machine when the temperature is below the set value.
Similar Product Recommend