
09,10,2026 9 views
With the gradual maturity of spray free materials, in mold decoration, and in mold spraying processes, the traditional manufacturing path of "injection molding followed by surface treatment" is undergoing changes.This change has already taken shape in the field of automotive exterior design.
In the past, exterior components such as front grilles, pillar trims, and rearview mirror housings often required multiple post-processing steps after injection molding, including polishing, spraying, and curing;Nowadays, some surface effects are beginning to be achieved during the molding stage.
Taking PUR (polyurethane) in mold spraying as an example: After the substrate injection molding is completed, the second PUR coating is directly injected into the surface of the plastic part. After curing, the parts taken out of the mold already have their own coating and do not need to be sprayed again. Integrating the decorative layer into the injection molding process in this way,Not only does it reduce waste in subsequent processing steps, but it also shortens the delivery cycle.

However, the change in the production path of automotive exterior is only a microcosm of industry changes.The trend of later processes being "incorporated" has quietly begun,More and more manufacturing companies are starting to consider the possibility of integrating post-processingSurface decoration, embedded integration, and multi-component assembly, as the three typical directions of the subsequent processes, are the first to become the links combined with injection molding.
Three types of post-processing steps that are included in the injection molding process
Surface decoration, embedded integration, and multi-component assembly, which used to be independent processes after injection molding, are now being vertically integrated into the injection molding processThe core of this change is not simply "one less process", but to enable more product functions to be completed in one molding process, thereby reducing subsequent sequence switching, assembly, and repetitive processing.
When the objects delivered in the injection molding process extend from single molded parts to higher completion parts or even finished products, the demand for injection molding machines naturally changes. The requirements of "playing fast," "playing steadily," and "playing well" still apply, but on this basis,'One machine with multiple capabilities' has also begun to be included in the demand list.
fromSingle machine to integrated solutionZhenxiong's answer
As the subsequent processes are continuously integrated and integrated, what customers need is no longer just a stable injection molding machine, but a set of capabilities that can enable the entire product to be molded in one go. And this is exactly what Zhenxiong has been doing——Not limiting oneself to the role of equipment suppliers, but integrating equipment, processes, and automation capabilities around the goal of "finished product delivery".
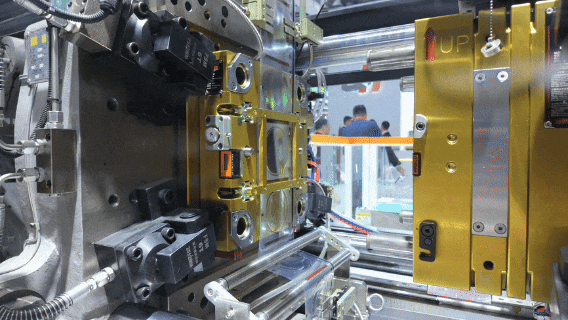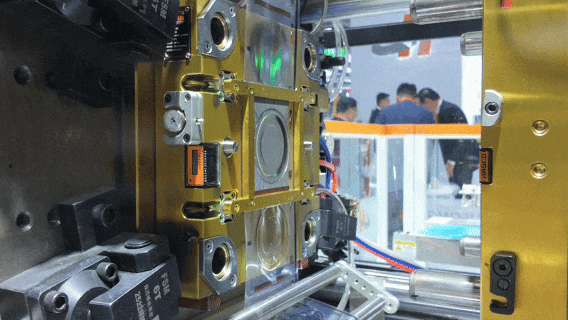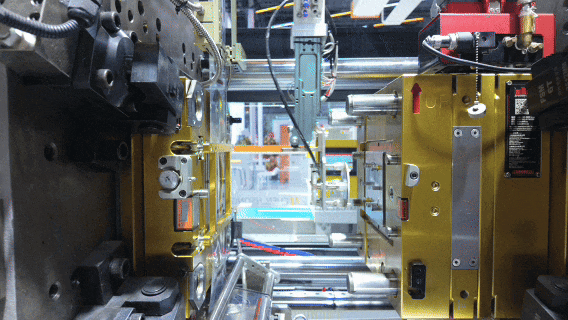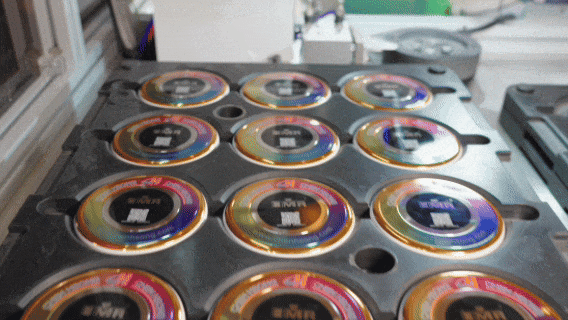
The transfer window of IMR technology is short, and the transfer of the pattern from the film to the surface of the plastic part occurs within a few seconds before mold opening. Injection molding, holding pressure, and carrier peeling are almost completed simultaneously. This requires the device to achieve millisecond level accuracy in controlling injection pressure and clamping force. Any small displacement or pressure fluctuation can directly cause pattern ghosting, edge blurring, or even transfer failure. In addition, the decorative layer of IMR will be directly exposed to the surface of the product after transfer printing, and the cleanliness of the molding environment is equally important.
Zhenxiong SPARK AE fully electric injection molding machine x IMR

production process
Product Information
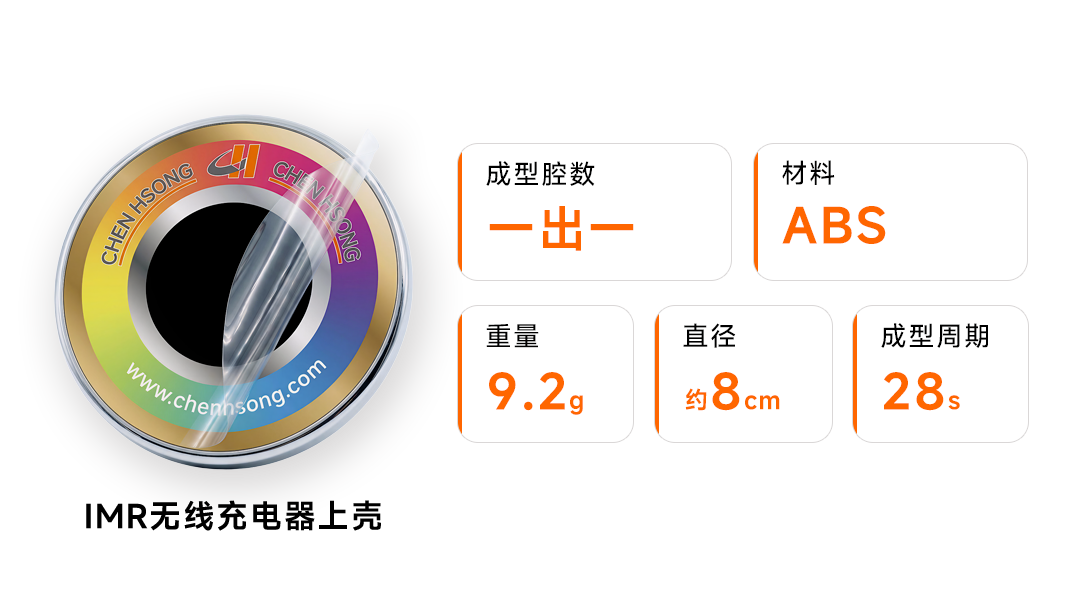
Highlights of the Solution
1. The repeated precision of equipment glue injection is stable within ± 0.01mmEnsure that the physical form of the carrier film remains constant at the moment of compression, effectively avoiding the scrap rate caused by film displacement;
2. Millisecond level pressure responseBased on the pressure feedback of the film, the real-time correction curve is used to minimize pressure fluctuations during the transfer printing process, ensuring clear edges of the pattern;
3. 震雄SPARK AEFully electric configurationTo eliminate the possibility of hydraulic oil mist pollution and ensure that the transfer surface is flawless.
PART 02
IML process plan
Surface decoration moved forward
Surface decoration moved forward
IML for membrane positioningmoldThere are high requirements for design, automation coordination, injection and temperature control stability. Injection molding equipment needs to be equipped with an automated film feeding system andManipulatorHelp the film to complete decoration and molding inside the mold, reducing subsequent decorative processes such as spraying and screen printing. Whether the membrane positioning is accurate, whether the injection speed curve is stable, whether the pressure switching is timely, and whether the mold temperature is uniform, all affect the final appearance of the product.
Zhenxiong SPARK MS electric injection molding machine x IML
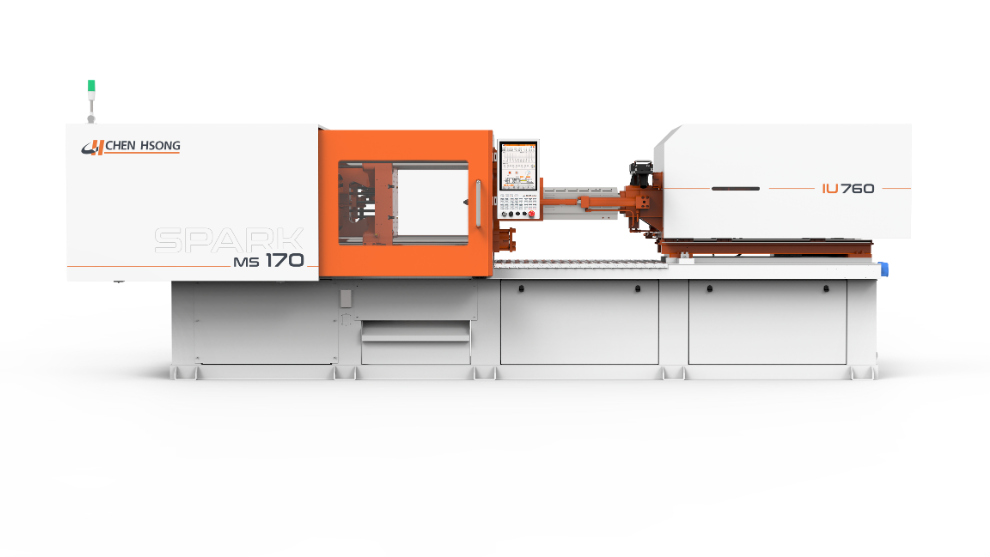
production process

Product Information

Highlights of the Solution
1. The equipment covers a clamping force of 90 to 1700 tonsThe large template design is adapted to the increased mold opening stroke and film feeding space required by IML, covering production needs from small parts to large exterior parts;
2. The precision of repeated positioning is controlled at the level of ± 0.01mmMake every action stay in its proper position;
3. Standard 160mm/s high-speed stable injectionAllow the melt to fill smoothly and avoid bursting the membrane;
4. iChen ™ AI Molder intelligent parameter tuning controlAutomatically adjust and optimize molding parameters to reduce variable interference during manual mold testing.
PART 03
Embedded molding scheme
Assembly forward
Embedded molding scheme
Assembly forward
The difficulty of integrated molding lies in the balance between strength, accuracy, and efficiency. Metal inserts, electronic components, wiring harnesses, and sealing structures, which are often covered with precision and fragility, can cause small deviations during mold closing, momentary impacts during molding, and fluctuations in pressure output, all of which can lead to embedded displacement, coil breakage, and inadequate covering.
Zhenxiong H series vertical molding machine x insert molding
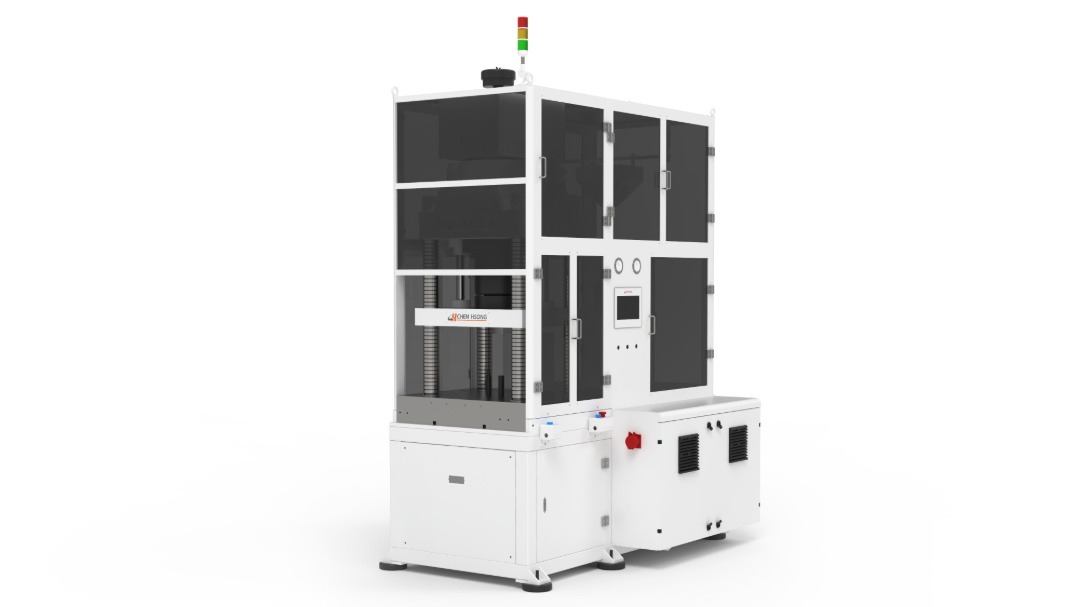
production process

Product Information

Highlights of the Solution
1. High rigidity body, small mold clearance, and excellent anti eccentric load capabilityEnsure that the slider remains vertical during high-speed motion to avoid dimensional deviations caused by tilting;
2. Micro scale closed-loop controlEven under rapid molding, it can still accurately encapsulate micro coils, effectively preventing wire breakage and eccentricity, ensuring a utilization rate of over 99.6% for the solution;
3. Efficient integrated moldingSome structures that originally required subsequent welding, riveting, or bonding can be moved forward into the mold for one-time molding.
PART 04
In mold assembly plan
Multi component assembly moving forward
For multi-component products, manufacturing complexity often comes not only from the molding of individual parts, but also from subsequent assembly. After the number of components increases, the assembly stations, turnover times, and positioning coordination will also increase, and size and position errors may accumulate in multiple processes.
Zhenxiong SPARK EH electric injection molding machine x in mold assembly

production process

Product Information

Highlights of the Solution
1. Flexible combination of multiple shooting stationsOne time molding of multi-color and multi material products significantly improves production efficiency and batch consistency;
2. Through the coordination of the turntable mold and the shaft mechanism, injection molding can be completedComplete product assembly directly inside the mold, and the finished product is produced after demoldingNo additional assembly station is required.
The 'subtraction' of the subsequent process is not the disappearance of the process, but the rewriting of the manufacturing logic. As more and more post-processing is integrated into the molding stage, the value of injection molding equipment extends from a single molding capability to process integration, automation collaboration, and higher completion delivery.And Zhenxiong is also continuously expanding the capability boundaries of injection molding equipment and integrated molding solutions around this change.
This article is reproduced from a third-party platform for the purpose of promoting information exchange and has no profit-making purpose. The views expressed in this article are not related to the position of this website, and unverified information is for reference only and is not used as any investment or trading basis. If you have no intention of infringing on media or personal intellectual property rights, please call or write to us, and our website will handle it as soon as possible.
This article is reproduced from a third-party platform for the purpose of promoting information exchange and has no profit-making purpose. The views expressed in this article are not related to the position of this website, and unverified information is for reference only and is not used as any investment or trading basis. If you have no intention of infringing on media or personal intellectual property rights, please call or write to us, and our website will handle it as soon as possible.