-
E-mail
564481047@qq.com
-
Phone
13706223809
-
Address
Intersection of New Wukesong Road and New 204 National Highway in Leyu Town, Zhangjiagang City, Suzhou City, Jiangsu Province
Product Categories
Zhangjiagang Huade Machinery Technology Co., Ltd
Industrial PVC power pipe extrusion production line
NegotiableUpdate on 01/17
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
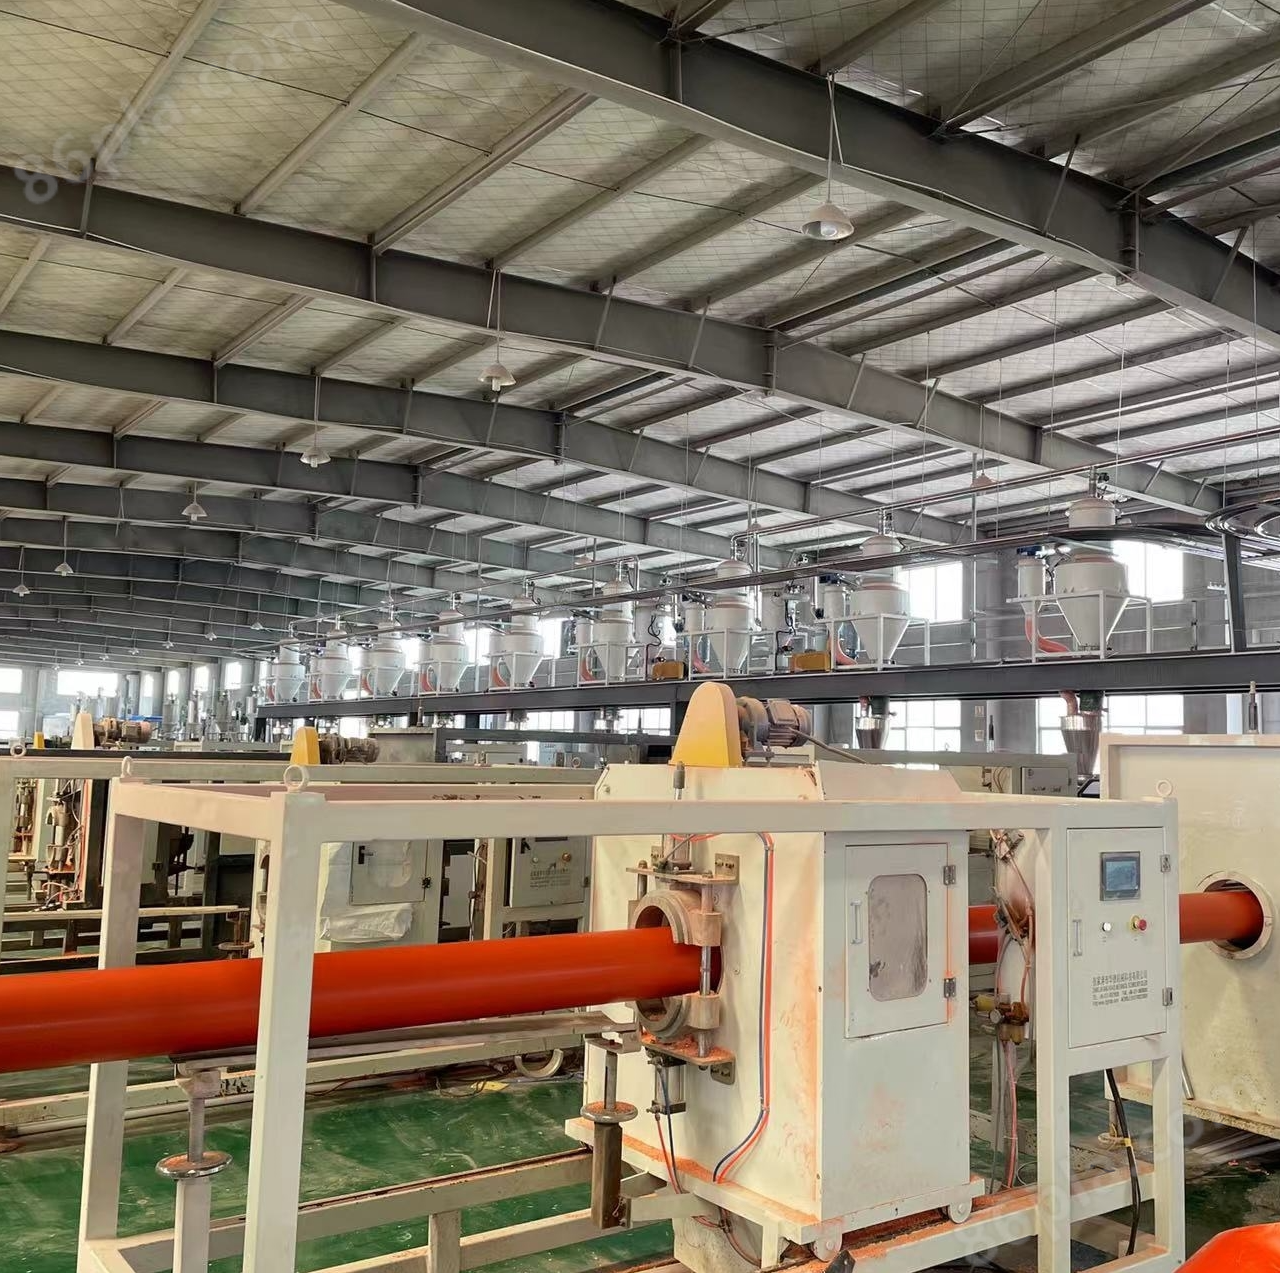
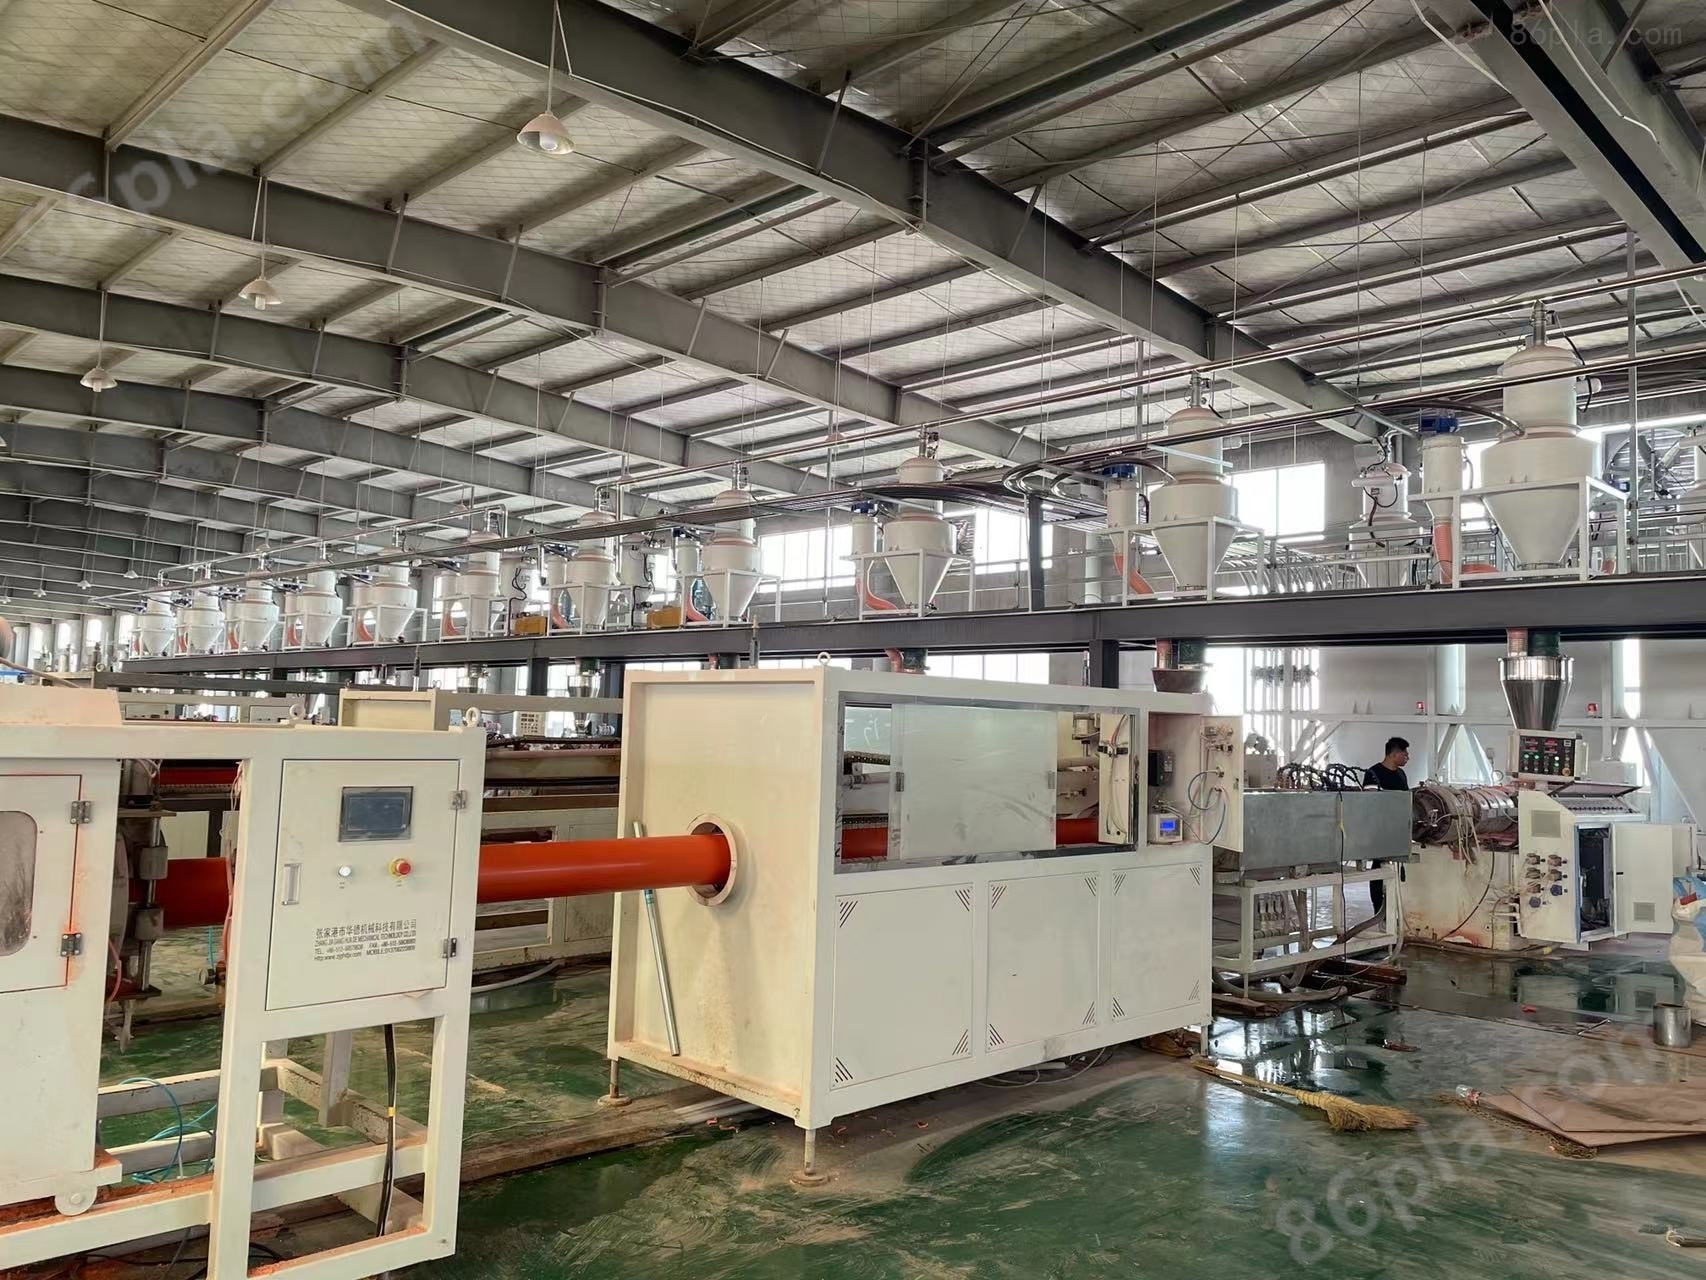
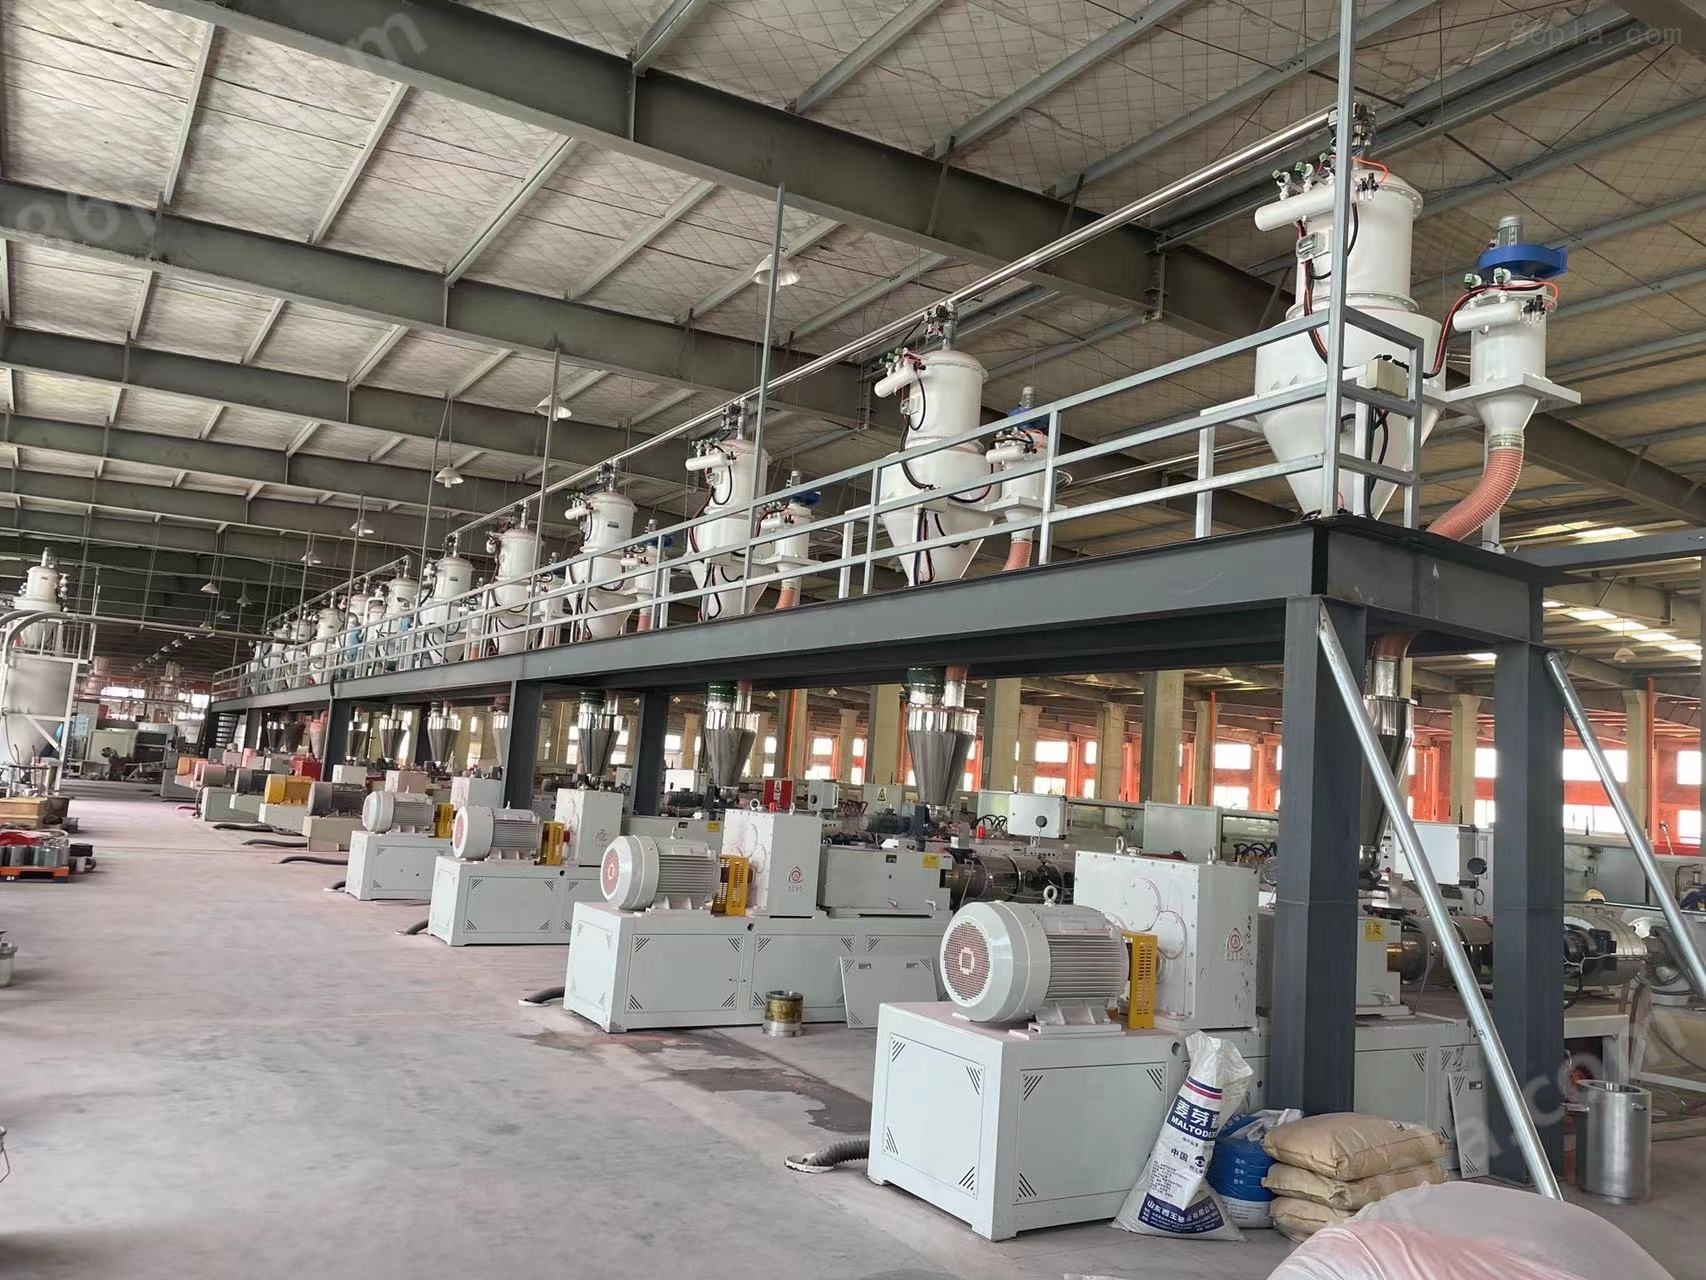
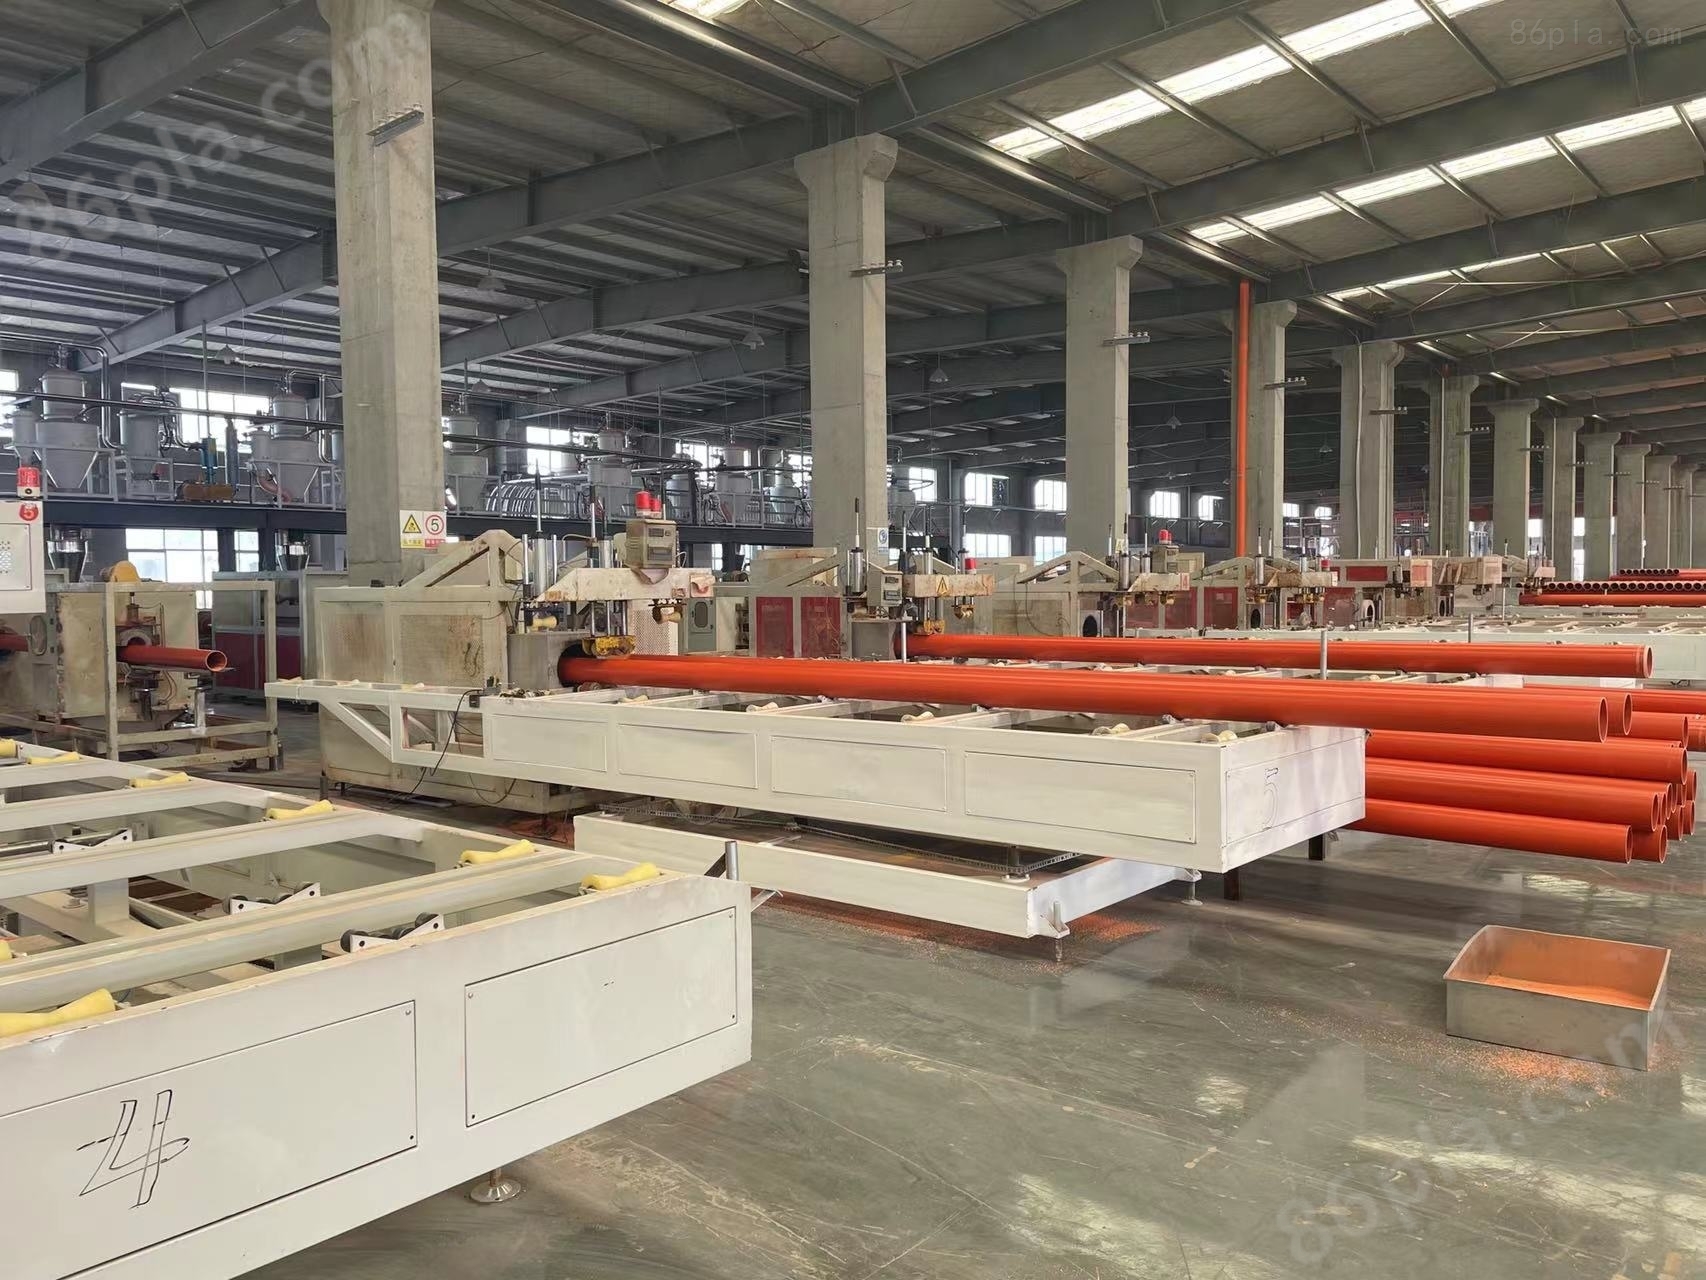
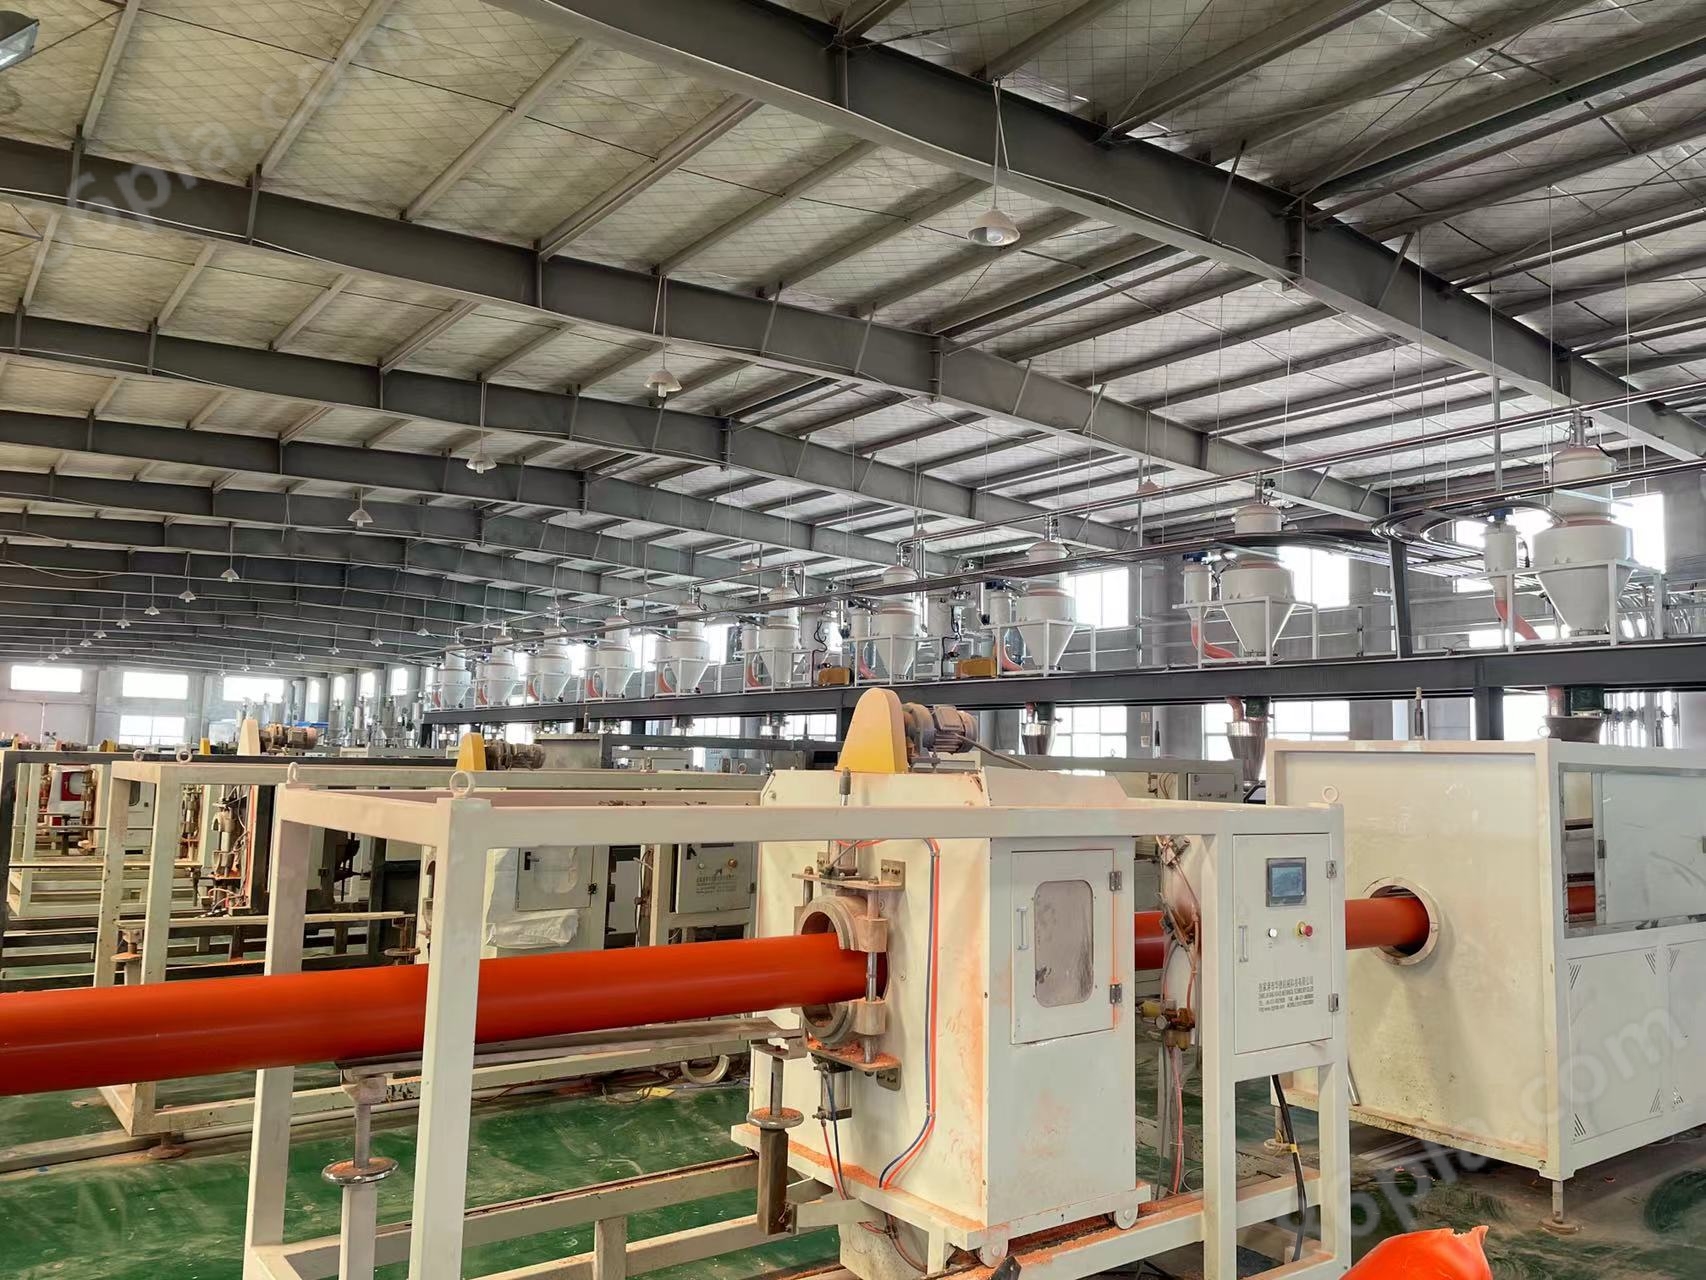
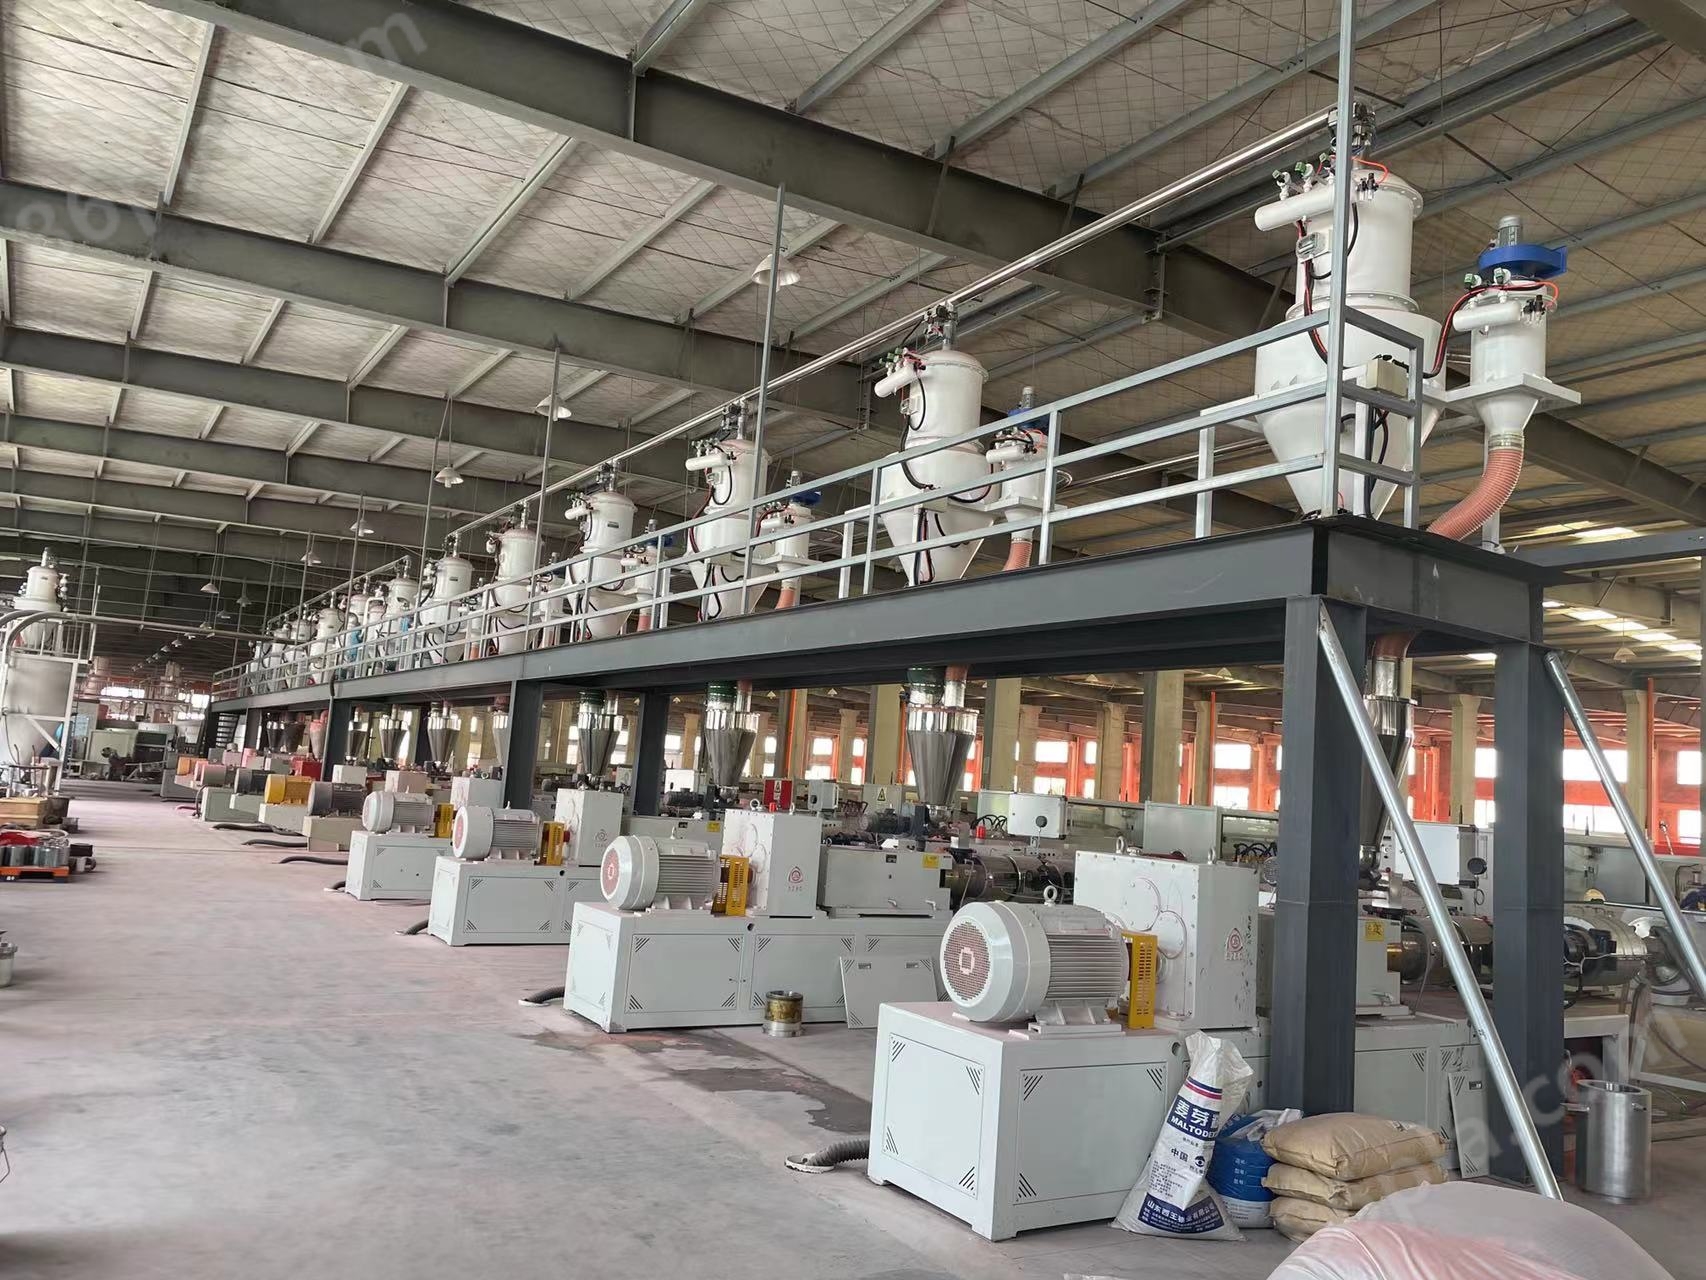
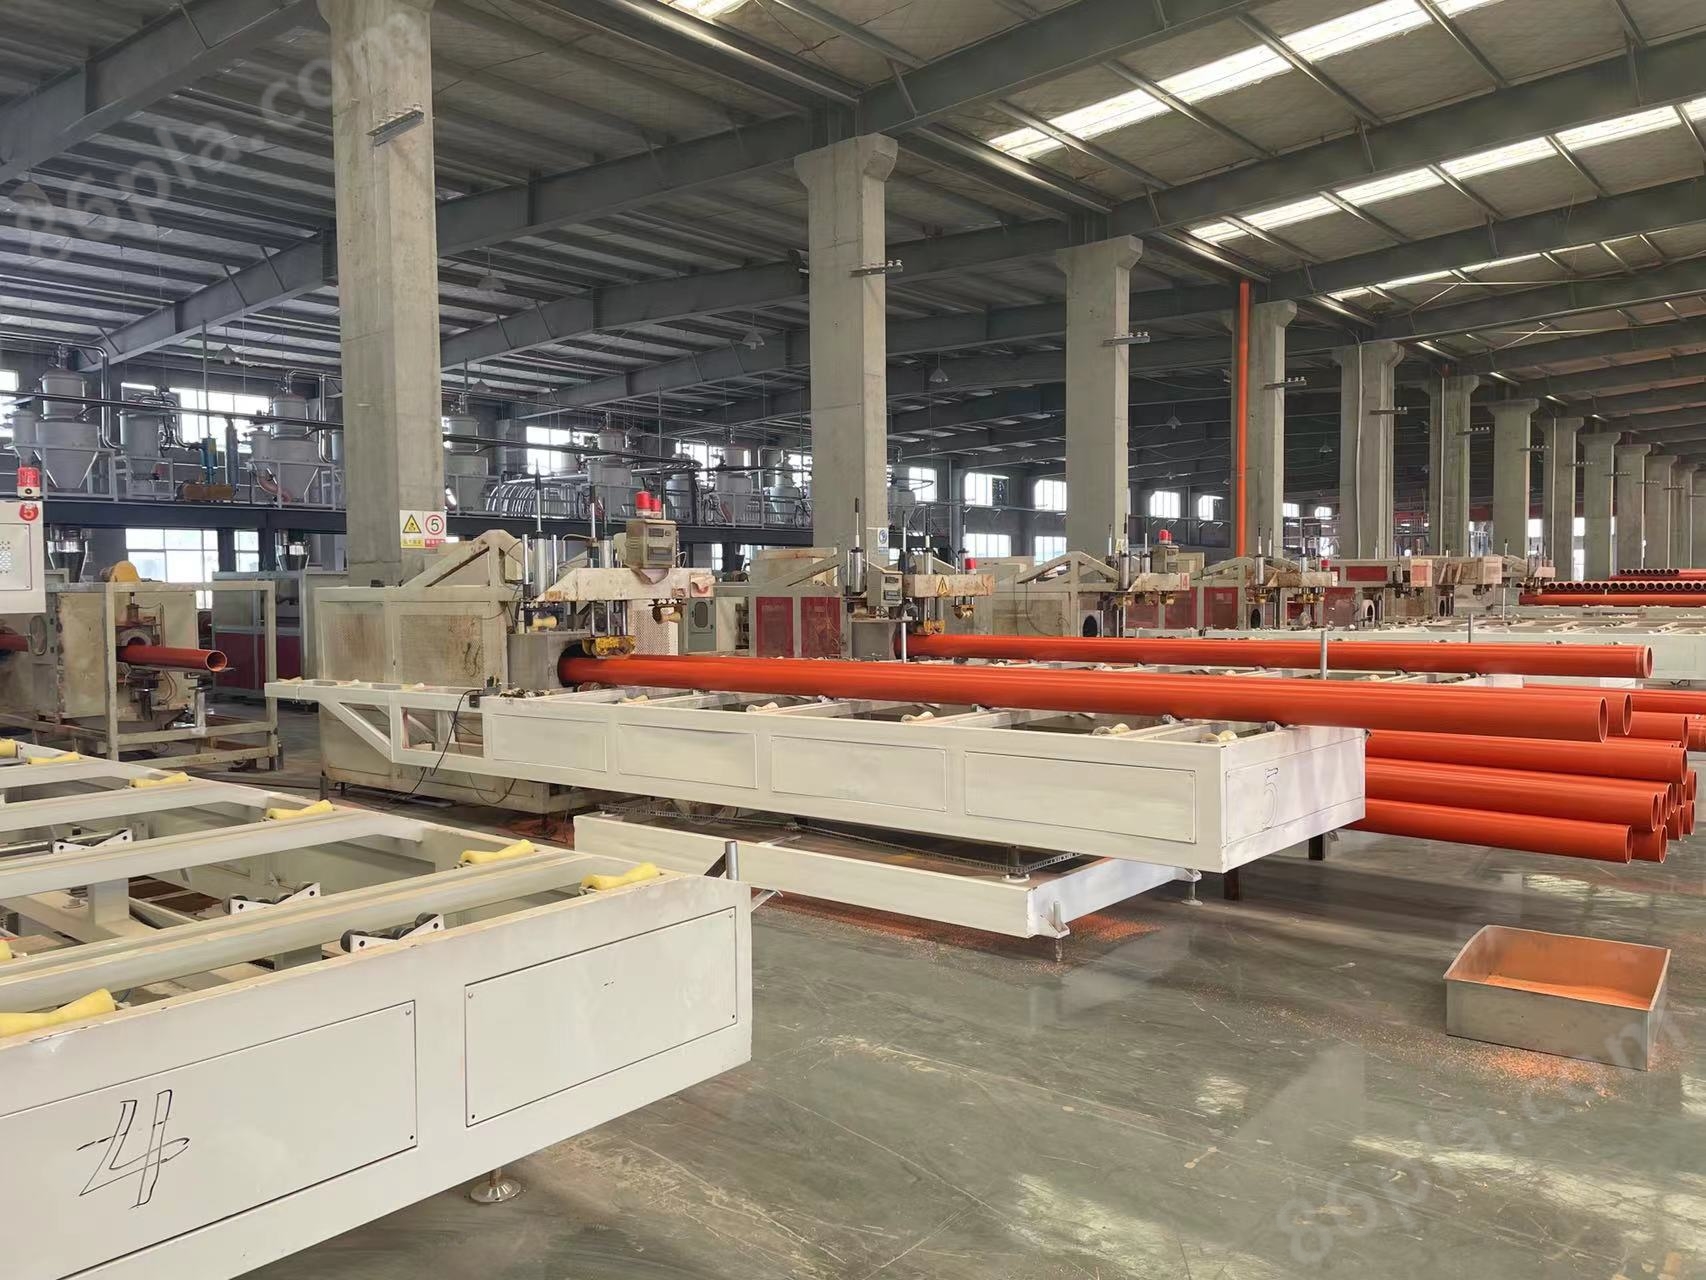
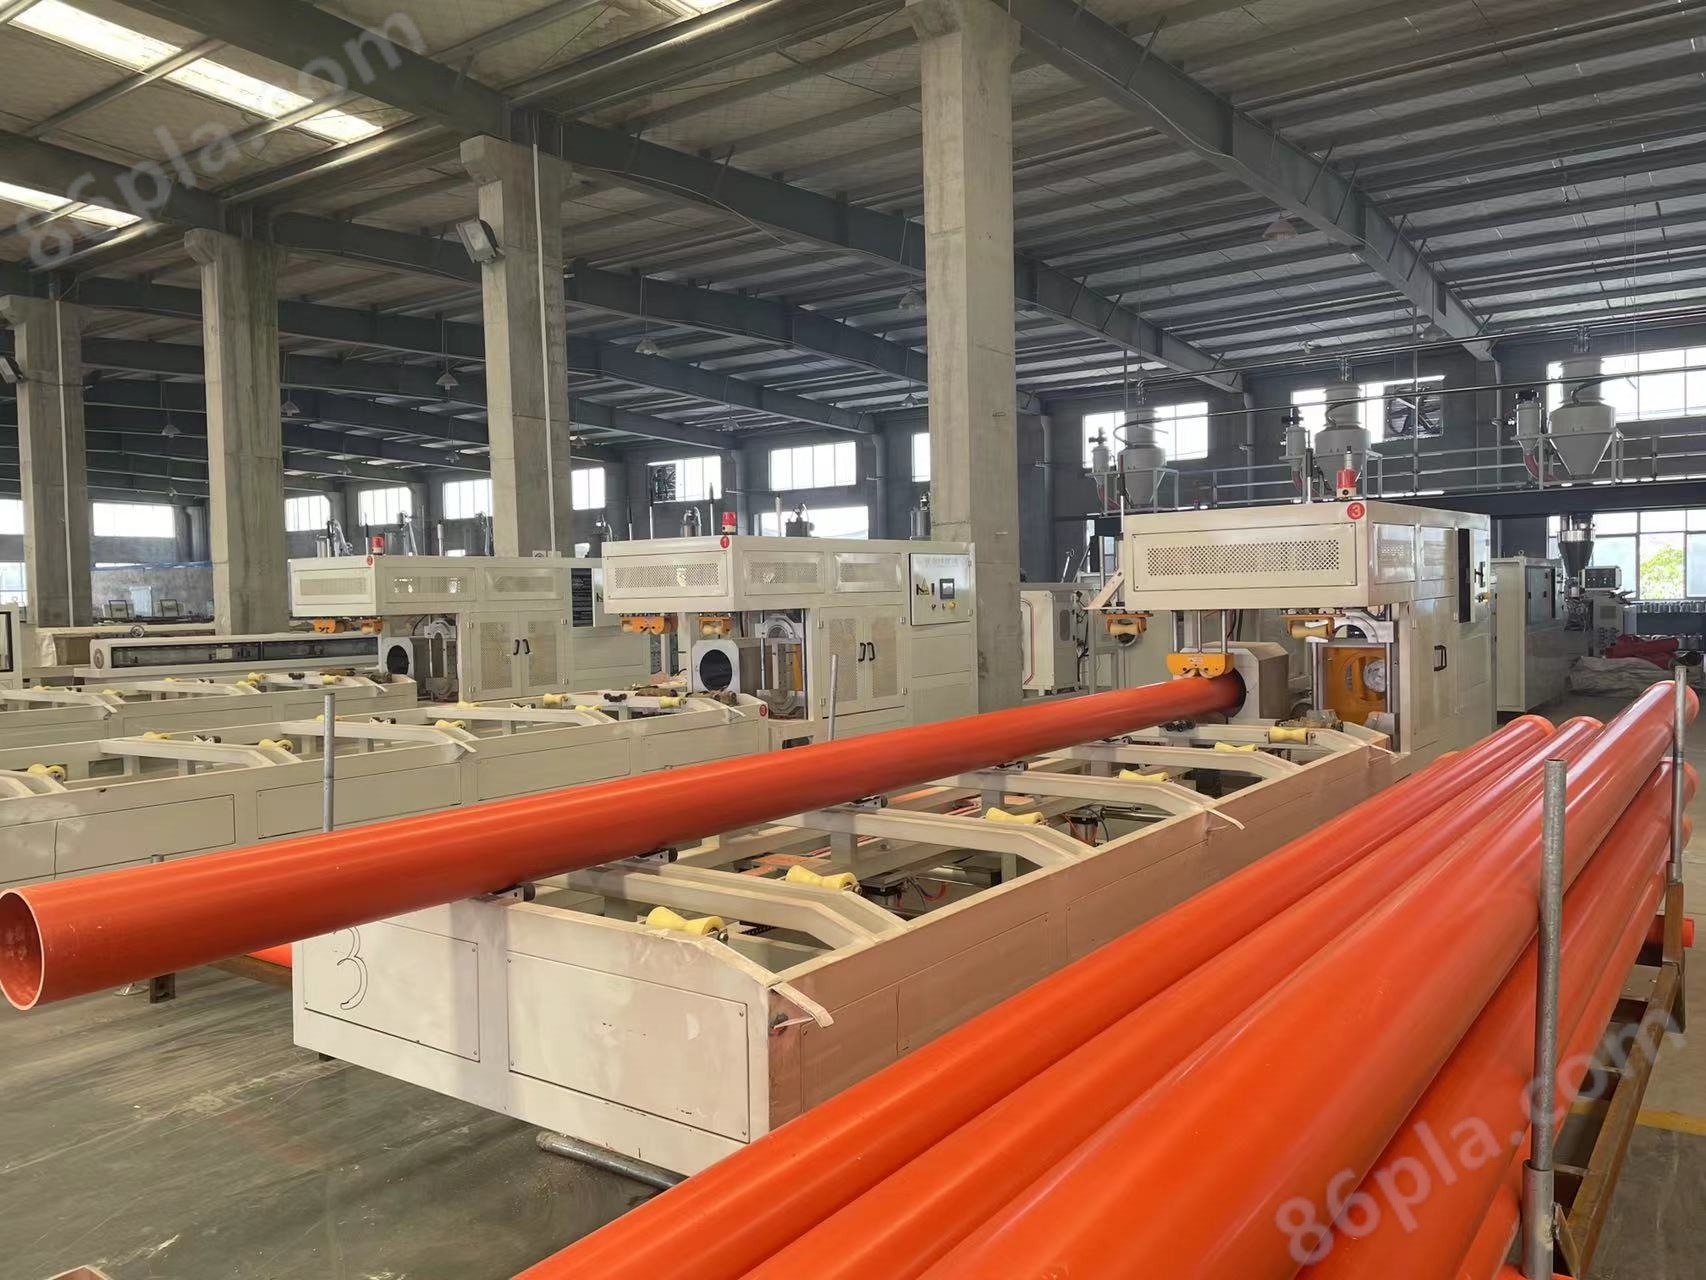
The industrial PVC power pipe extrusion production line is mainly used for producing plastic PVC pipes with various diameters and wall thicknesses in agricultural water supply and drainage, building water supply and drainage, power cable and other fields.
Product Details
Industrial PVC power pipe extrusion production lineIntroduction
There are two claw, three claw, four claw, six claw, eight claw and other traction methods for tractors.
It can be cut with a saw blade or planetary cutting method, and equipped with a meter counter and thickening device.
The planetary cutting machine adopts fully automatic computer numerical control, which has the advantages of easy operation and reliable performance, reaching the international level.
The unit has reliable performance and high production efficiency. Our company can provide different configurations according to customer requirements. Our company provides formula technology and other support.
Industrial PVC power pipe extrusion production lineDaily maintenance and upkeep:
1. It is necessary to regularly check whether the pipelines of plastic pipe equipment are leaking and whether the fasteners are tightened during long-term operation. The plastic pipe production equipment consists of a control system, extruder, machine head, shaping cooling system, traction machine, cutting device, winding machine, and flipping rack.
2. Regularly check whether the safety device of the machine is effective, especially after replacing the mold, check whether the mechanical safety has been adjusted accordingly. This plays a crucial role in ensuring the safe operation of all production lines.
3. Regularly check the condition of the oil filter screen or packing, replace it in a timely manner, and pay attention to whether the oil quality is contaminated or deteriorated. As an important component of chemical building materials, plastic pipe production lines are widely accepted by users for their excellent performance, hygiene, environmental protection, and low consumption. They mainly include polyethylene water supply pipes, polypropylene pipes, floor heating pipes, composite pipes, etc. When the hydraulic oil turns black brown and emits a foul odor, it indicates oxidation and deterioration. The hydraulic oil should be updated as soon as possible. When there are small freckles or translucent spots in the hydraulic oil, it indicates impurities or metal powder mixed in and should be filtered or replaced.
4. During the running process, it is best to perform several maintenance and repairs, lubrication, adjustment, physical examination, etc. on the pipe equipment. The plastic pipe production equipment consists of a control system, extruder, machine head, shaping cooling system, traction machine, cutting device, winding machine, and flipping rack. Proper maintenance and upkeep are essential to ensure the normal operation of the production line.
Notes:
1. Temperature control
Temperature control is an important control factor in extrusion operations. The temperature control factors required for extrusion molding are barrel temperature, diameter temperature, and die temperature. Low temperature, poor plasticization, dull appearance of pipes, poor mechanical properties, and product quality not meeting requirements: high temperature can cause material decomposition, product discoloration, and other phenomena.
2. Screw speed
By increasing the screw speed, the extrusion amount can be increased, which can increase the yield. However, it is easy to cause poor plasticization, resulting in rough inner walls of the pipe and a decrease in strength. At this time, the head pressure should be adjusted to achieve the desired yield and quality. The temperature control of the screw affects the material conveying rate, plasticization, and melting quality of the material. Squeezing pipes requires cooling water to reduce the temperature of the screw, which is beneficial for improving plasticization quality. The temperature of the screw cooling water should be around 50-70 degrees Celsius.
3. Traction speed
The adjustment of traction speed is very important in the re extrusion operation. After the material is extruded, melted and plasticized, it is continuously extruded from the machine head and then pulled into the shaping device, cooling device, traction device, etc. The traction speed should match the extrusion speed. In normal production, the traction speed should be about 1% to 10% faster than the extrusion speed of the pipe.
4. Compressed air and pressure
Compressed air can inflate pipes and maintain a certain degree of roundness. The pressure should be of appropriate magnitude. The pressure is too low, the pipe is not round, the pressure is too high, the core mold is cooled, cracks appear on the inner wall of the pipe, it is not smooth, and the quality of the pipe decreases. At the same time, stable pressure is required. If the pressure fluctuates, the pipe material is prone to bamboo knots.
5. Temperature of sizing device and cooling device
Squeezing different plastic products, using different sizing and cooling methods, the cooling medium can be air, water, or other liquids, and temperature needs to be controlled, which is mainly related to production efficiency, internal stress of the product, etc.

Similar Product Recommend


