-
E-mail
564481047@qq.com
-
Phone
13706223809
-
Address
Intersection of New Wukesong Road and New 204 National Highway in Leyu Town, Zhangjiagang City, Suzhou City, Jiangsu Province
Product Categories
Zhangjiagang Huade Machinery Technology Co., Ltd
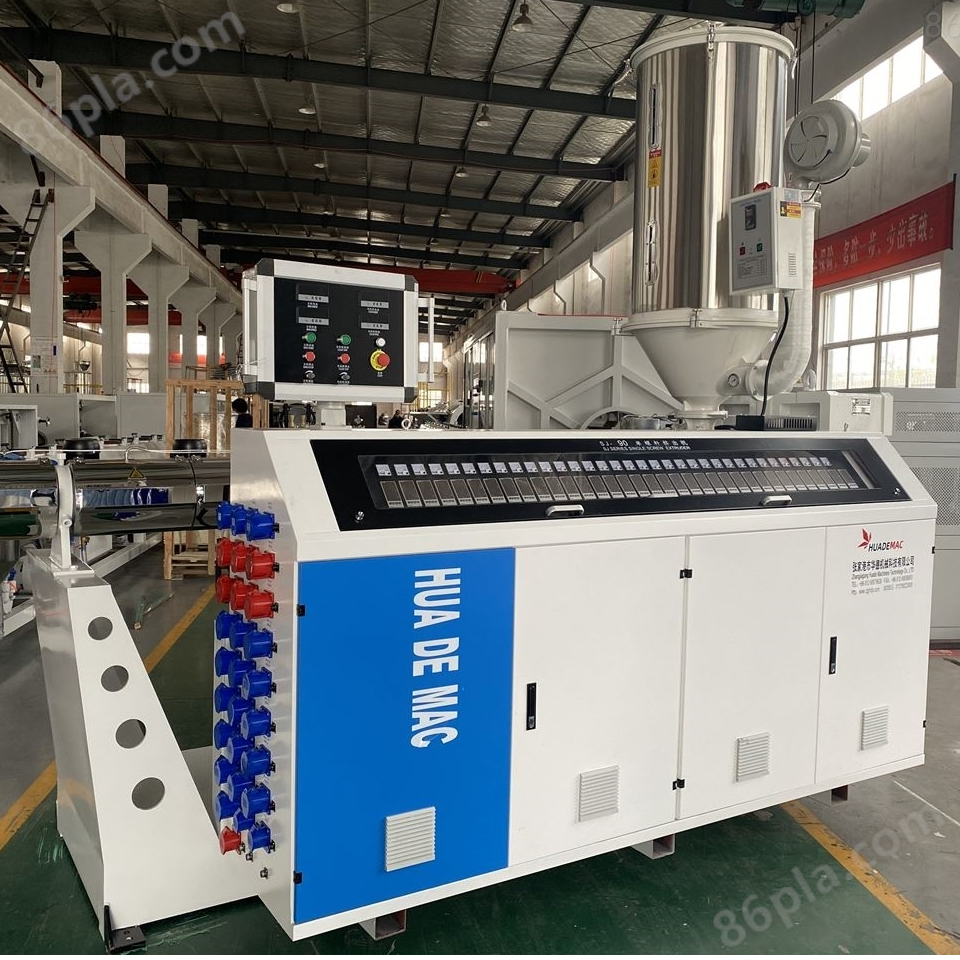
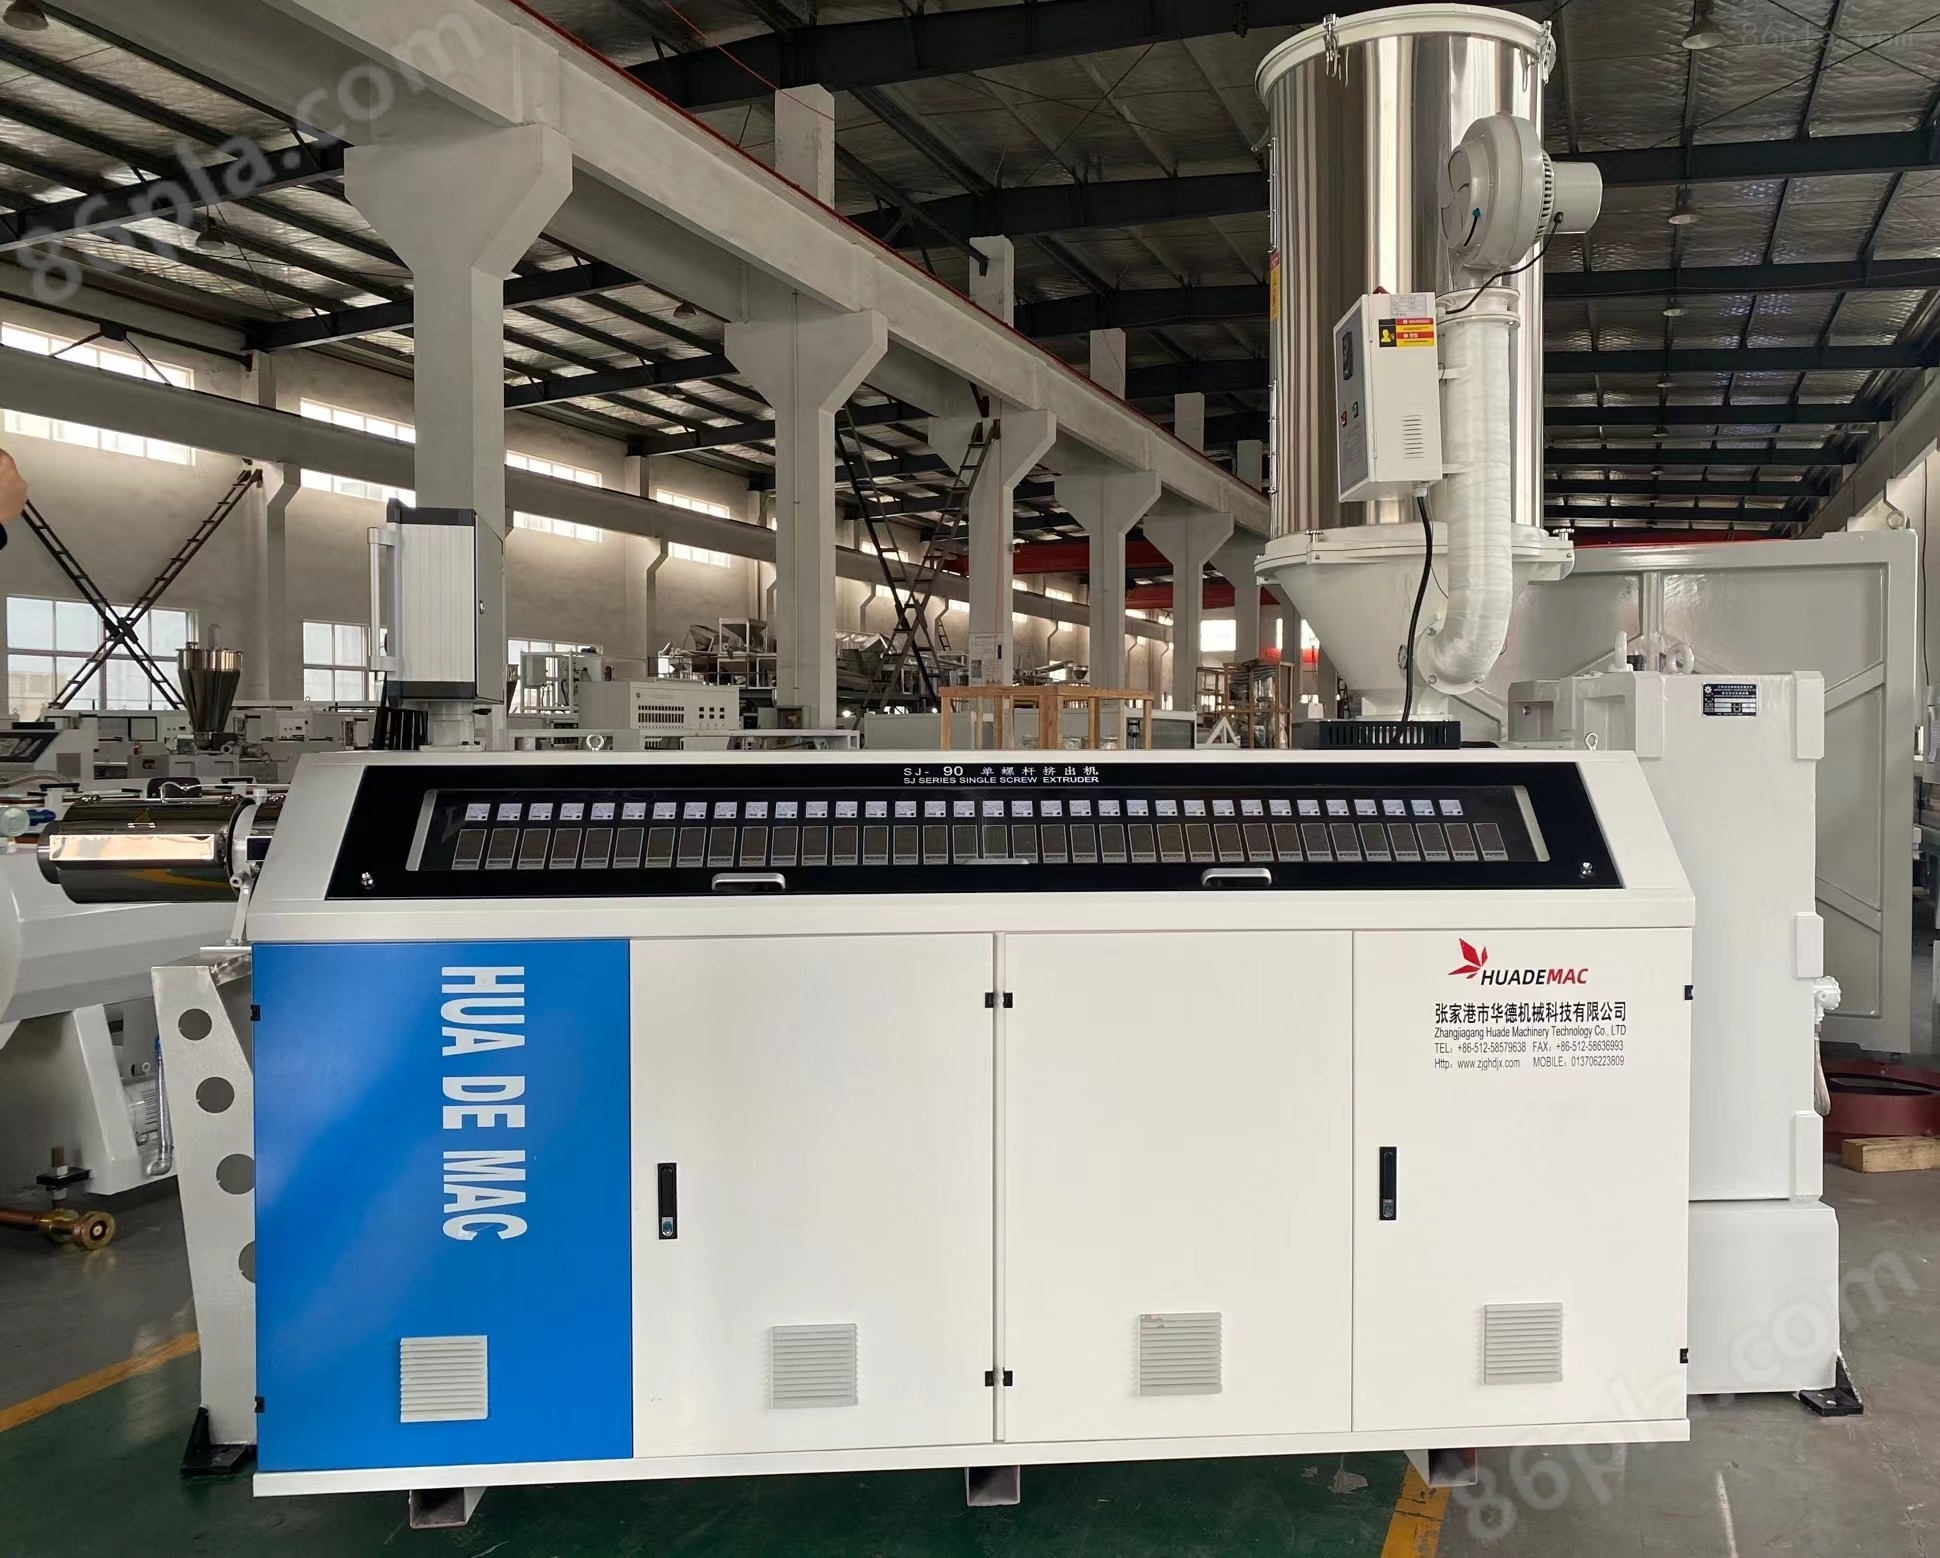
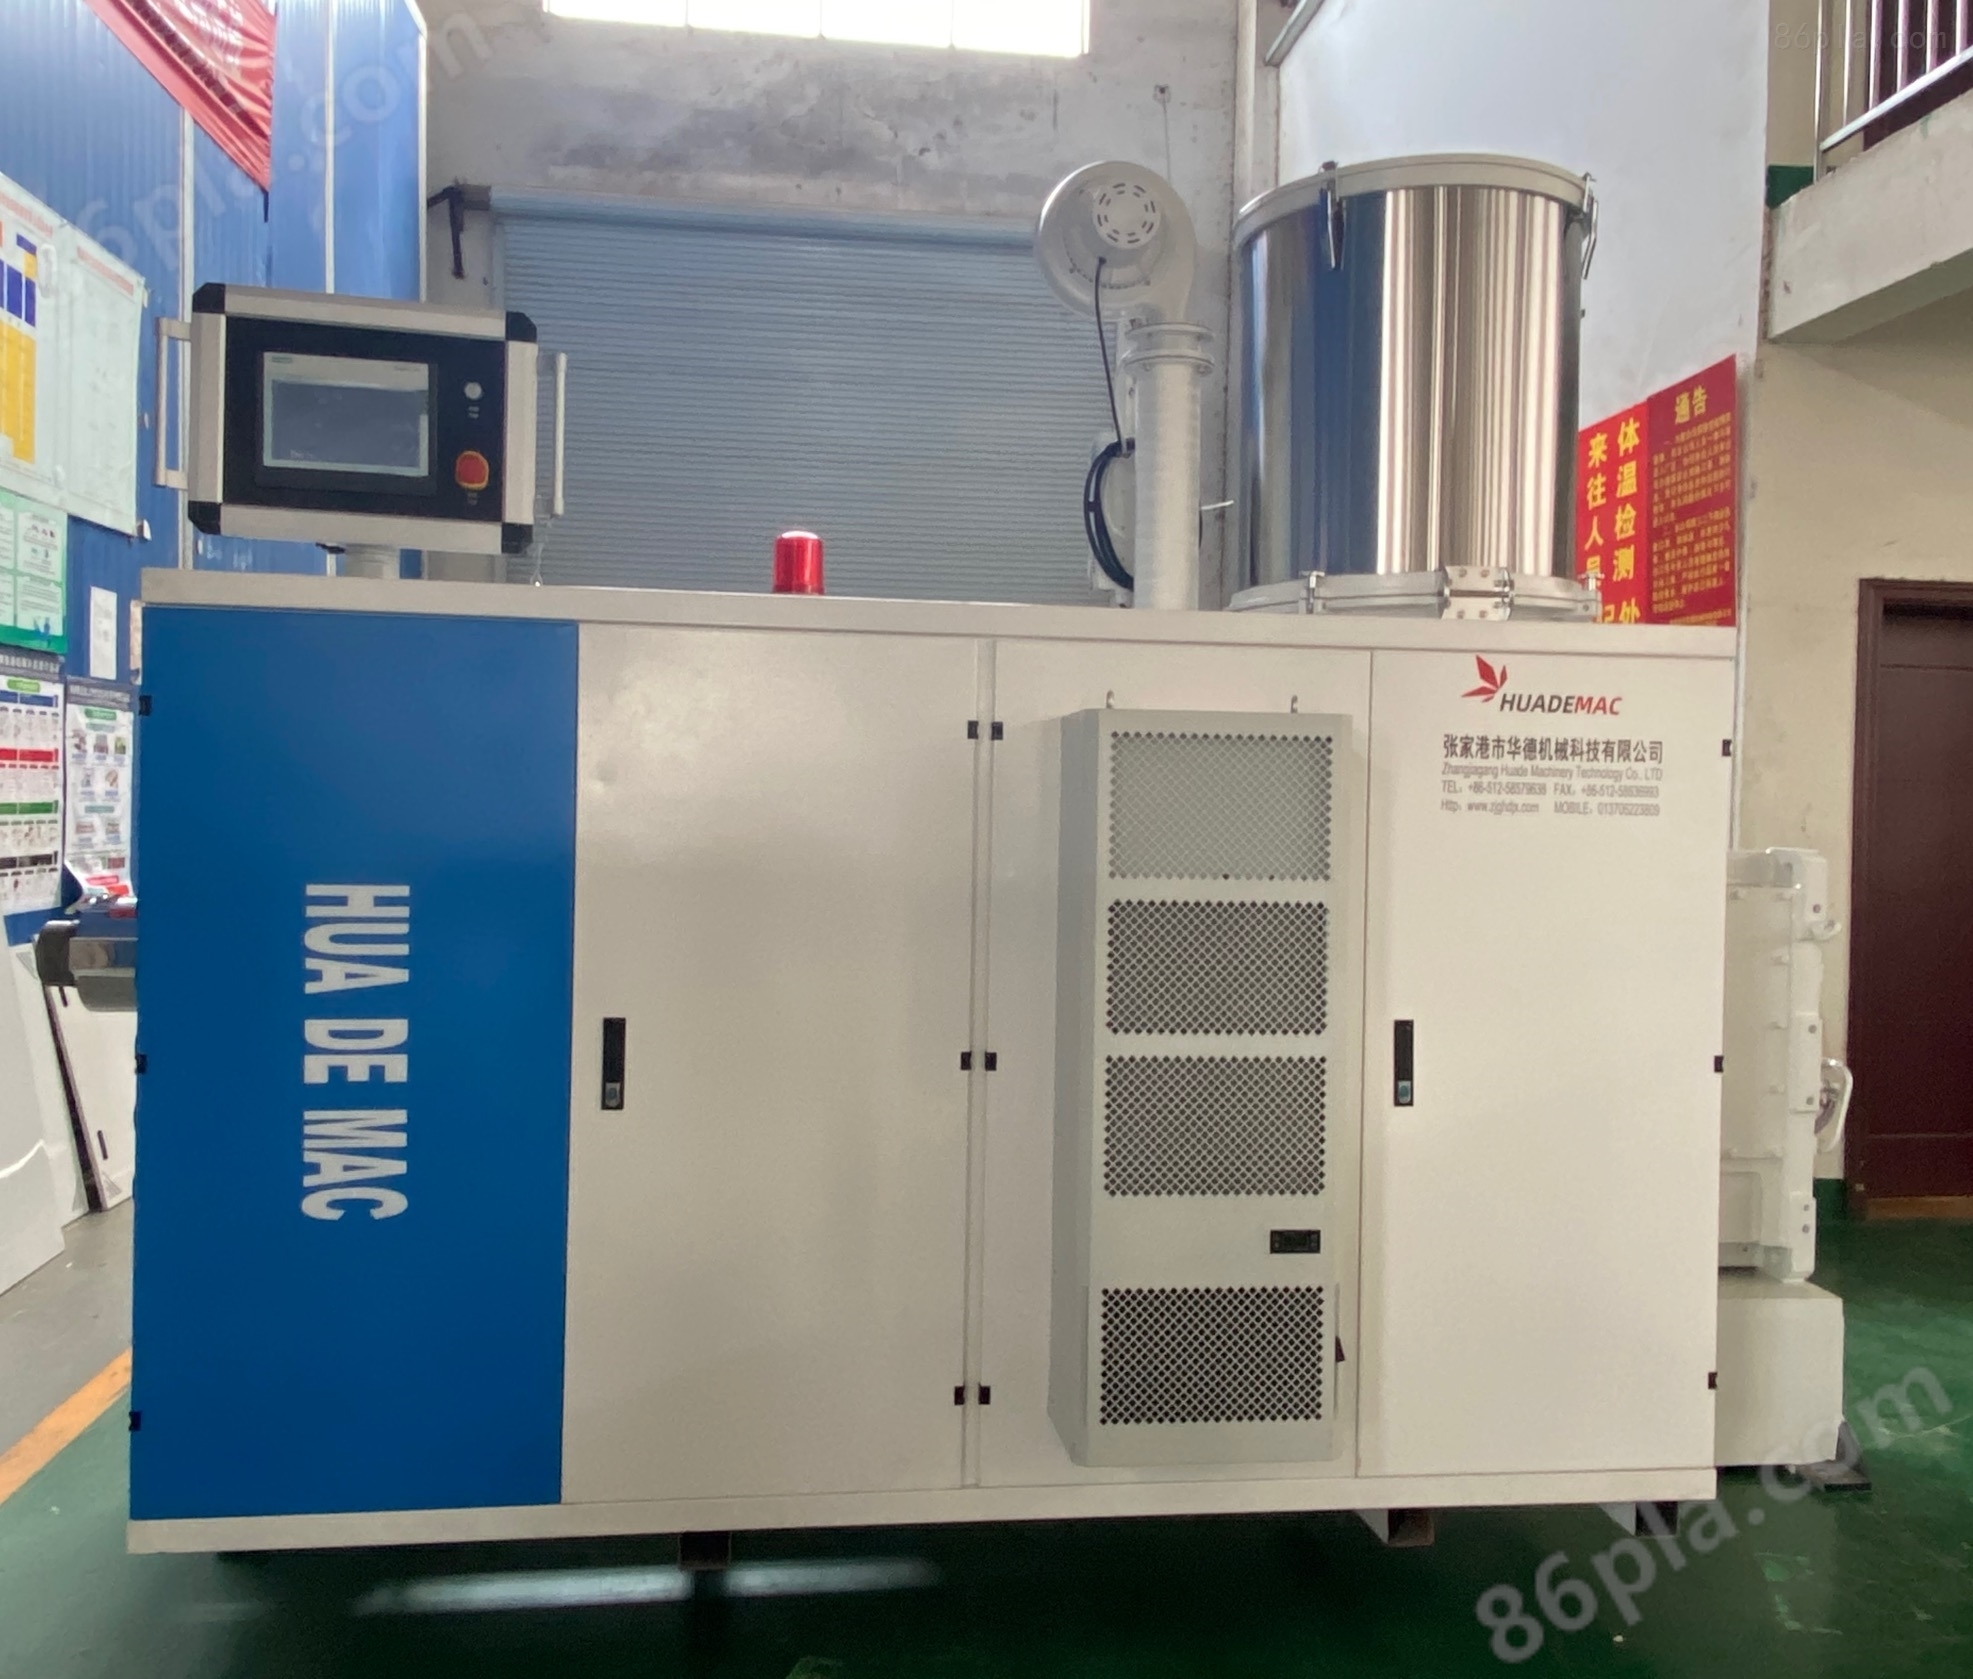

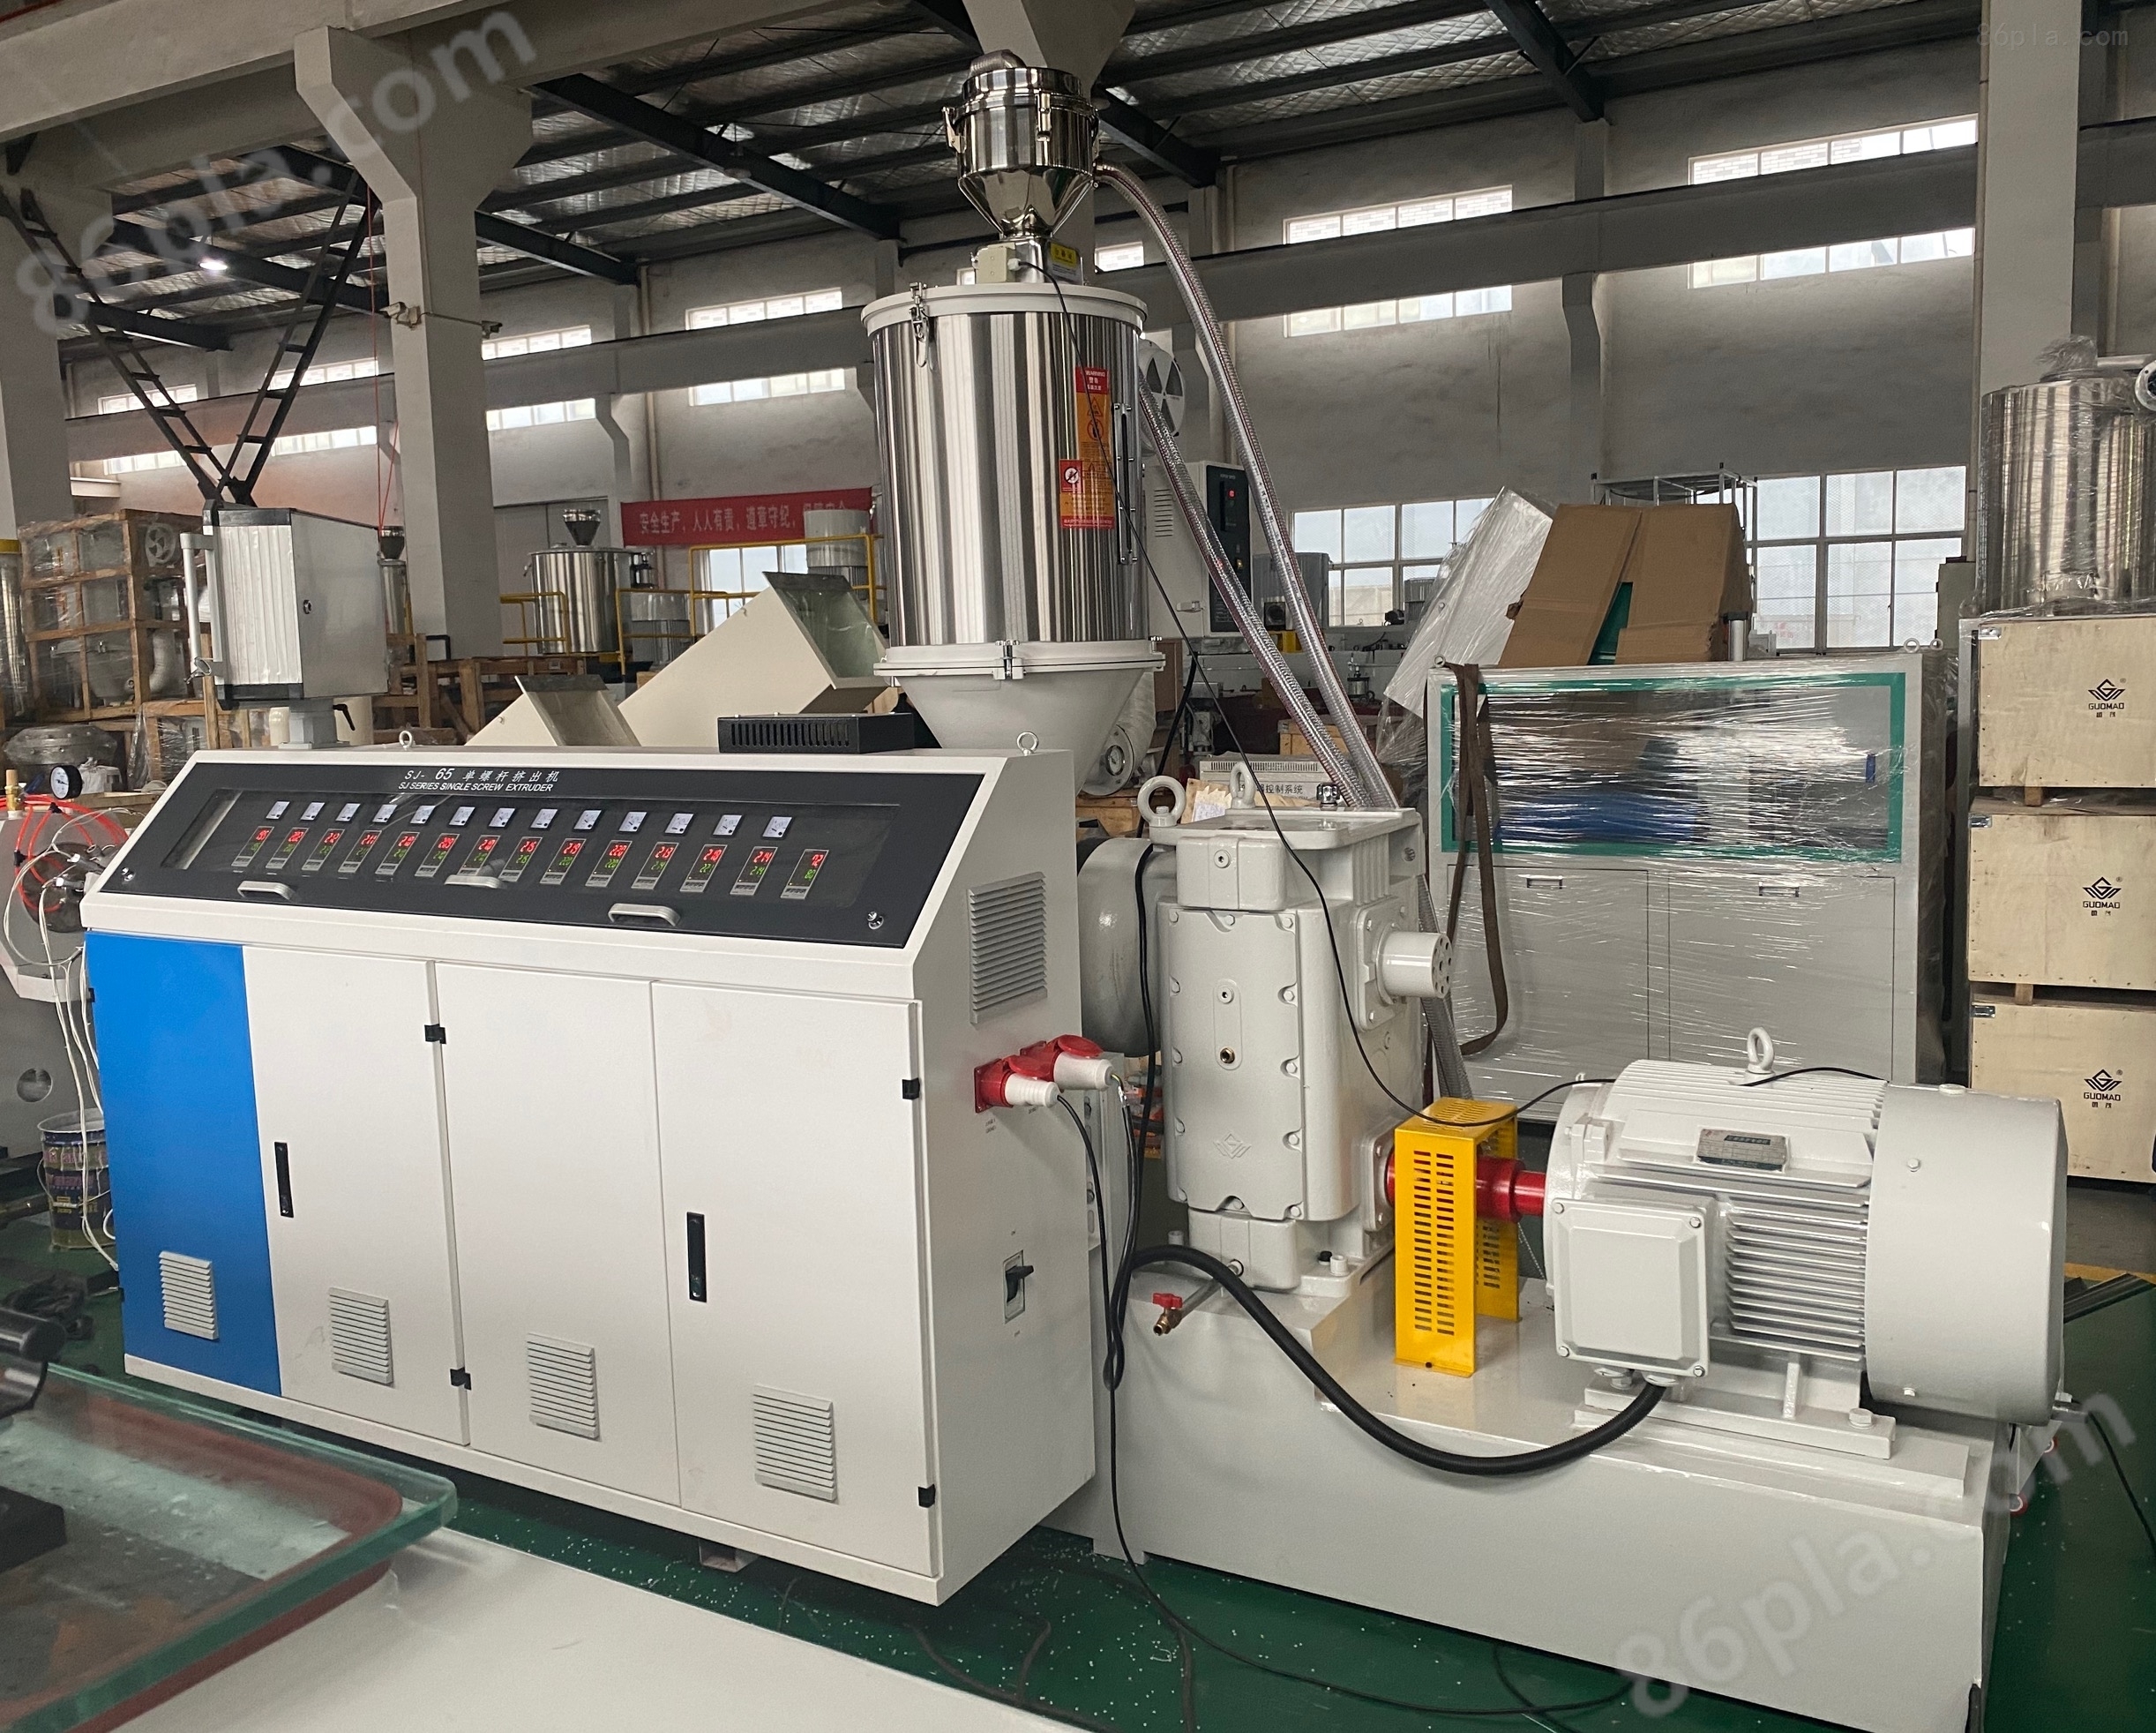
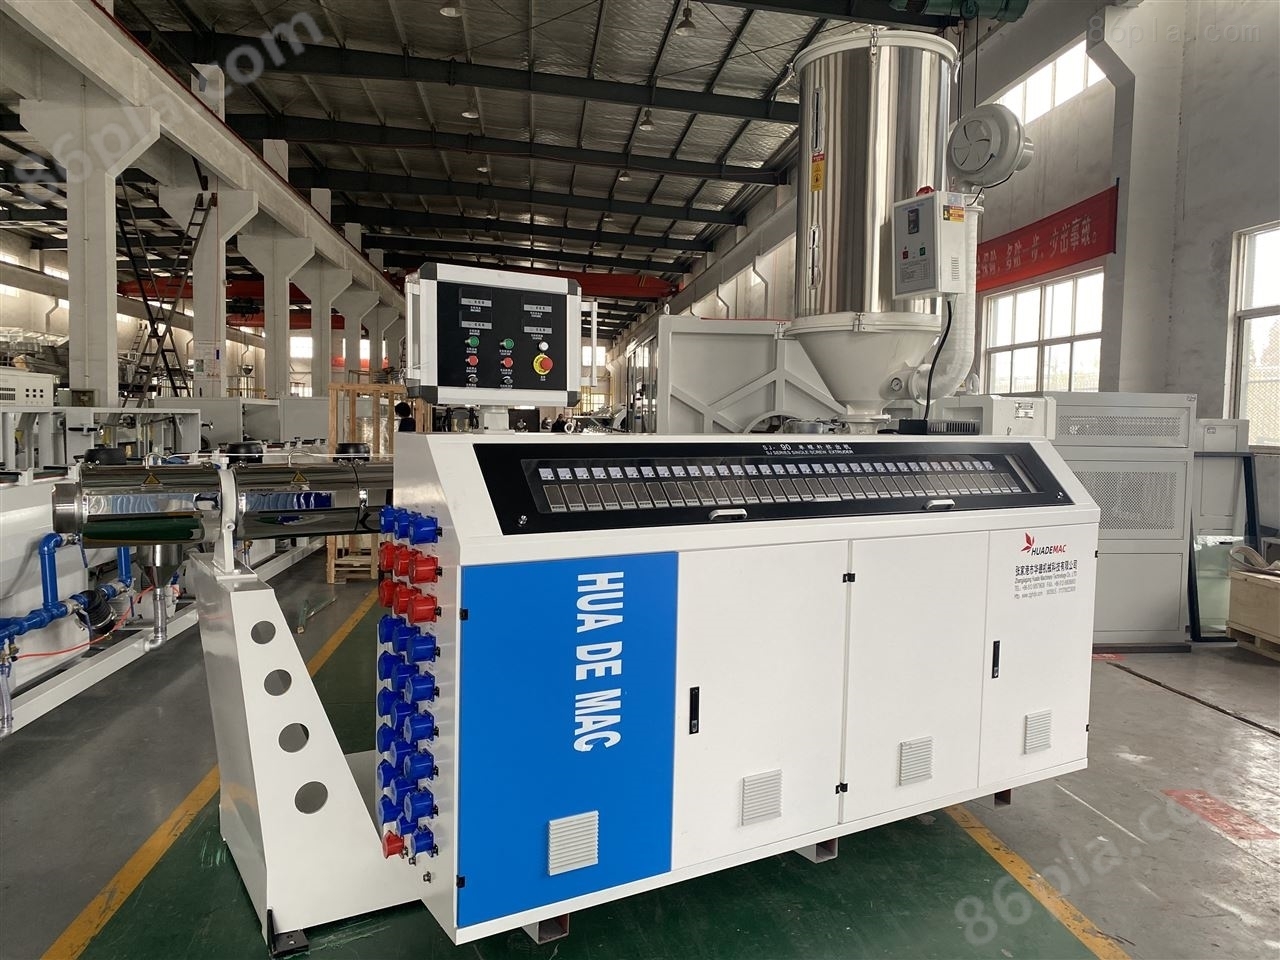
Double stage plastic pellet extruder
NegotiableUpdate on 01/17
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The fully automatic plastic pellet extruder adopts a dual stage integrated design, which enhances the plasticizing function and ensures high-speed, high-performance and stable extrusion. The special barrier comprehensive mixing design ensures the mixing effect of the material, and the high shear and low melting plasticizing temperature ensures the high-performance, low-temperature and low-pressure metering extrusion of the material. Design concept and characteristics: High speed and high-yield extrusion based on high flatness.
Product Details
Double stage plastic pellet extruderpurpose
Pipe extrusion: suitable for PP-R pipes, PE gas pipes, PEX cross-linked pipes, aluminum-plastic composite pipes, ABS pipes, PVC pipes, HDPE silicon core pipes, and various co extruded composite pipes.
Plate and sheet extrusion: suitable for extrusion of PVC, PET, PS, PP, PC and other profiles and plates. Extrusion of various other plastics such as silk, sticks, etc.
Double stage plastic pellet extruderOperation:
1. Preparation for operating the granulator: When using plastic for extrusion molding, attention should be paid to its dryness. The primary raw material should meet the required dryness requirements, and further dryness may be necessary. And sieve the material to remove clumps and mechanical impurities.
2. When operating the granulator, check whether the water, electricity, and gas systems in the equipment are normal, ensure that the water and gas paths are unobstructed and leak free, whether the electrical system is normal, and whether the heating system, temperature control, and various appearances are reliable in operation; Conduct low-speed idle test operation of auxiliary equipment to investigate whether the equipment is operating normally; Activate the shaping table vacuum pump and investigate if the operation is normal; Smooth the lubrication parts of various devices by adding oil. If any problems are found, they should be cleaned up in a timely manner.
3. Install the machine head and shaping sleeve. Choose the appropriate machine head standard based on the type and size of the product. Install the machine head in the following order.
4. Start the operation of the granulator.
5. After the constant temperature is maintained, the machine can be driven. Before driving, the flange bolts of the machine head and granulator should be tightened again to eliminate the difference in thermal expansion between the bolts and the machine head. The sequence of tightening the machine head bolts is diagonal tightening, and the force should be even. When tightening the flange nut of the machine head, it is necessary to ensure that the tightness is consistent in the vicinity, otherwise material will run out.
When operating the granulator, select the "Ready to Start" button, then connect the "Start" button, and slowly rotate the screw speed adjustment knob to start the screw speed slowly. Then gradually accelerate and add a small amount of material together. Pay close attention to the changes in the readings of the host ammeter and various indicator heads when adding materials. The torque of the screw cannot exceed the red mark. During the operation of the granulator, no one is allowed to stand directly in front of the die before the plastic profile is extruded, in order to avoid injury accidents caused by bolt breakage or material wetting and foaming. After the plastic is extruded from the die of the machine head, the extruded material needs to be gradually cooled and led onto the traction equipment and shaping die, and these devices need to be activated. Then, based on the indication values of the manipulated appearance and the demand for extruded products. Adjust each part accordingly to ensure that the entire extrusion operation reaches normal conditions.
Similar Product Recommend


